

Working Principle and Features of Gray Bin Pneumatic Conveying System Equipment
For industrial applications requiring efficient material handling, the gray bin pneumatic conveying system equipment stands out as a reliable solution. This article explores the working principle and key features of such systems, providing insights into how they operate and the advantages they offer to businesses.
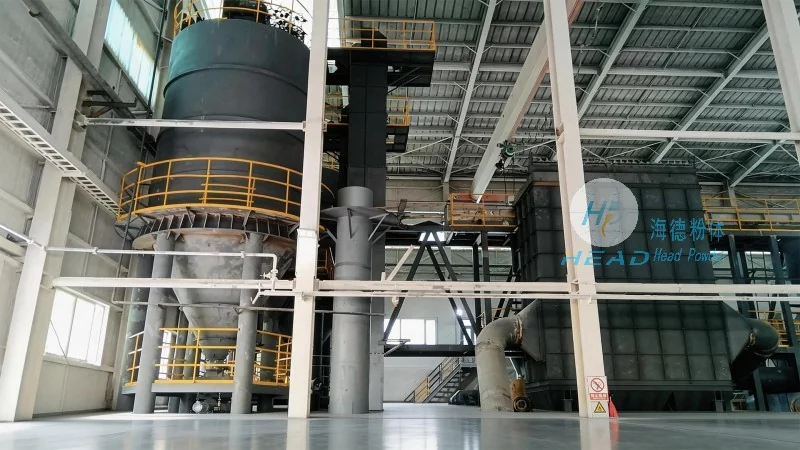
Working Principle of Gray Bin Pneumatic Conveying Systems
The gray bin pneumatic conveying system operates on the principle of using air to transport bulk materials from one location to another. At the core of this system is the gray bin, which serves as the material storage container. The system typically includes a blower or air compressor that generates the necessary airflow. When the system is activated, the material from the gray bin is drawn into the conveying line through a hopper or inlet. The air, under pressure, moves the material particles along the pipeline, ensuring a continuous and controlled flow. The system may also incorporate components like cyclones or filters to separate the material from the air at the discharge end, allowing for clean material delivery and air recycling.
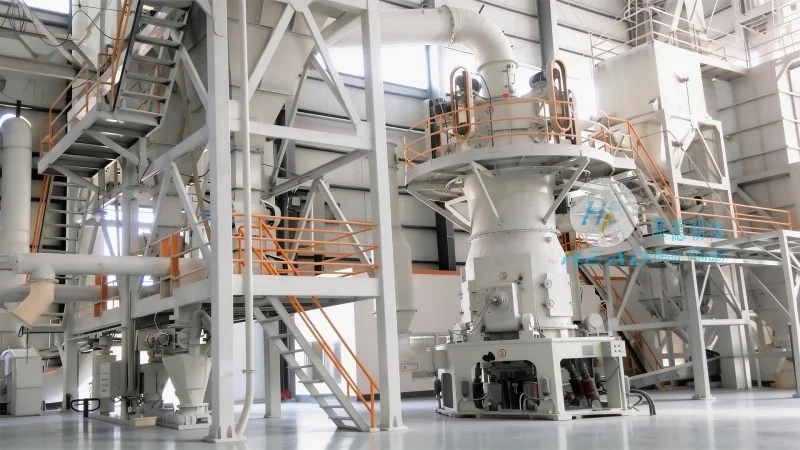
Key Features of Gray Bin Pneumatic Conveying Equipment
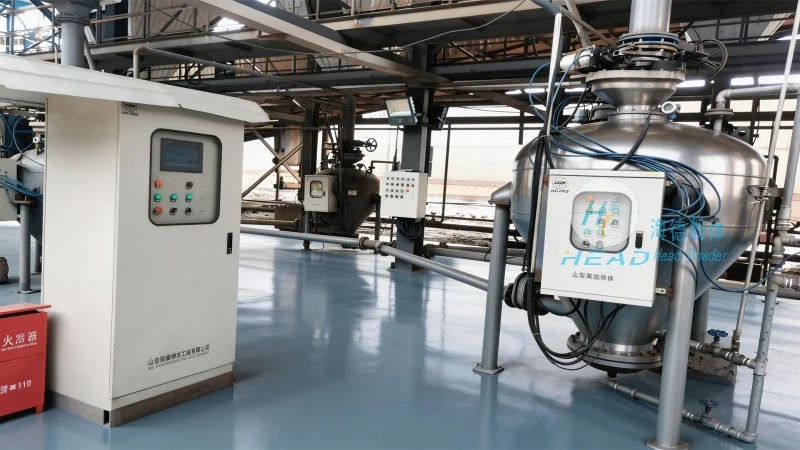
Several notable features define the effectiveness of gray bin pneumatic conveying systems. Firstly, the gray bin itself is designed for durability and easy access to stored materials, often with a hinged lid or sliding door for maintenance and loading. The blower or air compressor unit is engineered for consistent airflow, ensuring stable material transport even with varying material types or quantities. The conveying pipeline is typically made of robust materials like stainless steel or PVC to withstand the abrasive nature of bulk materials and the pressure of the air system. Additionally, the system may include control panels with digital displays and adjustable settings, allowing operators to monitor and adjust the conveying rate as needed. This adaptability is crucial for handling different material properties, such as particle size, density, and moisture content. The system also emphasizes energy efficiency, with some models incorporating variable speed drives to optimize air usage and reduce operational costs. Furthermore, the design often prioritizes safety, with features like pressure relief valves and emergency shut-off mechanisms to prevent accidents and protect equipment.
Applications and Benefits in Industrial Settings
Gray bin pneumatic conveying systems are widely used across various industries, including food processing, pharmaceuticals, chemicals, and mining. In food processing, for example, these systems are employed to transport dry ingredients like flour, sugar, or spices, ensuring hygienic and dust-free handling. The system's ability to maintain product integrity and prevent contamination is a significant advantage. In the pharmaceutical industry, the systems are used for transporting active pharmaceutical ingredients (APIs) and other sensitive materials, where cleanliness and precision are paramount. The controlled environment and minimal human contact reduce the risk of cross-contamination. In chemical and mining sectors, the systems handle abrasive and heavy materials, such as powders, granules, and ores, efficiently moving them over long distances without the need for multiple transfer points. The benefits of using such systems include increased productivity, reduced labor costs, and improved safety compared to traditional manual or mechanical conveying methods. The consistent and reliable material flow minimizes downtime and ensures smooth production processes. Moreover, the compact design of the gray bin allows for easy integration into existing facilities, making it a flexible solution for businesses looking to upgrade their material handling capabilities.
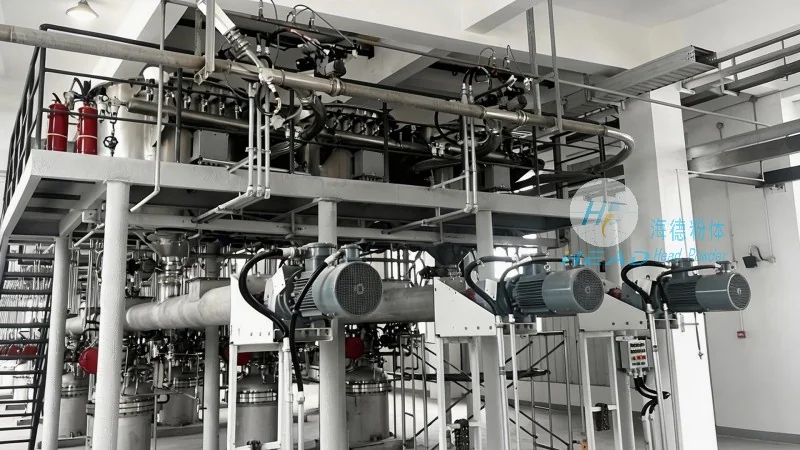
Conclusion and Company Information
In conclusion, the gray bin pneumatic conveying system equipment offers a sophisticated and efficient method for bulk material transport. Its working principle, based on air pressure and controlled material flow, combined with key features like durability, adaptability, and energy efficiency, makes it a preferred choice for industrial applications. The system's ability to handle diverse materials and maintain product quality while reducing operational costs highlights its value. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality gray bin pneumatic conveying systems tailored to meet the specific needs of various industries. With a commitment to innovation and customer satisfaction, the company ensures that its equipment delivers optimal performance and reliability. Based in Shandong, China, HeadPowder continues to be a trusted partner for businesses seeking advanced material handling solutions.