

Pneumatic Conveying in Bulk Chocolate Handling
For companies in the chocolate industry, efficient and reliable bulk material handling is crucial to maintaining production flow and product quality. Pneumatic conveying systems have emerged as a preferred solution for transporting chocolate powders and other bulk ingredients, offering advantages such as hygienic operation, minimal product contamination, and the ability to handle sensitive materials like cocoa and chocolate masses. This article explores the application of pneumatic conveying in bulk chocolate handling, highlighting its benefits and the role of specialized engineering companies in implementing these systems.
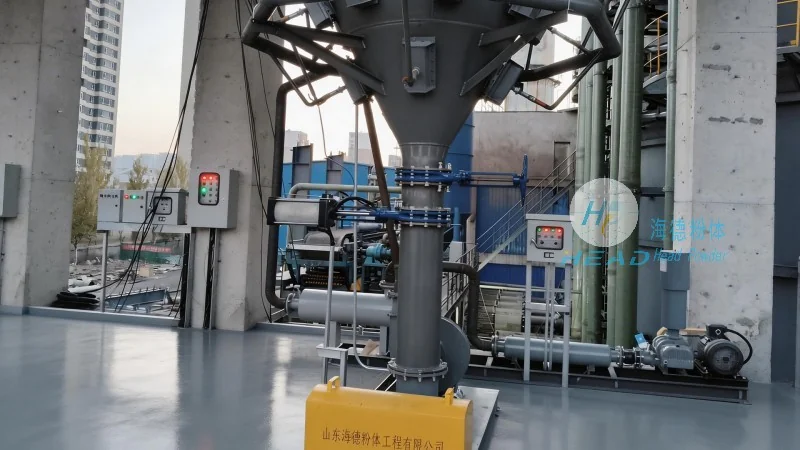
Understanding Pneumatic Conveying Systems
Pneumatic conveying uses air or other gases to transport bulk materials through a pipeline system. There are two main types: pressure and vacuum systems. Pressure systems use compressed air to push material through the line, while vacuum systems use a vacuum to draw material into the system. For chocolate processing, pressure systems are often preferred due to their ability to handle high material loads and maintain consistent flow rates. These systems are designed to minimize product degradation, ensuring that the chocolate's texture, flavor, and color remain intact throughout the conveying process.
Key Benefits of Pneumatic Conveying in Chocolate Handling
Implementing pneumatic conveying in chocolate production offers several key advantages. First, it provides a hygienic and closed system, which is essential for maintaining food safety standards. The enclosed pipeline prevents contamination from external sources and reduces the risk of cross-contamination between different ingredients. Second, pneumatic systems are highly efficient, allowing for continuous material flow without the need for manual handling or frequent equipment stops. This improves overall production throughput and reduces labor costs. Third, these systems are flexible and can be integrated into existing production lines, adapting to changes in production volume or ingredient types. Additionally, they offer better control over material temperature and moisture, which is critical for preserving the quality of chocolate products.
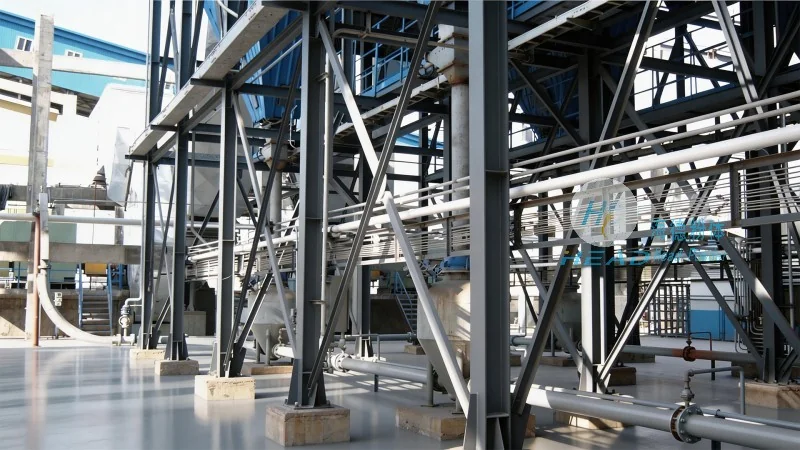
HeadPowder Engineering: Expertise in Chocolate Handling Solutions
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of pneumatic conveying solutions tailored for the chocolate industry. With years of experience in bulk material handling, the company specializes in designing and manufacturing systems that meet the specific needs of chocolate manufacturers. HeadPowder's engineers work closely with clients to understand their production processes, ingredient characteristics, and quality requirements, ensuring that the final system is optimized for performance and reliability. The company's solutions are built using high-quality materials, such as stainless steel and food-grade components, to comply with industry standards and regulations. This commitment to quality and customization has made HeadPowder a trusted partner for chocolate producers worldwide.
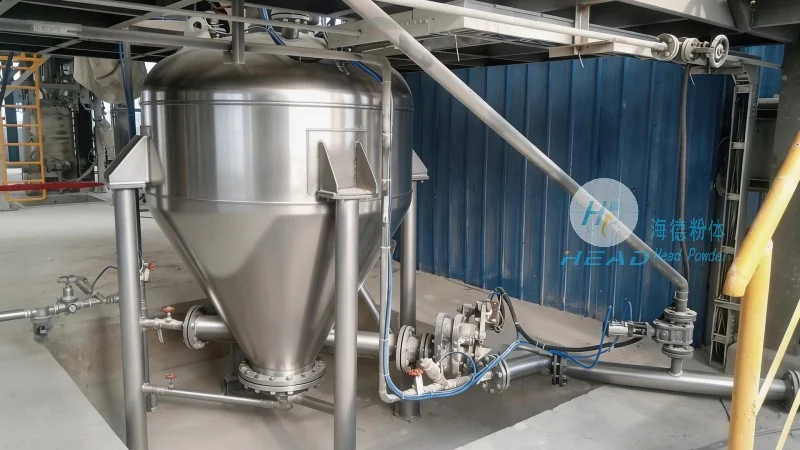
Customized Pneumatic Conveying Solutions for Chocolate Production
HeadPowder offers a range of customized pneumatic conveying solutions for chocolate handling, including screw conveyors, bucket elevators, and flexible hose systems. These solutions are designed to handle various chocolate products, from cocoa powders and chocolate masses to finished chocolate products. The company's systems are equipped with advanced control technologies, allowing for precise control over material flow rates and pressure levels. This ensures that the chocolate is transported efficiently and without damage, maintaining its quality throughout the process. Additionally, HeadPowder provides comprehensive support, including installation, maintenance, and training services, to help clients maximize the performance of their conveying systems.
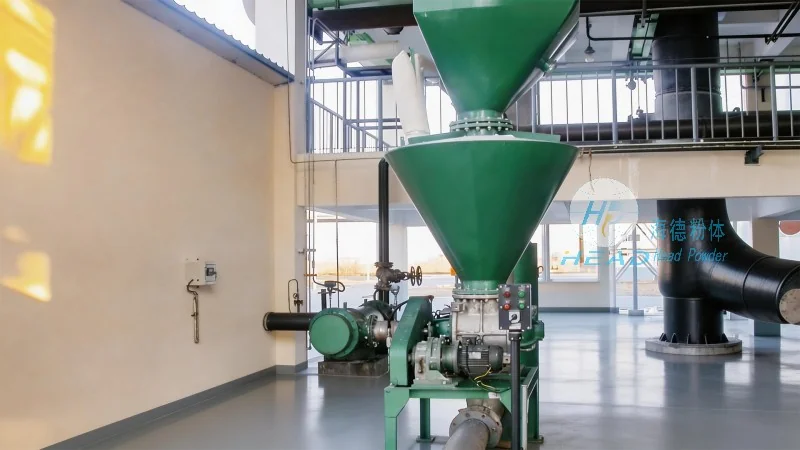
Ensuring Food Safety and Compliance
For chocolate manufacturers, adhering to food safety regulations is paramount. Pneumatic conveying systems, when properly designed and maintained, can help meet these requirements. The enclosed nature of the system prevents contamination from external sources, and the use of food-grade materials ensures that the chocolate remains safe for consumption. HeadPowder Engineering ensures that all its systems comply with international food safety standards, such as HACCP and FDA regulations. The company conducts thorough testing and validation of its systems to guarantee that they meet the highest standards of hygiene and performance. This commitment to compliance helps chocolate producers avoid costly recalls and maintain their reputation in the market.
Conclusion: Enhancing Chocolate Production with Pneumatic Conveying
Pneumatic conveying has become an indispensable technology in the chocolate industry, offering efficient, hygienic, and flexible solutions for bulk material handling. By leveraging the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., chocolate manufacturers can improve their production processes, maintain product quality, and meet regulatory requirements. The integration of advanced pneumatic systems not only enhances operational efficiency but also contributes to the overall success of chocolate production. As the demand for high-quality chocolate products continues to grow, the role of reliable conveying systems will remain critical in meeting industry standards and customer expectations.