

Design of a Chocolate Pneumatic Conveying System
Chocolate processing demands precise and hygienic material handling solutions to preserve product quality and safety. The design of a chocolate pneumatic conveying system is a critical component in modern chocolate manufacturing, enabling the efficient transport of chocolate powders, granules, and other related materials within production facilities. Such systems are engineered to maintain low temperatures, prevent contamination, and ensure smooth operation throughout the entire production process. By integrating advanced technology and robust construction, these systems help chocolate manufacturers achieve higher productivity, reduce operational costs, and meet stringent food safety standards.
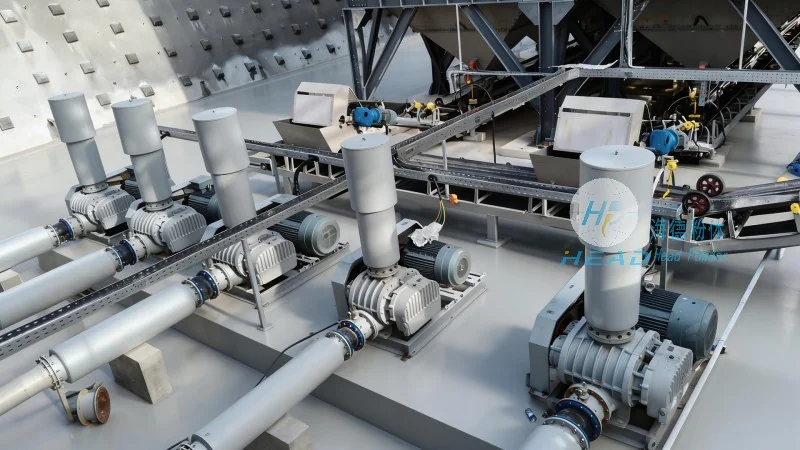
Key Features of the HeadPowder Chocolate Pneumatic Conveying System
HeadPowder Engineering Co., Ltd. has developed a specialized chocolate pneumatic conveying system that combines cutting-edge technology with durable construction. This system is specifically designed to handle a wide range of chocolate products, including cocoa powder, chocolate chips, and finished chocolate items, with exceptional precision and reliability. The equipment features a modular design that facilitates easy installation and maintenance, minimizing downtime during production. Additionally, the system is constructed using high-quality materials that are resistant to corrosion, heat, and chemical exposure, ensuring long-term durability in demanding chocolate manufacturing environments. The hygienic design of the system, with smooth surfaces and easy-to-clean components, complies with food industry regulations, making it suitable for handling sensitive chocolate products.
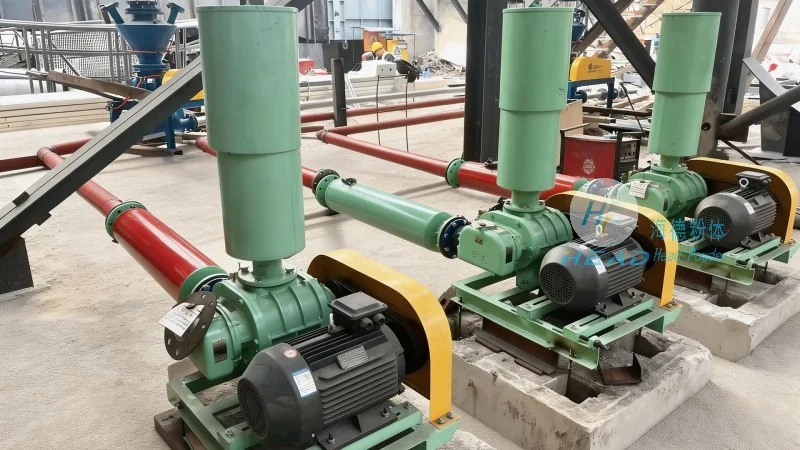
Technical Specifications and Performance Capabilities
The chocolate pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. is engineered with precision to deliver optimal performance. It utilizes a combination of positive and negative pressure conveying methods to ensure efficient material transport while minimizing product degradation. The system is capable of handling various particle sizes and moisture contents, adapting to diverse chocolate production requirements. Advanced control systems are integrated into the design, allowing for real-time monitoring and adjustment of conveying parameters, which ensures consistent product quality and operational efficiency. The equipment operates at controlled temperatures to prevent melting or overheating of chocolate products, preserving the integrity of the final product. The system's high airflow capacity and efficient particle separation mechanisms ensure that even fine chocolate powders are conveyed without clogging or loss, maintaining the purity and quality of the material throughout the process. Additionally, the system features adjustable pressure and flow rates, enabling manufacturers to optimize performance based on specific production needs, such as varying batch sizes or product types.
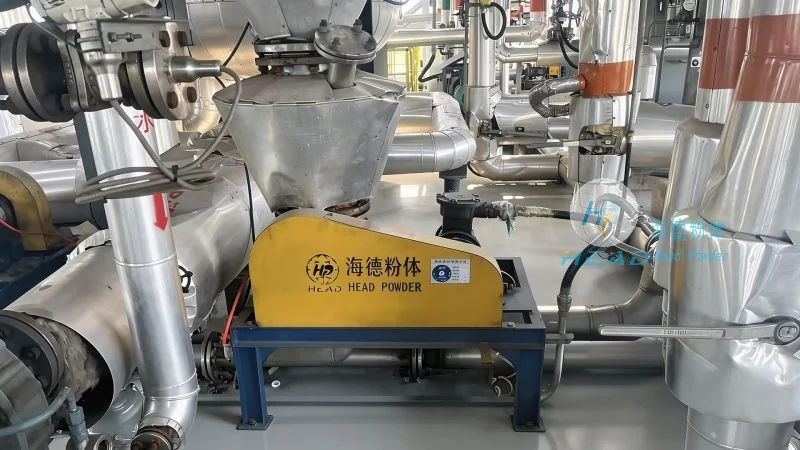
Application in Chocolate Production Lines
Chocolate pneumatic conveying systems play a vital role in chocolate manufacturing facilities by transporting raw materials and finished products seamlessly. The HeadPowder system is particularly well-suited for applications such as moving cocoa powder from storage silos to processing lines, conveying chocolate chips to packaging stations, and transporting finished chocolate products to storage or shipping areas. The system's ability to handle bulk materials efficiently reduces the need for manual handling, enhancing workplace safety and reducing labor costs. In addition, the system's hygienic design and easy cleaning features make it ideal for food processing environments, where compliance with food safety regulations is non-negotiable. By integrating this system into their production lines, chocolate manufacturers can streamline their operations, improve overall productivity, and maintain consistent product quality across different batches.
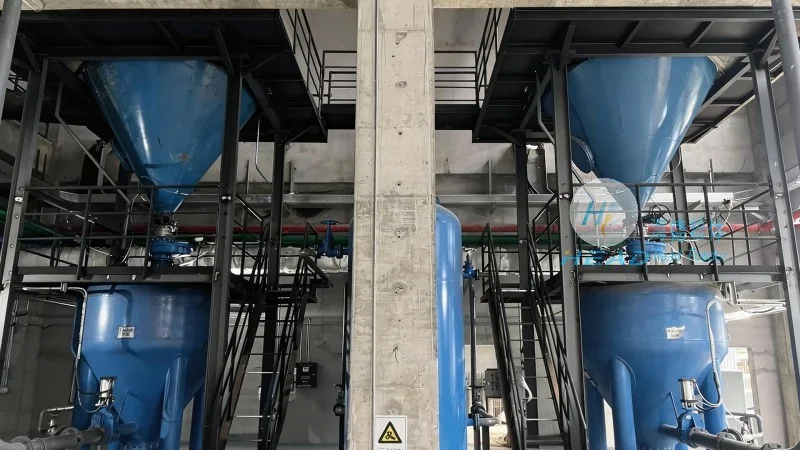
Advantages of Partnering with HeadPowder Engineering
Choosing HeadPowder Engineering Co., Ltd. for your chocolate pneumatic conveying system offers several key advantages. The company has a proven track record in designing and manufacturing high-quality conveying equipment tailored to the food industry's specific needs. Their team of experienced engineers and technicians provides customized solutions that address the unique challenges faced by each client. The HeadPowder system is backed by comprehensive technical support, including professional installation, operator training, and ongoing maintenance services. This ensures that clients receive the best possible service and support throughout the equipment's lifecycle. The company's commitment to quality, reliability, and customer satisfaction has established it as a trusted partner for chocolate manufacturers worldwide. By selecting HeadPowder Engineering, manufacturers can enhance their operational efficiency, reduce costs, and ensure the highest standards of product quality and safety.