

Design of a Powdered Milk Pneumatic Conveying System
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional engineering company based in Shandong, China. The company specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems, particularly for the food and dairy industries. With a strong focus on precision, efficiency, and safety, headpowder provides customized solutions tailored to the unique requirements of each client.
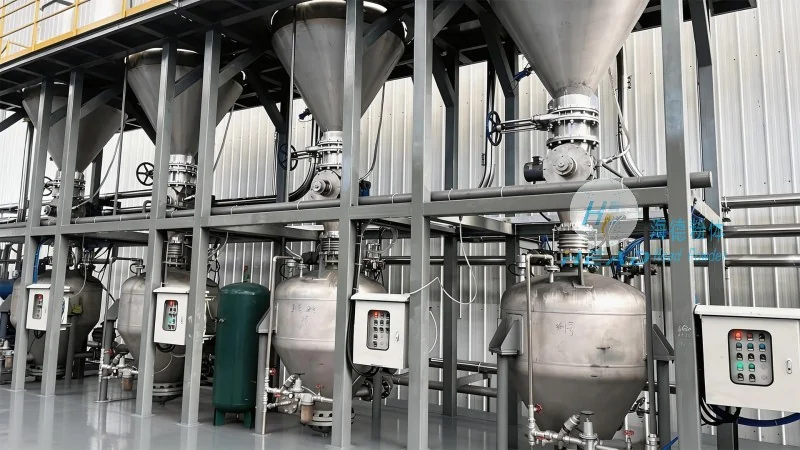
Pneumatic Conveying System Design for Powdered Milk
The design of a powdered milk pneumatic conveying system involves a comprehensive approach that integrates mechanical engineering principles, material science, and process control. At headpowder, our team of experienced engineers works closely with clients to understand their specific operational needs, production volumes, and product characteristics. This collaborative process ensures that the final system is optimized for maximum performance and minimal downtime.
Key Components and Their Functionality
A typical powdered milk pneumatic conveying system consists of several critical components, each playing a vital role in the overall operation. The system begins with a hopper or silo that stores the powdered milk, equipped with a level indicator to monitor the material volume. The hopper is connected to a feeder, which controls the flow rate of the material into the conveying line. This feeder is crucial for maintaining consistent pressure and preventing blockages in the system.
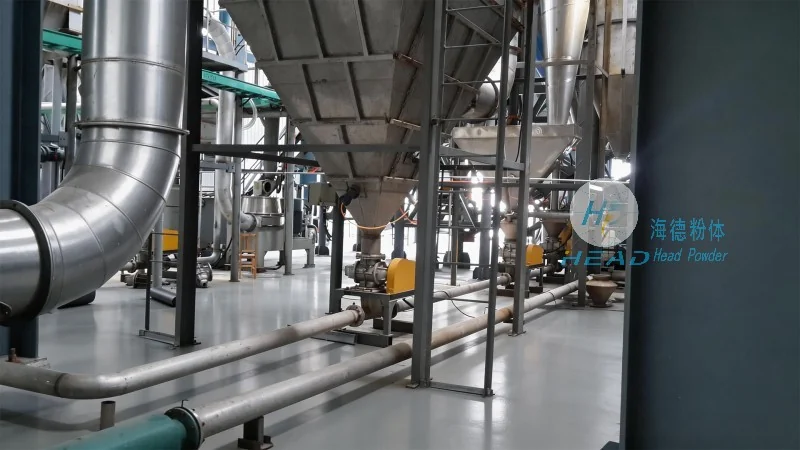
The conveying line itself is the core of the system, often made of stainless steel to ensure hygiene and durability. The line may include various sections such as vertical or horizontal pipes, bends, and expansion joints. The choice of pipe diameter and material is determined by the flow rate, particle size, and moisture content of the powdered milk. For example, larger particles may require a larger pipe diameter to prevent clogging, while smaller particles can be conveyed in narrower lines with higher air velocities.
Air Supply and Control Systems
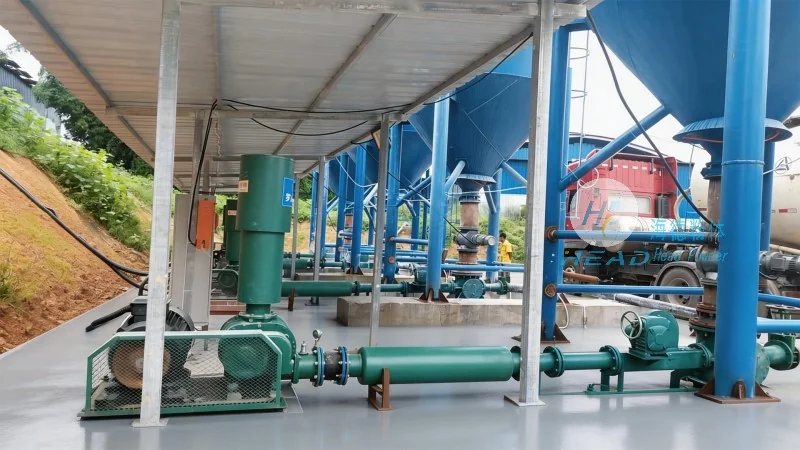
Air supply is a critical factor in pneumatic conveying, as it provides the necessary force to move the material through the system. At headpowder, we use high-quality air compressors and blower systems that are specifically designed for the demands of powder handling. These systems are equipped with pressure regulators and flow meters to maintain stable air pressure and volume. The control system includes sensors that monitor pressure, temperature, and flow rates, allowing for real-time adjustments to optimize the conveying process.
Material Handling and Safety Features
Ensuring the safe and efficient handling of powdered milk is a top priority. Our systems incorporate several safety features, including dust collection and filtration systems to prevent airborne contamination. The design also includes explosion-proof components where necessary, as the accumulation of powder can pose a fire risk. Additionally, the system is equipped with emergency shut-off valves and alarms to detect and respond to any potential issues, such as blockages or pressure spikes.
Customization and Integration
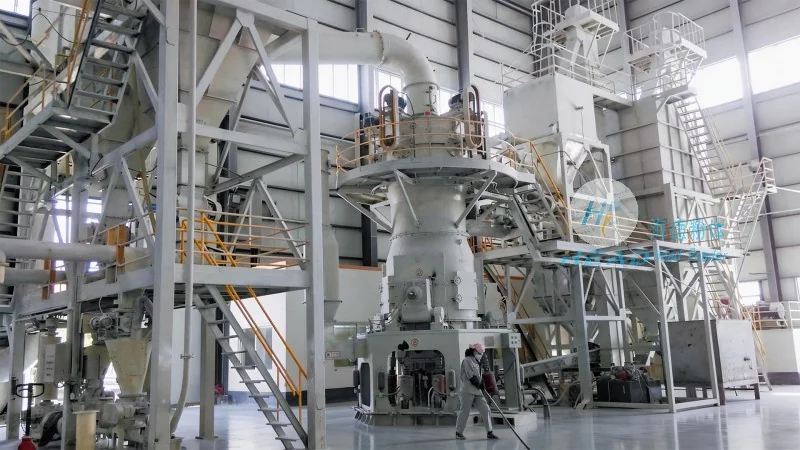
Every pneumatic conveying system is unique, and headpowder understands the importance of customization. We work with clients to develop solutions that integrate seamlessly with existing production lines, whether it's a new installation or an upgrade to an existing facility. Our engineers consider factors such as space constraints, power availability, and regulatory requirements to ensure the system meets all operational and safety standards. The final design is validated through simulations and testing to guarantee optimal performance before installation.
Benefits of a Well-Designed Pneumatic Conveying System
Implementing a properly designed pneumatic conveying system for powdered milk offers numerous benefits. These include increased production efficiency, reduced labor costs, and improved product quality through consistent handling. The system also minimizes material waste and contamination, which is essential in the food industry. Furthermore, the automated nature of the system reduces the risk of human error and ensures compliance with hygiene standards. Overall, a well-engineered pneumatic conveying system provides a reliable and cost-effective solution for the transportation of powdered milk in industrial settings.