

Colored Sand Pneumatic Conveying System Solution
HeadPowder, a leading engineering company based in Shandong, China, specializes in providing comprehensive solutions for colored sand pneumatic conveying systems. This article outlines the key aspects and benefits of such systems, emphasizing the technical expertise and practical applications offered by the company.
Introduction to Colored Sand Pneumatic Conveying Systems
Colored sand, often used in construction, decoration, and industrial applications, requires efficient and reliable transportation methods to ensure quality and minimize material loss. Pneumatic conveying systems offer a superior alternative to traditional methods like belt conveyors or bucket elevators, particularly for handling fine powders and granular materials. These systems utilize air pressure to move colored sand through a network of pipes, making them ideal for applications where dust control, hygiene, and flexibility are critical.
Key Features and Advantages of the System
The colored sand pneumatic conveying system designed by HeadPowder incorporates several advanced features that enhance performance and operational efficiency. One of the primary advantages is the ability to handle a wide range of colored sand types, from fine powders to coarse granules, without compromising on material integrity. The system employs high-efficiency air compressors and specialized ductwork to maintain consistent air flow, ensuring smooth and continuous material transport. Additionally, the design includes dust collection and filtration components to comply with environmental regulations and maintain a clean working environment. This not only improves safety but also reduces maintenance costs by minimizing equipment wear and tear.
Technical Specifications and Components
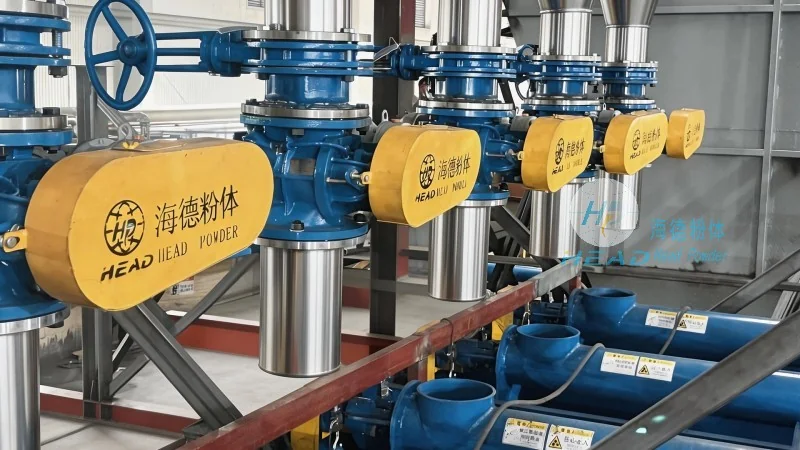
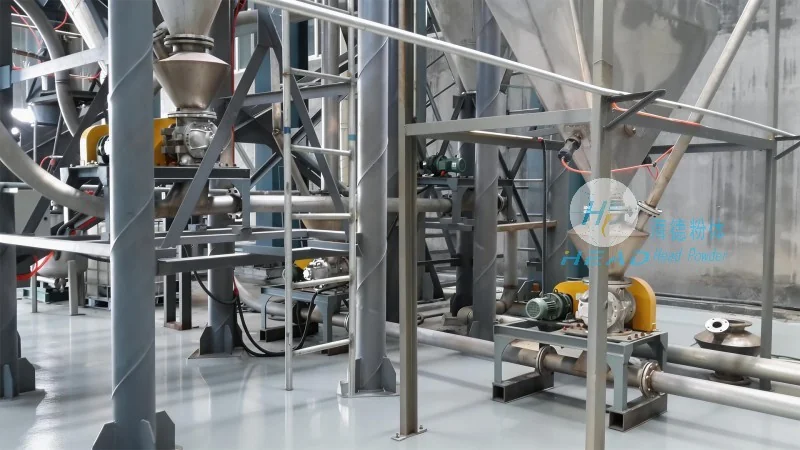
HeadPowder's colored sand pneumatic conveying system is built with robust components that are engineered for durability and long-term performance. The system typically includes a hopper for material storage, a rotary airlock valve to control the flow of colored sand into the pipeline, and a series of vertical or horizontal ducts connected by elbows and tees. The air compressor, often a positive displacement type, generates the necessary pressure to move the material through the system. The system may also feature a pressure regulator to maintain stable air pressure and a vacuum or pressure relief valve to prevent over-pressurization. For applications requiring high capacity, multiple pipelines or a larger compressor can be integrated to increase throughput. The company's engineers tailor the system design to meet specific client requirements, ensuring optimal performance for each project.
Applications and Industries
The colored sand pneumatic conveying system is widely used across various industries that rely on colored sand for their products. In the construction industry, it is used to transport colored sand for concrete and mortar production, ensuring consistent color and texture. The decorative industry benefits from the system's ability to handle fine colored powders for paints, coatings, and architectural finishes. Additionally, in the manufacturing sector, the system is employed in the production of colored plastics, ceramics, and other composite materials. The flexibility of the pneumatic conveying system allows it to adapt to different production scales, from small-scale artisanal operations to large industrial facilities. This adaptability makes it a preferred choice for companies seeking to improve their material handling processes and reduce operational costs.
Installation and Maintenance Considerations
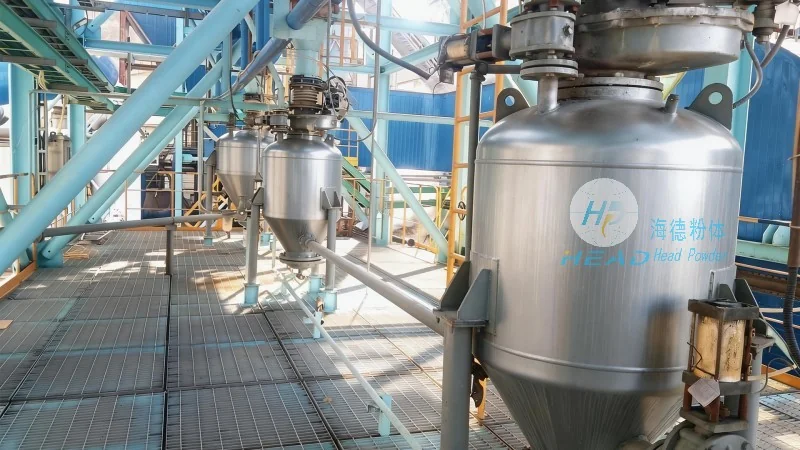
Proper installation and regular maintenance are crucial for the optimal performance and longevity of the colored sand pneumatic conveying system. HeadPowder provides comprehensive installation services, including site assessment, system layout design, and equipment assembly. The company's technicians ensure that all components are correctly aligned and connected to minimize air leaks and material blockages. Regular maintenance involves checking air compressor performance, cleaning filters and ducts, and inspecting rotary airlock valves for wear. The system's design incorporates easy access points for maintenance, reducing downtime and ensuring that the equipment remains in good working condition. HeadPowder offers maintenance contracts and technical support to assist clients in keeping their systems operational and efficient. This support includes scheduled inspections, parts replacement, and troubleshooting services, ensuring that any issues are addressed promptly and effectively.
Environmental and Safety Compliance
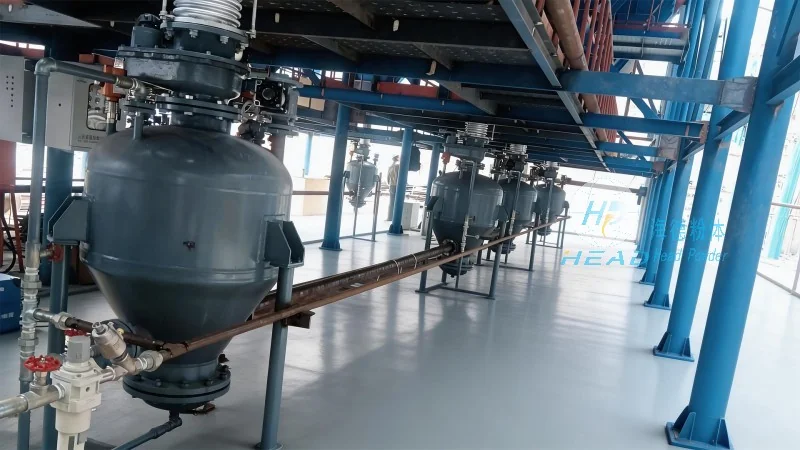
HeadPowder's colored sand pneumatic conveying system is designed with environmental and safety considerations in mind. The system includes dust collection and filtration systems that capture and neutralize airborne particles, reducing the risk of dust explosions and improving air quality. The use of sealed ductwork and proper ventilation helps maintain a safe working environment for personnel. Additionally, the system complies with local and international environmental regulations regarding emissions and waste management. By implementing these safety and environmental features, the company ensures that its clients can operate their facilities in compliance with legal requirements while minimizing their environmental impact. This commitment to safety and sustainability aligns with the growing demand for responsible industrial practices in the market.
Conclusion
HeadPowder's colored sand pneumatic conveying system offers a reliable and efficient solution for transporting colored sand in various industrial applications. With its advanced features, robust components, and tailored design, the system enhances operational efficiency, reduces material loss, and improves overall productivity. The company's expertise in engineering and manufacturing ensures that each system is customized to meet the specific needs of clients, providing long-term benefits and cost savings. Based in Shandong, China, HeadPowder continues to be a trusted partner for companies seeking high-quality material handling solutions. By leveraging the latest technology and adhering to strict quality standards, the company delivers systems that meet the highest industry benchmarks and contribute to the success of its clients' operations.