

Operation Process and Working Principle of Catalyst Powder Material Handling System Equipment
For industrial applications involving catalyst powders, the efficient and reliable transportation of these fine materials is crucial. The catalyst powder material handling system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., is designed to address the challenges associated with handling such delicate and often sensitive powders. This equipment ensures that catalyst powders are transported safely and effectively, maintaining their quality and integrity throughout the process. The system integrates advanced technology and robust engineering to meet the demanding requirements of modern industrial processes.
Key Components and Their Roles in the Material Handling System
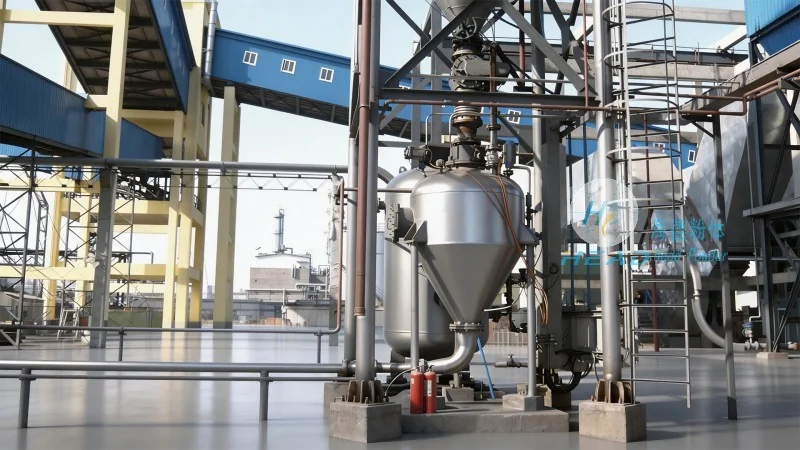
The catalyst powder material handling system consists of several key components that work in tandem to ensure smooth operation. The primary components include the hopper, conveyor system, control panel, and dust collection unit. The hopper serves as the storage container for the catalyst powder, providing a stable and controlled environment for material storage. The conveyor system, which may include screw conveyors, belt conveyors, or pneumatic conveying lines, is responsible for transporting the powder from the hopper to the desired destination. The control panel allows operators to monitor and adjust the system parameters, ensuring optimal performance. The dust collection unit is essential for maintaining a clean and safe working environment by capturing and filtering any airborne particles.
Operation Process of the Catalyst Powder Material Handling System
The operation of the catalyst powder material handling system follows a systematic process. Initially, the catalyst powder is loaded into the hopper. The system then activates the conveyor mechanism, which transports the powder through the system. The control panel allows operators to set the speed and direction of the conveyor, ensuring precise control over the material flow. As the powder moves through the system, it may pass through a series of processing steps, such as mixing or blending, if required. The system is equipped with sensors and alarms to detect any abnormalities, such as blockages or overfilling, and to alert operators. Once the powder reaches the final destination, it is discharged into the receiving container. The entire process is designed to be automated, reducing the need for manual intervention and minimizing the risk of human error.
Working Principle of the Catalyst Powder Material Handling System
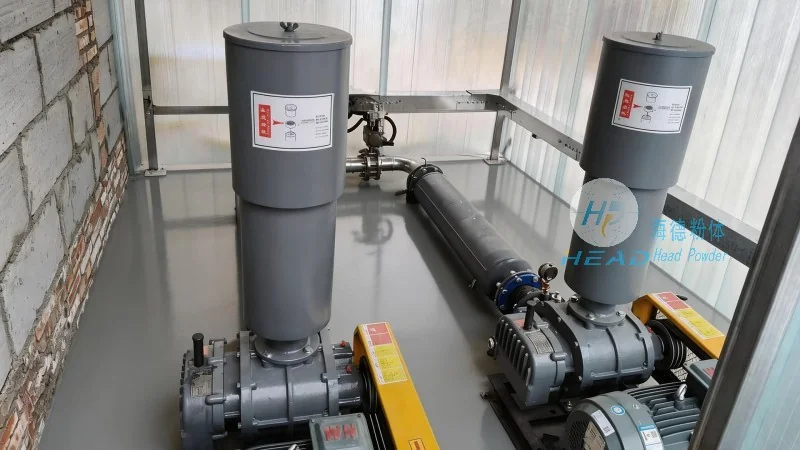
The working principle of the catalyst powder material handling system is based on the principles of fluidization and pneumatic conveying. The system utilizes a combination of mechanical and pneumatic forces to move the powder. In the hopper, the powder is kept in a fluidized state, which allows it to flow freely and be easily conveyed. The conveyor system uses either a screw or a belt to move the powder, while the pneumatic conveying lines use compressed air to transport the powder through the system. The control panel regulates the flow of air and the speed of the conveyor, ensuring that the powder is transported at the optimal rate. The dust collection unit uses filters to capture any particles that may be released during the process, preventing air pollution and maintaining a safe working environment.
Advantages of Using the Catalyst Powder Material Handling System
Shandong HeadPowder Engineering Co., Ltd.'s catalyst powder material handling system offers several advantages over traditional methods of powder transportation. The system is designed to handle fine and delicate powders without causing agglomeration or degradation. The automated operation reduces labor costs and increases efficiency. The system also minimizes the risk of contamination, as it is equipped with dust collection and filtration systems. Additionally, the system is highly customizable, allowing it to be adapted to the specific needs of different industrial applications. The robust design ensures long-term reliability and minimal maintenance requirements.
Applications of the Catalyst Powder Material Handling System
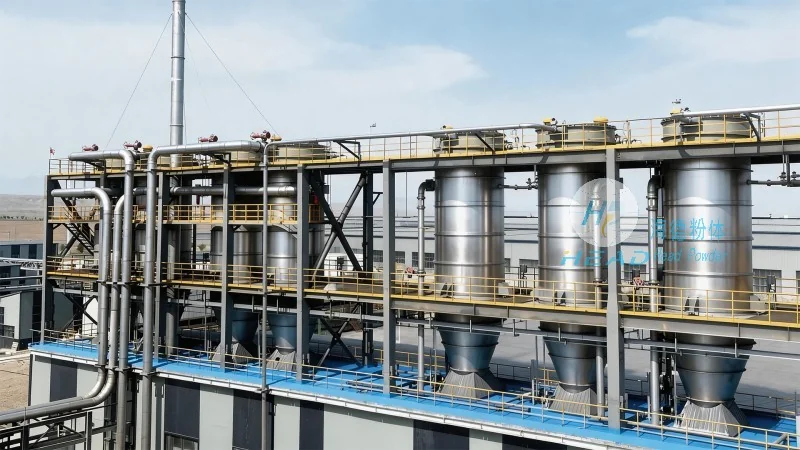
The catalyst powder material handling system is widely used in various industrial sectors, including chemical, pharmaceutical, and petrochemical industries. In the chemical industry, the system is used to transport catalyst powders for reactions and processes. In the pharmaceutical industry, it is used to handle active pharmaceutical ingredients (APIs) and other fine powders. In the petrochemical industry, the system is used to transport catalysts for refining processes. The system is also used in research and development laboratories for small-scale experiments and pilot studies.
Conclusion and Company Information
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of catalyst powder material handling system equipment. The company is committed to providing high-quality, reliable, and efficient solutions for industrial applications. The catalyst powder material handling system is designed to meet the demanding requirements of modern industries, ensuring safe and effective transportation of catalyst powders. The company's expertise in engineering and manufacturing ensures that the system is built to the highest standards, providing long-term performance and reliability. With its headquarters in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. serves customers worldwide, offering customized solutions to meet their specific needs.