

Principle and Working Scene Characteristics of Sugar Material Pneumatic Conveying Machines
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced pneumatic conveying systems tailored for sugar processing industries. The company's expertise lies in developing efficient and reliable equipment that addresses the unique challenges of handling sugar materials, ensuring optimal performance in various operational environments.
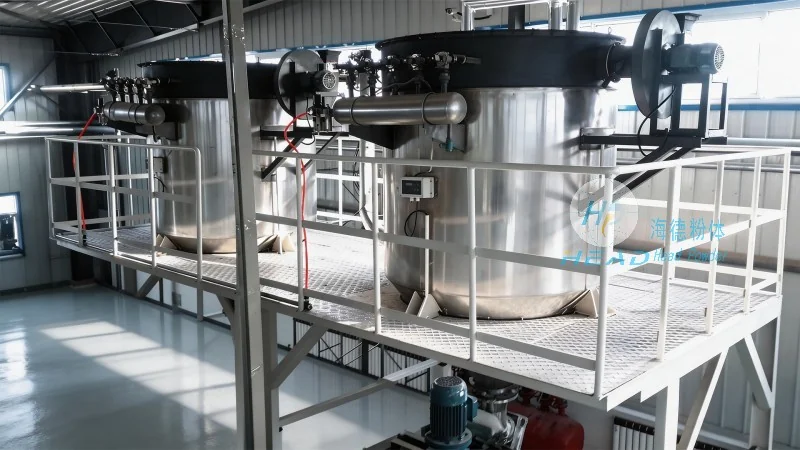
Principle of Sugar Material Pneumatic Conveying Machines
Sugar material pneumatic conveying machines operate on the fundamental principle of using air or gas as the conveying medium to transport bulk materials. The system typically consists of a hopper, a conveyor pipe, a fan or blower, and a discharge outlet. When the fan generates airflow, it draws the sugar particles from the hopper into the pipe, where they are carried to the destination point. This process is often referred to as "air-assisted" or "pressure-assisted" conveying, depending on the system design. The key to efficient operation lies in maintaining consistent air pressure and flow rates, which directly impact the conveying capacity and material handling efficiency. The equipment is engineered to handle different sugar types, including raw sugar, refined sugar, and sugar syrups, with varying particle sizes and moisture content. By controlling the air velocity and pressure, the system ensures minimal product degradation, reduced dust generation, and improved overall process reliability. For instance, in the case of raw sugar, which often has larger crystal sizes and higher moisture content, the system is designed with larger pipe diameters and higher air velocities to prevent blockages and ensure smooth transport. In contrast, refined sugar, with finer granules, may require lower air velocities to avoid particle breakage and maintain product quality. The principle of pneumatic conveying is also adaptable to different operational pressures, with pressure-assisted systems providing higher conveying distances and capacities compared to vacuum-assisted systems.
Working Scene Characteristics of Sugar Material Pneumatic Conveying Machines
The working scene characteristics of sugar material pneumatic conveying machines are tailored to meet the specific demands of sugar processing facilities. These systems are commonly used in scenarios such as raw sugar storage and transfer, refined sugar production lines, sugar syrup processing, and bulk sugar handling in warehouses. The equipment is designed to operate in environments where space constraints and material flow optimization are critical. For instance, in sugar refineries, the pneumatic conveying system efficiently transports sugar from storage silos to processing units, reducing the need for manual handling and enhancing safety. In sugar processing plants, the system can handle both dry and wet sugar materials, adapting to different production stages. The working scene also includes applications in sugar export and import facilities, where the equipment facilitates the smooth transfer of bulk sugar between storage areas and shipping containers. The characteristics of these systems, such as low maintenance requirements and energy efficiency, make them suitable for continuous operation in industrial settings. Additionally, the systems are equipped with features like dust collection and filtration, ensuring compliance with environmental regulations and maintaining a clean working environment. In raw sugar processing plants, the pneumatic conveying system may be used to transport raw sugar from the storage yard to the refining unit, where it undergoes washing, screening, and crystallization. The system's ability to handle large volumes of raw sugar with minimal downtime is crucial for maintaining production efficiency. In refined sugar production, the system can transport refined sugar from the crystallization tank to the packaging line, ensuring a continuous flow of product. The working scene also includes applications in sugar syrup processing, where the system is used to convey syrup from the evaporation tanks to the storage tanks, maintaining the syrup's viscosity and preventing contamination. The equipment's adaptability to different sugar types and processing stages makes it a versatile solution for various working scenarios in the sugar industry.
Key Features and Advantages of Sugar Material Pneumatic Conveying Systems
HeadPowder's sugar material pneumatic conveying machines are equipped with several key features that enhance their performance and reliability. One of the primary advantages is the ability to handle a wide range of sugar types, from fine granules to larger crystals, without causing product degradation. The systems are designed with corrosion-resistant materials, such as stainless steel, to withstand the acidic and humid conditions often encountered in sugar processing environments. This ensures long-term durability and minimal maintenance. Another significant feature is the integration of advanced control systems that allow for precise regulation of air pressure and flow rates. This control capability enables operators to adjust the conveying speed according to production needs, optimizing energy consumption and reducing operational costs. The equipment also includes safety features like overload protection and automatic shut-off mechanisms, which prevent damage to the system and ensure safe operation. Furthermore, the pneumatic conveying systems are designed to minimize dust generation, which is crucial for maintaining a clean and safe working environment in sugar processing facilities. The low noise operation of these machines also contributes to a more pleasant working atmosphere, reducing the impact on personnel health. The systems are also equipped with self-cleaning mechanisms that prevent material buildup in the pipes, ensuring consistent performance over time. This feature is particularly important in sugar processing, where product contamination can occur if the system is not properly maintained. The advanced filtration systems in the equipment help to capture fine sugar particles, preventing them from entering the air exhaust and ensuring compliance with environmental standards. Additionally, the systems are designed for easy maintenance, with accessible components that allow for quick repairs and replacements, reducing downtime and increasing overall operational efficiency.

Application Examples and Operational Benefits
Real-world applications of sugar material pneumatic conveying machines demonstrate their effectiveness in improving operational efficiency and product quality. In a large-scale sugar refinery, the system was implemented to transport raw sugar from the storage silos to the refining unit. The system's high conveying capacity and low maintenance requirements resulted in a 20% reduction in labor costs and a 15% increase in production output compared to traditional manual handling methods. The reduced dust generation also improved the working conditions for employees, leading to fewer respiratory issues and increased job satisfaction. In another case, a sugar processing plant used the system to transport refined sugar from the crystallization tank to the packaging line. The system's ability to handle fine granules without breaking them maintained the product's quality, which was crucial for meeting export standards. The energy-efficient design of the system also contributed to a 10% reduction in electricity consumption, lowering the plant's operational costs. These examples highlight the operational benefits of using pneumatic conveying systems in sugar processing, including improved productivity, reduced costs, and enhanced product quality. The systems are also scalable, allowing companies to expand their operations without significant additional investment in new equipment. This flexibility makes them an attractive solution for both small and large-scale sugar processing facilities.
Conclusion and Future Developments
Sugar material pneumatic conveying machines, as developed by HeadPowder, represent a reliable and efficient solution for handling sugar materials in various industrial applications. The systems are designed to meet the specific demands of the sugar industry, ensuring optimal performance, minimal product degradation, and compliance with environmental regulations. With their advanced features and adaptability, these machines contribute to improved operational efficiency and product quality in sugar processing facilities. As the sugar industry continues to evolve, the development of more advanced pneumatic conveying systems, such as those with intelligent control systems and automated monitoring, will further enhance their performance and reliability. HeadPowder remains committed to providing innovative solutions that address the unique challenges of the sugar processing industry, ensuring that their equipment continues to meet the evolving needs of their clients.