

Principles and Working Scene Characteristics of Multi-functional Bulk Material Pneumatic Conveying E
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in Shandong, China, specializes in the design, development, and production of advanced multi-functional bulk material pneumatic conveying equipment. This article delves into the fundamental principles behind these systems and highlights the key working scene characteristics that make them indispensable in various industrial applications.
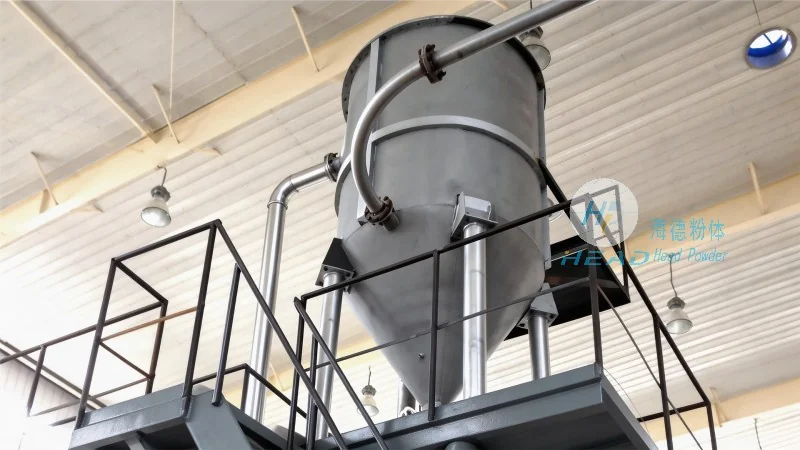
Understanding the Core Principles of Pneumatic Conveying Systems
The multi-functional bulk material pneumatic conveying equipment operates on the principle of using air as the medium to transport bulk materials from one location to another. Unlike traditional mechanical conveying methods, such as belt conveyors or screw conveyors, pneumatic systems utilize a pressurized or vacuum environment to move materials through a pipeline network. The core components typically include a blower or vacuum pump, a hopper for material storage, a conveyor line, and a control system. The system can function in either positive pressure (blowing air to push material) or negative pressure (sucking air to draw material) modes, offering flexibility based on the specific material characteristics and operational requirements.
Key to the efficiency of these systems is the selection of the appropriate air velocity and pipeline diameter. The air velocity must be sufficient to overcome the frictional forces and gravitational effects acting on the material particles, ensuring stable and continuous flow. For different materials with varying densities, particle sizes, and flow properties, the system design is tailored to maintain optimal air-to-material ratios. This balance is crucial for preventing material deposition, blockages, or excessive energy consumption. The control system plays a vital role in regulating the air pressure, flow rate, and material feed rate, enabling precise and automated operation that adapts to changing production demands.
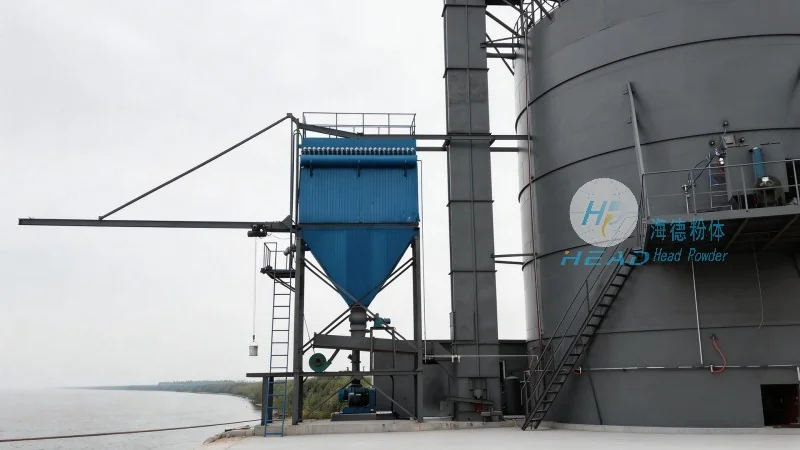
Working Scene Characteristics Across Diverse Industrial Applications
The versatility of multi-functional bulk material pneumatic conveying equipment is evident in its widespread adoption across numerous industrial sectors. In the food and pharmaceutical industries, where hygiene and contamination control are paramount, these systems offer enclosed, dust-free environments that comply with stringent regulatory standards. The equipment can handle sensitive materials like powders, granules, and fine particles without compromising quality or safety. For example, in a food processing plant, the system efficiently transports flour, sugar, or spices from storage silos to production lines, maintaining product integrity and preventing cross-contamination.
In the chemical and petrochemical industries, the equipment is used to transport abrasive or corrosive materials, such as powders, slurries, or bulk chemicals. The robust construction of the pipelines and components ensures durability under harsh conditions, while the pneumatic design minimizes the risk of material leakage or environmental exposure. The system's ability to handle high-temperature or high-pressure materials makes it suitable for processes like chemical synthesis or petrochemical refining, where precise material transfer is critical for process efficiency and safety.
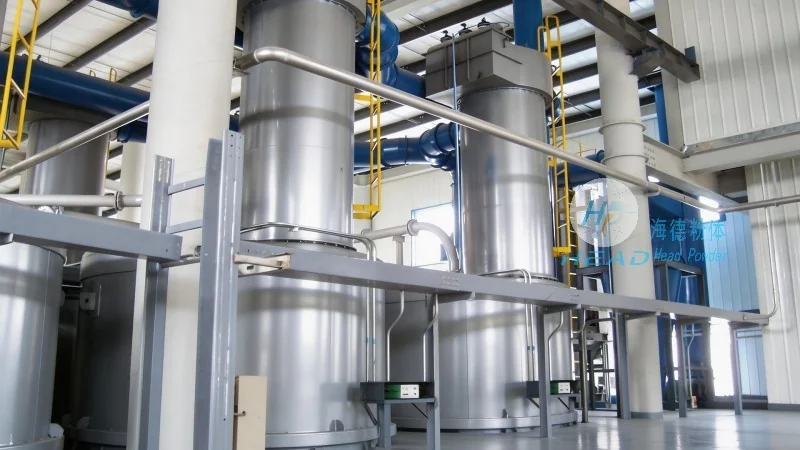
In the mining and mineral processing sector, the equipment is employed to transport raw ores, crushed rocks, or tailings from mining sites to processing facilities. The high-capacity and long-distance conveying capabilities of the system reduce transportation costs and improve operational efficiency. The system's adaptability to various material types, including heavy and abrasive minerals, ensures reliable performance even in challenging mining environments. Additionally, the enclosed design helps in controlling dust emissions, contributing to better occupational health and environmental compliance.
In the cement and construction materials industry, the equipment is utilized to transport raw materials like limestone, clay, or cement clinker from storage to production lines. The system's ability to handle large volumes of bulk materials at high speeds enhances production throughput, making it an essential component in cement manufacturing plants. The pneumatic conveying system also reduces the need for manual handling and reduces the risk of material spillage, improving overall operational safety and productivity.
Advantages and Practical Considerations in Real-World Operations
Multi-functional bulk material pneumatic conveying equipment offers several advantages that make it a preferred choice over traditional conveying methods. The primary benefit is the ability to handle a wide range of materials, including fine powders, granules, and bulk solids, with minimal maintenance requirements. The enclosed system design reduces dust emissions, improving workplace safety and environmental sustainability. Additionally, the system's flexibility allows for easy integration into existing production lines, enabling seamless material transfer without the need for extensive infrastructure modifications.
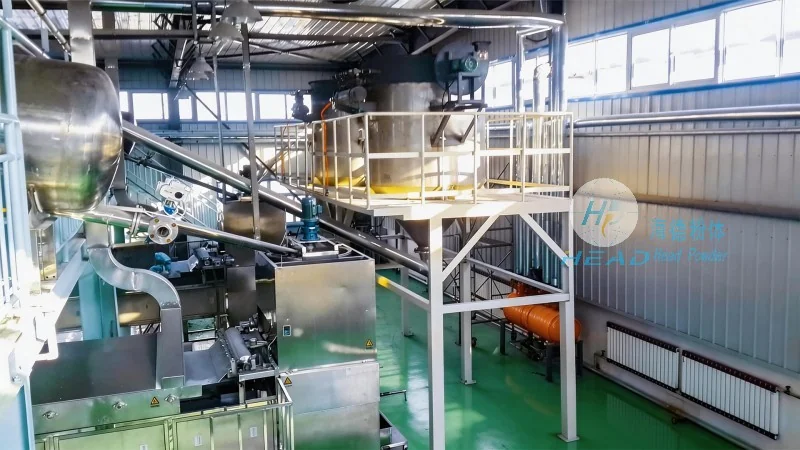
However, the effective operation of these systems requires careful consideration of several practical factors. The selection of the appropriate air velocity and pipeline diameter is critical to prevent material blockages or excessive energy consumption. Regular maintenance of the blower, vacuum pump, and control system is essential to ensure optimal performance and longevity. The system's design must also account for the material's flow properties, such as angle of repose and cohesive forces, to maintain stable flow and prevent agglomeration. In addition, the system's capacity and distance capabilities must be matched to the specific production requirements to avoid underutilization or overloading.
Overall, the multi-functional bulk material pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. represents a sophisticated solution for efficient and reliable material handling across diverse industrial applications. By leveraging the principles of pneumatic transport and incorporating advanced control technologies, these systems provide a versatile and cost-effective approach to meeting the demanding requirements of modern industrial operations.