

Principle and Working Scene Characteristics of Paddy Husk Ash Powder Pneumatic Conveying System
For industries dealing with paddy husk ash, efficient and reliable material handling is crucial. The paddy husk ash powder pneumatic conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., offers a sophisticated solution to meet these demands. This article explores the fundamental principles and operational characteristics of such systems, highlighting their practical applications and benefits.
Understanding the Core Principle of Pneumatic Conveying
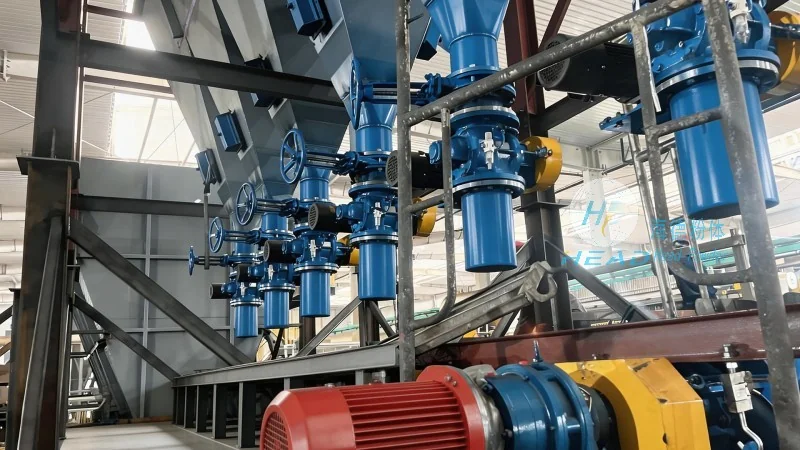
The pneumatic conveying system for paddy husk ash powder operates on the principle of transporting dry bulk materials through a pressurized or vacuumed air stream. Unlike traditional mechanical conveying methods, this system uses air as the medium to move the powder, eliminating the need for mechanical components like belts or buckets that may cause wear and tear or contamination. The system typically consists of a hopper for material storage, a conveyor line (either positive or negative pressure), and a receiver for the discharged material. The air flow is controlled by a blower or vacuum pump, which creates the necessary pressure differential to move the powder from the source to the destination. This method ensures a clean, dust-free transfer process, which is essential for maintaining the quality of paddy husk ash, a material often used in industrial applications like cement production, fertilizer manufacturing, or as a fuel source.
Key Working Scene Characteristics
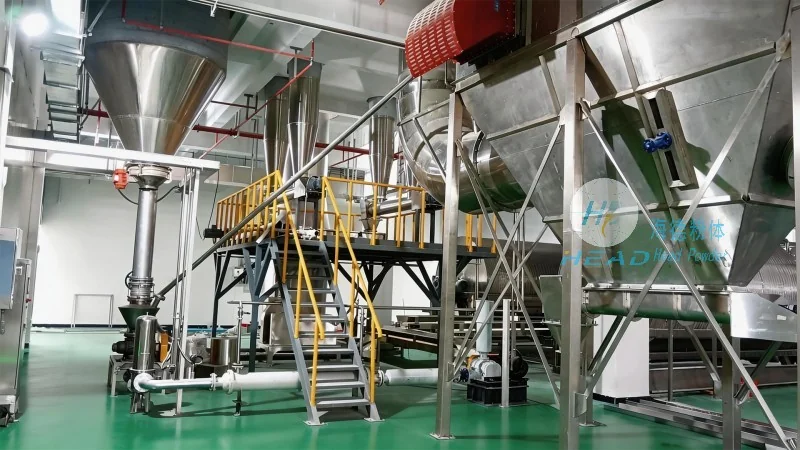
The effectiveness of a paddy husk ash powder pneumatic conveying system is heavily influenced by its working scene characteristics. These include the material's properties, the distance and elevation changes between the source and destination, and the required flow rate. For instance, the system's design must account for the density and particle size of paddy husk ash, as these factors affect the air velocity needed for efficient transport. In scenarios where the material is to be conveyed over long distances or through multiple bends, the system may incorporate pulse-jet or rotary airlock valves to maintain consistent flow and prevent blockages. Additionally, the system's ability to handle variations in ash quality, such as moisture content or impurity levels, is crucial for maintaining operational stability. The working scene characteristics also dictate the choice between positive and negative pressure systems. Positive pressure systems are ideal for short to medium distances and when the material needs to be transported to a higher elevation, as they generate sufficient pressure to push the powder through the line. Conversely, negative pressure systems are suitable for long-distance or when the material must be drawn from a lower elevation, as they create a vacuum to pull the powder. The system's flexibility in adapting to different working conditions makes it a versatile solution for various industrial settings.
Practical Applications and Benefits
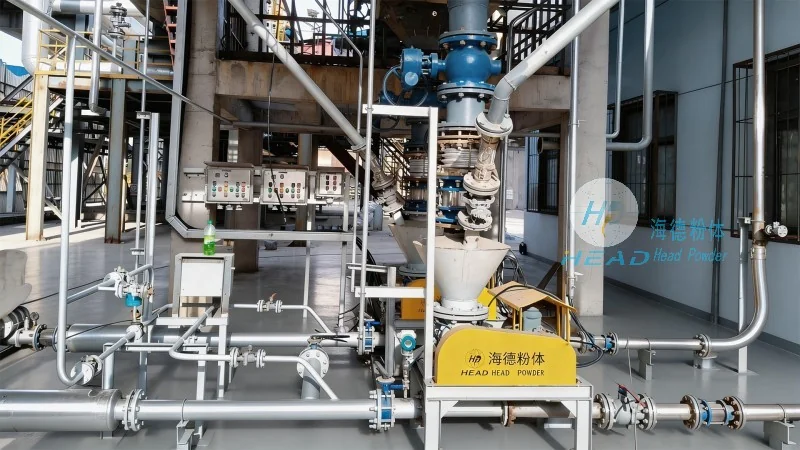
Shandong HeadPowder Engineering Co., Ltd.'s paddy husk ash powder pneumatic conveying systems are widely used in several industrial applications. One primary application is in the cement industry, where paddy husk ash is used as a supplementary cementitious material (SCM) to improve the properties of concrete, such as reducing water demand and enhancing durability. The pneumatic conveying system ensures that the ash is delivered to the cement plant in a consistent and controlled manner, which is critical for maintaining the quality of the final product. Another significant application is in the fertilizer industry, where paddy husk ash is processed into organic fertilizers. The system efficiently transports the ash from storage silos to processing units, minimizing dust generation and ensuring a smooth production flow. Additionally, in power generation plants, paddy husk ash can be used as a fuel or co-fuel in boilers. The pneumatic conveying system enables the ash to be transported from the boiler to the ash handling facilities without the need for manual handling, which improves safety and operational efficiency. The benefits of using such a system extend beyond material handling efficiency. By reducing manual labor and minimizing the risk of dust exposure, the system enhances workplace safety. Furthermore, the clean and dust-free transfer process helps maintain the purity of the paddy husk ash, which is essential for its intended applications. The system's ability to handle varying material loads and flow rates also contributes to its cost-effectiveness, as it reduces downtime and maintenance costs associated with traditional mechanical conveying systems.
Company Overview and Expertise
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized engineering solutions for powder handling and material transport. With a focus on innovation and customer-centric design, the company has developed advanced pneumatic conveying systems tailored to the unique needs of industries dealing with paddy husk ash and other fine powders. The company's expertise lies in understanding the complex properties of different powders and designing systems that optimize material flow, minimize energy consumption, and ensure operational reliability. Headpowder's team of engineers and technicians work closely with clients to assess their specific requirements, from initial material analysis to system installation and maintenance. This collaborative approach ensures that the final solution is not only efficient but also tailored to the client's operational environment. The company's commitment to quality is reflected in its adherence to international standards and rigorous testing protocols, which guarantee the performance and safety of its systems. With a strong presence in China, particularly in Shandong, headpowder has established itself as a trusted partner for industries seeking reliable and sustainable powder handling solutions.