

Principle and Working Scene Characteristics of Activated Carbon Powder Material Handling System Equi
Activated carbon powder is widely used in various industrial processes, and the efficient transportation of this fine powder is crucial for maintaining production efficiency and product quality. The material handling system equipment designed by Shandong HeadPowder Engineering Co., Ltd. addresses these challenges with advanced technology and robust design. This article explores the underlying principles of the system and highlights its key working scene characteristics.
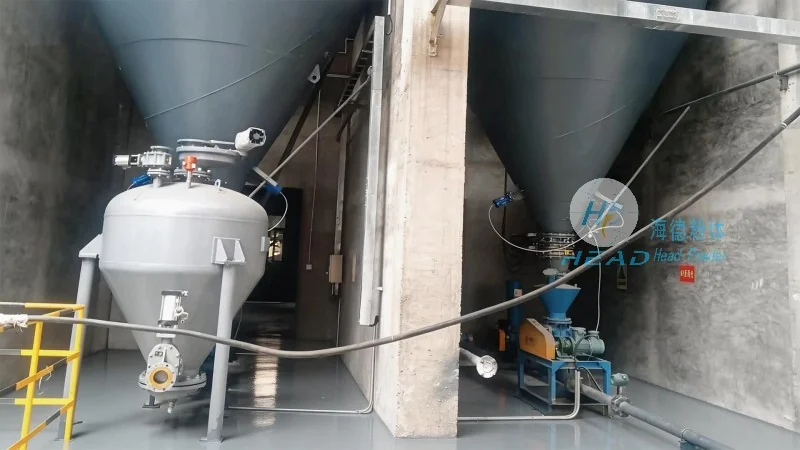
Company Background and Expertise
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the development and production of high-quality material handling solutions. With years of experience in the industry, the company has built a strong reputation for delivering reliable and efficient equipment tailored to the unique needs of different sectors. The company's commitment to innovation and customer satisfaction has enabled it to become a trusted partner for businesses requiring advanced powder handling systems.
Principle of Activated Carbon Powder Material Handling System
The core principle of the activated carbon powder material handling system is to ensure the safe, efficient, and controlled transportation of fine powders. The system typically incorporates several key components, including feeders, conveyors, and dust collection systems, all working in harmony to minimize material loss and prevent contamination. The design focuses on maintaining the integrity of the activated carbon powder, which is essential for its performance in applications such as air purification, water treatment, and chemical processing. By utilizing advanced engineering techniques, the system ensures consistent flow rates and reduces the risk of clogging or blockages that are common in traditional powder handling methods.
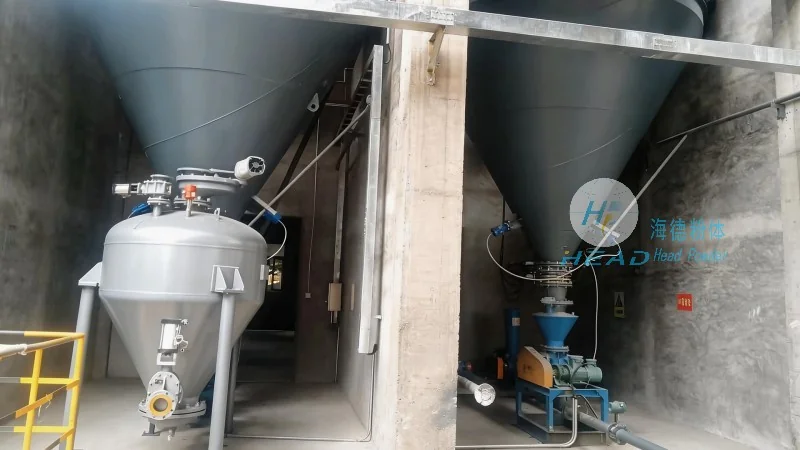
Working Scene Characteristics
The activated carbon powder material handling system is designed to operate effectively in diverse industrial environments. Its adaptability makes it suitable for applications in chemical plants, pharmaceutical facilities, and environmental treatment centers. The system's ability to handle high volumes of fine powder while maintaining low dust emissions is a significant advantage in these settings. Additionally, the system's modular design allows for easy integration into existing production lines, reducing downtime and installation costs. In industrial settings where material handling efficiency directly impacts production output, this system provides a reliable solution that enhances operational performance.
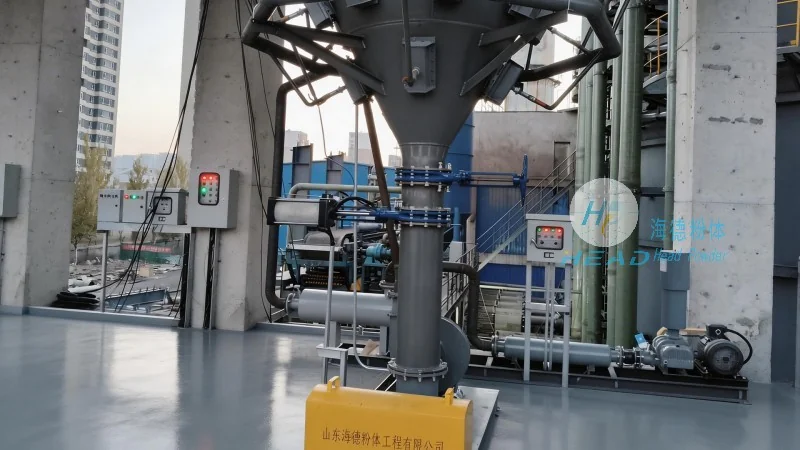
Key Features and Benefits
Shandong HeadPowder Engineering Co., Ltd. has incorporated several features into the activated carbon powder material handling system to enhance its functionality and user experience. These include adjustable speed controls, which allow operators to optimize the flow rate based on specific application requirements. The system also features robust construction materials, ensuring durability and longevity even in harsh industrial conditions. Another notable benefit is the reduced risk of dust-related health hazards, as the enclosed design minimizes airborne particles. This not only improves workplace safety but also complies with environmental regulations, making it a responsible choice for modern industrial operations.
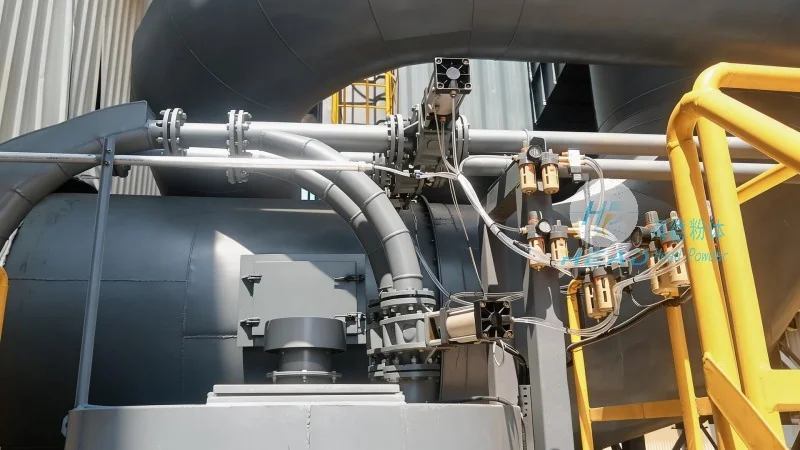
Application Examples
The versatility of the activated carbon powder material handling system is demonstrated through its application in various industries. In the chemical industry, the system is used to transport activated carbon for adsorption processes, where consistent material flow is critical for achieving desired purification levels. In pharmaceutical manufacturing, the system ensures the safe handling of activated carbon used in filtration and purification stages, maintaining product purity and meeting stringent quality standards. Environmental treatment facilities also benefit from the system's ability to handle large quantities of activated carbon for water and air purification, contributing to improved environmental outcomes.
Conclusion
Shandong HeadPowder Engineering Co., Ltd.'s activated carbon powder material handling system represents a significant advancement in industrial material handling technology. By combining advanced engineering principles with practical design, the system addresses the unique challenges of transporting fine powders while ensuring operational efficiency and safety. The company's expertise and commitment to quality make it a leading provider of such solutions, catering to the diverse needs of industries worldwide. For businesses seeking reliable and efficient material handling equipment, this system offers a proven solution that enhances productivity and maintains product integrity.