

Principles and Working Scene Characteristics of Continuous Quantitative Material Conveying System Eq
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer specializing in the research, development, and production of continuous quantitative material conveying systems. The company is headquartered in Shandong, China, and has established a solid reputation in the industry for its advanced technology and reliable products. HeadPowder focuses on providing high-quality solutions for material handling and processing, catering to diverse industrial applications.
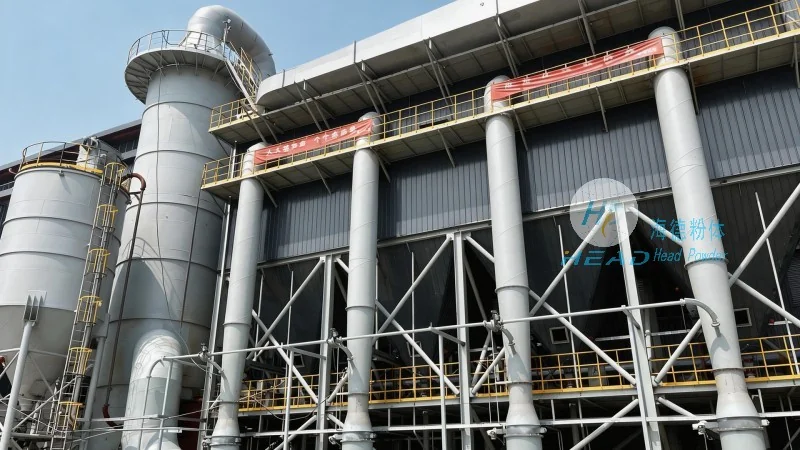
Principles of Continuous Quantitative Material Conveying Systems
Continuous quantitative material conveying systems are designed to transport bulk materials in a controlled and precise manner. The core principle involves the integration of conveyor mechanisms, feeding devices, and quantitative control units. These systems typically utilize screw conveyors, belt conveyors, or pneumatic conveying technologies to move materials from one location to another. The quantitative control component, often an adjustable screw or a variable-speed motor-driven feeder, ensures that the material is delivered at a consistent rate. This precision is crucial for applications where accurate material measurement and uniform delivery are essential. The system's design allows for seamless operation, minimizing downtime and maximizing efficiency in material handling processes.
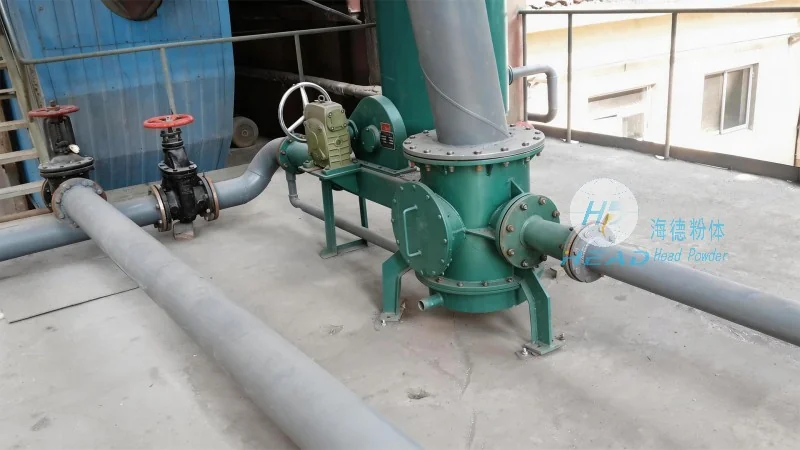
Working Scene Characteristics and Application Scenarios
The working scene characteristics of continuous quantitative material conveying systems are tailored to meet the demands of various industrial environments. These systems are commonly used in sectors such as food processing, pharmaceuticals, chemicals, and mining. In food processing, for example, the systems ensure hygienic and accurate delivery of ingredients, maintaining product quality and compliance with safety standards. In the pharmaceutical industry, the precision of these systems is vital for delivering raw materials to production lines, where consistency is paramount. The systems are also employed in chemical plants for handling powders and granules, where controlled dosing is necessary to prevent contamination and ensure process stability. Additionally, in mining operations, the equipment aids in transporting ore and other bulk materials efficiently, supporting large-scale production. The versatility of these systems allows them to adapt to different working conditions, from indoor processing facilities to outdoor industrial sites, making them a reliable choice for diverse operational needs.
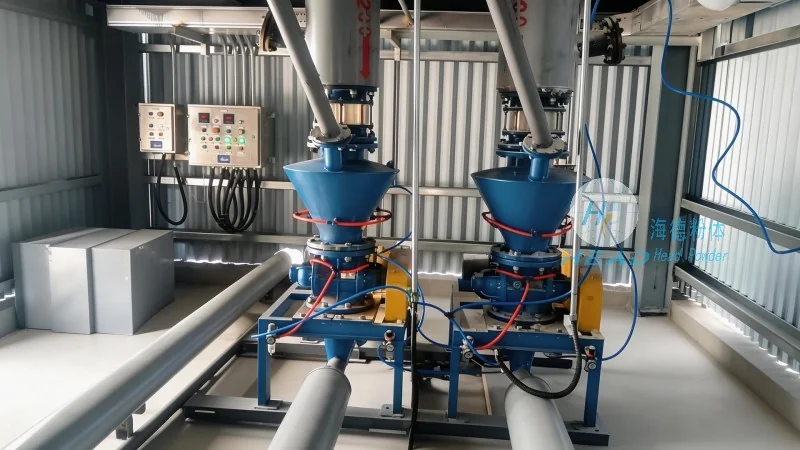
Advantages in Practical Applications
When integrated into industrial workflows, continuous quantitative material conveying systems offer several key advantages. Firstly, they enhance operational efficiency by providing consistent and reliable material delivery, reducing the need for manual intervention and minimizing errors. The automated quantitative control reduces labor costs and improves overall productivity. Secondly, the systems contribute to improved product quality by ensuring uniform material distribution, which is critical in processes where material consistency directly impacts final product characteristics. This is particularly important in industries like food and pharmaceuticals, where product quality is a top priority. Thirdly, the design of these systems promotes safety and compliance with industry regulations. The enclosed conveyor mechanisms and controlled feeding systems help prevent dust emissions and material spillage, creating a safer working environment. Furthermore, the modular design of many HeadPowder systems allows for easy customization and integration with existing production lines, providing flexibility for evolving operational requirements. These advantages make continuous quantitative material conveying systems an essential component in modern industrial operations, supporting companies in achieving higher efficiency, better quality control, and enhanced safety standards.