

[Principle and Working Scene Characteristics of Tonne Bag Material Conveying Lines]
Shandong HeadPowder Engineering Co., Ltd., a prominent engineering firm headquartered in Shandong, China, specializes in the development of advanced material handling solutions. The company focuses on creating efficient and reliable conveying systems, particularly those designed for the transport of bulk materials from tonne bags. These systems are engineered to meet the demands of various industrial sectors, ensuring safe, consistent, and high-volume material transfer.
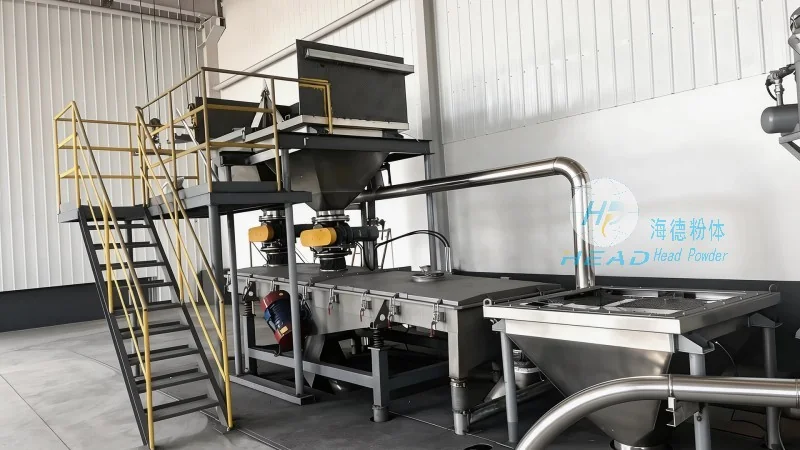
The Principle of Tonne Bag Material Conveying Lines
A tonne bag material conveying line operates on a systematic principle that integrates multiple components to facilitate seamless material movement. The process typically begins with the loading of bulk materials into sturdy tonne bags, which are then placed on a designated feeding platform. An automated lifting mechanism, often powered by hydraulic or mechanical systems, elevates the tonne bag and activates a discharge valve, allowing the material to flow into a receiving hopper or conveyor. The conveying system, which may consist of screw conveyors, belt conveyors, or pneumatic transport units, then transports the material to its final destination. This integrated approach minimizes manual labor, reduces operational errors, and enhances overall efficiency by ensuring a continuous flow of materials.
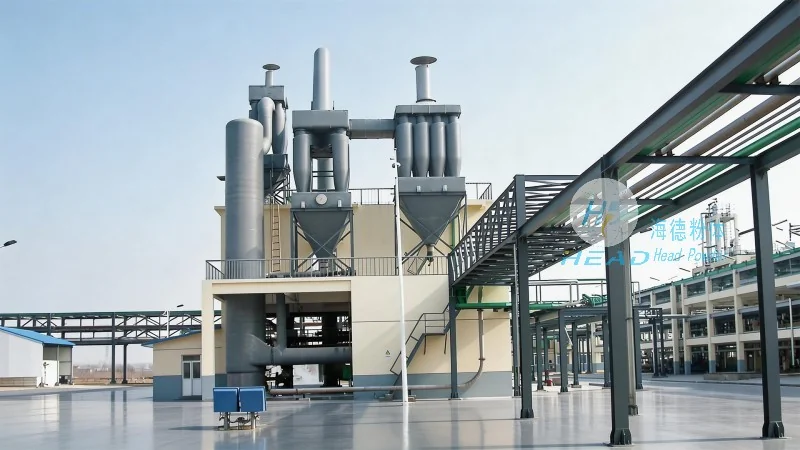
Key Components and Their Functions
Several critical components work in tandem to ensure the smooth operation of a tonne bag material conveying line. The tonne bag loading station is designed to securely hold and position the bags, preventing any movement during the lifting process. The lifting and discharge mechanism, which may include a hydraulic cylinder or a mechanical arm, is responsible for raising the bag to the correct height and opening the valve to release the material. The conveying system, tailored to the material's properties (e.g., granular, dusty, or cohesive), ensures effective transport. For example, screw conveyors are ideal for handling dry, free-flowing materials like sand or cement, while belt conveyors are suitable for bulkier materials such as gravel or coal. Pneumatic systems are often used for dusty or fine powders, utilizing air pressure to move the material through a pipeline.
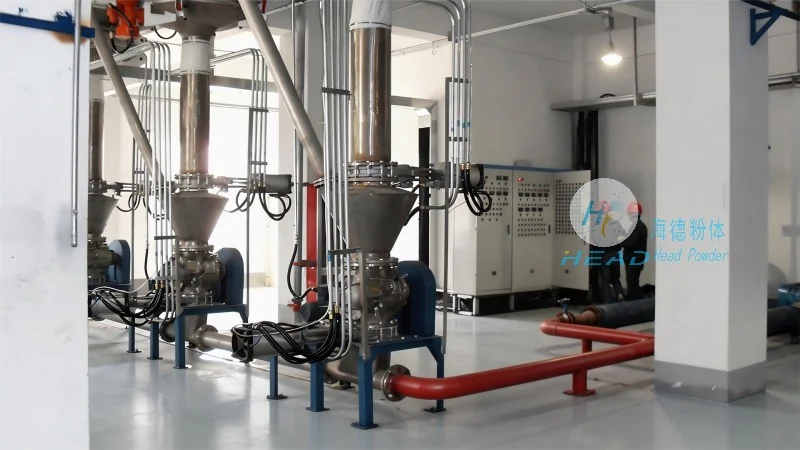
Working Scene Characteristics
The working scene characteristics of tonne bag material conveying lines are tailored to the specific requirements of different industrial environments. These systems are commonly employed in sectors such as mining, construction, and chemical processing, where large volumes of bulk materials need to be handled safely and efficiently. The design of the conveying line is adapted to the unique challenges of each application, including the type of material, the required throughput, and the available space. For instance, in mining operations, the conveying line may need to handle abrasive ores that can cause wear on components, requiring durable materials like stainless steel or high-grade alloys for the conveyor parts. In construction sites, the system might transport cement or sand, where the focus is on maintaining a consistent flow and preventing material buildup in the conveying path. The flexibility of the system allows for customization, ensuring that it can be integrated seamlessly into existing production lines or new installations.
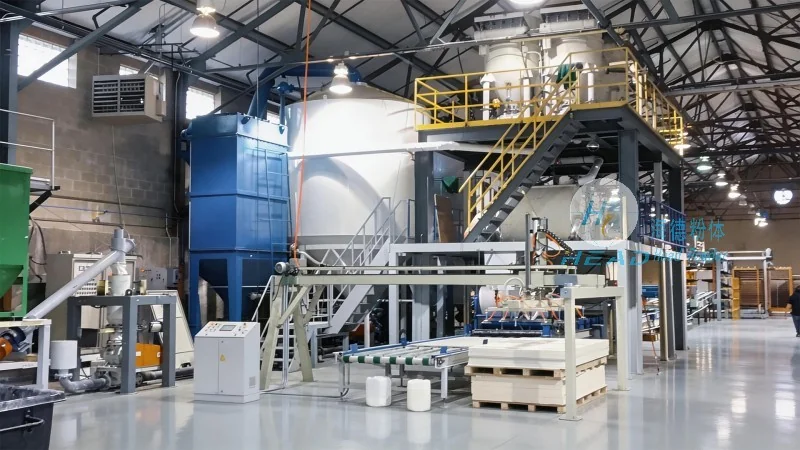
Advantages in Industrial Applications
Implementing a tonne bag material conveying line offers several advantages in industrial settings. Firstly, it significantly reduces labor costs by automating the material handling process, as the system can operate continuously without the need for constant human supervision. Secondly, it minimizes material loss and contamination, as the sealed tonne bags prevent dust or moisture from escaping during transport. Thirdly, the system enhances safety by reducing the risk of manual handling, which can lead to injuries. Additionally, the consistent and high-volume transport capability ensures that production lines operate at optimal efficiency, reducing downtime and increasing overall productivity. These benefits make tonne bag material conveying lines a preferred choice for industries that require reliable and efficient bulk material transport.