

Principles and Working Scene Characteristics of Waste Powder Conveying System Equipment
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer based in Shandong, China. The company specializes in the design, development, and production of advanced waste powder conveying systems, catering to various industrial needs. This article explores the fundamental principles behind these systems and highlights the key characteristics of their working environments.
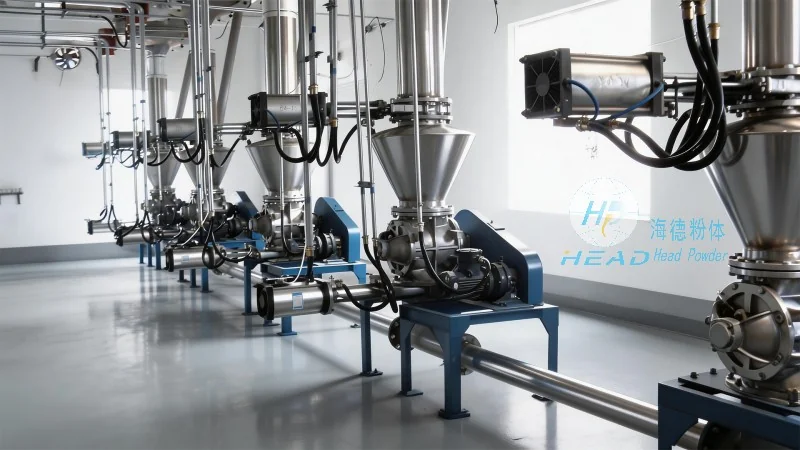
The Core Principles of Waste Powder Conveying Systems
Waste powder conveying systems are engineered to efficiently transport bulk powders, including waste materials from municipal or industrial sources. The primary principle revolves around the use of mechanical or pneumatic mechanisms to move powders through pipelines or other conduits. These systems typically incorporate components such as feeders, conveyors, and control units, which work in tandem to ensure consistent and reliable material handling. The design of the system is tailored to handle the specific properties of the waste powder, such as particle size, moisture content, and flowability, ensuring optimal performance and minimal operational issues.
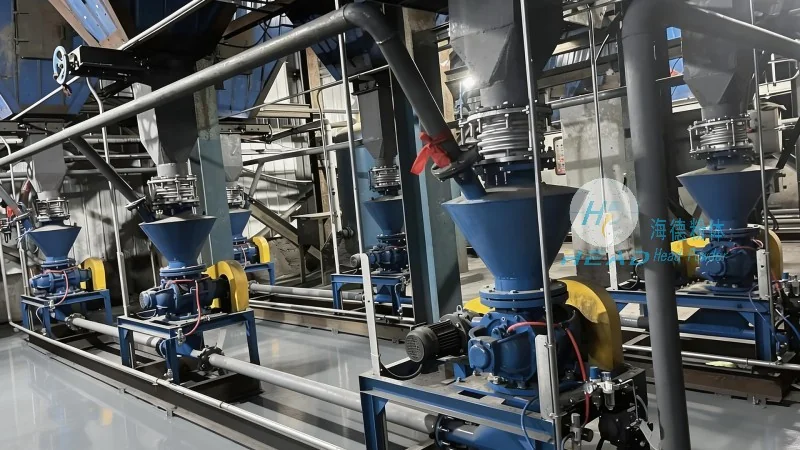
Key Characteristics of Working Scenarios for Waste Powder Conveying Systems
The working scenarios of waste powder conveying systems vary significantly based on the application and the nature of the waste material. For instance, in municipal waste management, these systems are often used to transport solid waste from collection sites to processing facilities. The working environment in such cases may involve high volumes of material, varying particle sizes, and potentially challenging conditions like dust or moisture. In industrial settings, the systems may handle waste from manufacturing processes, such as metal powders or chemical residues, where precision and cleanliness are critical. The characteristics of the working environment, including space constraints, ambient conditions, and safety requirements, directly influence the design and selection of the conveying system. HeadPowder's solutions are designed to adapt to these diverse scenarios, ensuring compatibility with the specific operational demands and environmental factors.
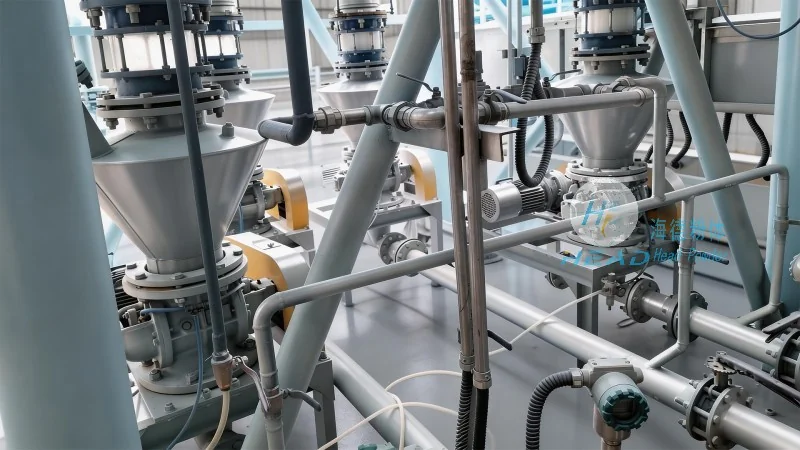
Key Advantages and Application Examples
HeadPowder's waste powder conveying systems offer several advantages that make them suitable for a wide range of applications. One of the primary benefits is their ability to handle large volumes of material with minimal human intervention, reducing labor costs and improving operational efficiency. The systems are also designed for low maintenance, with components that are easy to replace and inspect, ensuring long-term reliability. Additionally, the systems can be customized to meet specific operational requirements, such as varying conveyor speeds or material handling capacities. For example, in a municipal waste processing plant, the system might be configured to handle 100 tons of waste per hour, while in an industrial setting, it could be adjusted to process smaller batches of high-value materials. The adaptability of HeadPowder's systems allows them to be integrated into existing infrastructure or new projects, providing a flexible solution for waste management needs.