

Inert Gas Circulation Powder Conveying System Equipment: Principles and Application Scenario Feature
Efficient and reliable powder handling is a critical requirement in various industrial sectors, particularly those dealing with materials that are sensitive to air exposure or require precise control over the conveying process. The Inert Gas Circulation Powder Conveying System Equipment, developed by Shandong HeadPowder Engineering Co., Ltd., addresses these challenges through a sophisticated design that ensures safe, clean, and efficient material transport. This system leverages inert gas to create a sealed environment, preventing contamination and maintaining the integrity of the powder being handled.
Principles of the Inert Gas Circulation Powder Conveying System
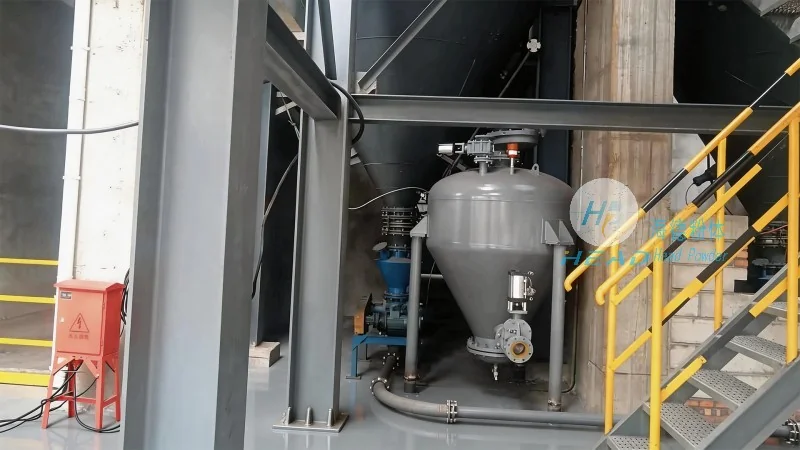
The core principle of this system is the creation of a closed-loop inert gas environment that isolates the powder from external air. By circulating an inert gas, such as nitrogen or argon, through the conveying lines and storage vessels, the system maintains a positive pressure that prevents oxygen and moisture from entering. This not only protects the powder from oxidation or degradation but also ensures that the material remains free from contaminants. The system operates by using a combination of positive displacement blowers or rotary lobe pumps to move the powder through the pipeline, with the inert gas acting as the medium that carries the material while maintaining the sealed conditions. The design incorporates pressure sensors and gas flow meters to monitor the system's performance, ensuring optimal operation and safety. Additionally, the system features automatic pressure relief valves and gas leak detection systems to prevent any potential hazards, making it a safe and reliable solution for handling sensitive powders.
Key Features and Application Scenarios
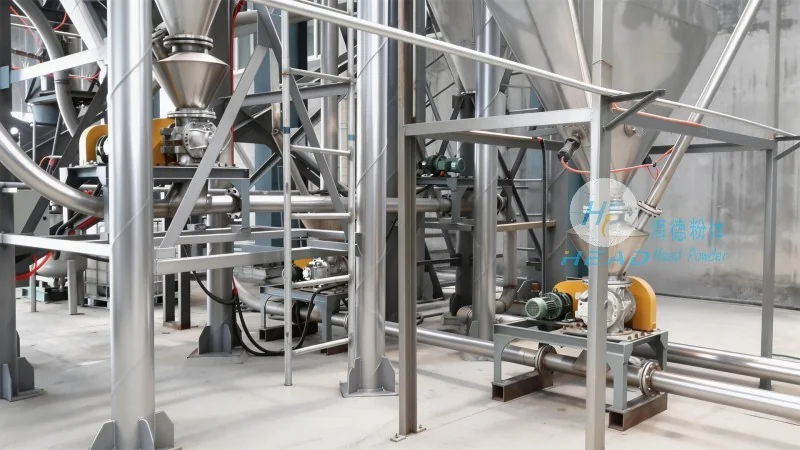
The Inert Gas Circulation Powder Conveying System is designed to meet the diverse needs of industries that require precise control over powder handling. Its primary features include: a fully sealed conveying system that eliminates the risk of contamination; adjustable flow rates to accommodate different powder types and processing requirements; and the ability to handle a wide range of particle sizes and bulk densities. The system is particularly suitable for applications in pharmaceuticals, food processing, chemical manufacturing, and specialty materials, where the quality and purity of the powder are paramount. For example, in pharmaceutical production, the system can be used to transport active pharmaceutical ingredients (APIs) or excipients without exposing them to air, ensuring that the final product meets stringent quality standards. In the food industry, it can handle powders like cocoa, sugar, or milk powder, maintaining their freshness and preventing spoilage. The system's flexibility also makes it suitable for research and development laboratories, where precise control over material handling is essential for experimental accuracy.
About Shandong HeadPowder Engineering Co., Ltd.
As a leading manufacturer of powder handling equipment, Shandong HeadPowder Engineering Co., Ltd. specializes in providing innovative solutions for industrial material transport. With a focus on quality, safety, and efficiency, the company has developed a range of products that cater to the unique needs of various industries. HeadPowder's expertise in inert gas technology and powder handling systems has enabled them to deliver reliable and durable equipment that meets international standards. The company's facilities are located in Shandong, China, where they leverage advanced manufacturing processes and rigorous quality control measures to ensure that each product meets the highest standards. By combining technical expertise with customer-centric approach, HeadPowder has established itself as a trusted partner for businesses seeking efficient and safe powder conveying solutions.