

Principles and Working Scene Characteristics of Sugar Powder Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced sugar powder conveying equipment. This equipment is engineered to efficiently handle the transportation of sugar powders in various industrial applications, ensuring optimal performance and reliability. The following sections will explore the fundamental principles behind these systems and the specific working scenarios where they are most effectively utilized.
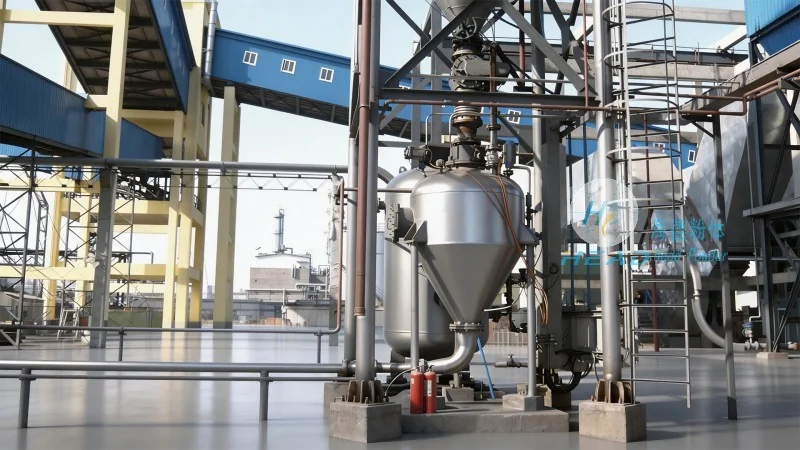
Principles of Powder Conveying Systems
The core principle of sugar powder conveying equipment revolves around the use of mechanical or pneumatic methods to transport granular or powdered materials like sugar. These systems are designed to maintain the integrity of the material while minimizing dust generation and ensuring consistent flow rates. Key components typically include feed hoppers, conveying pipes, control valves, and dust collection systems. The mechanical conveying systems often employ screw conveyors, belt conveyors, or bucket elevators, which rely on rotational motion to move the powder. In contrast, pneumatic conveying systems utilize air pressure to transport the material through pipelines, offering flexibility in layout and the ability to handle materials with higher moisture content or sensitivity to moisture.
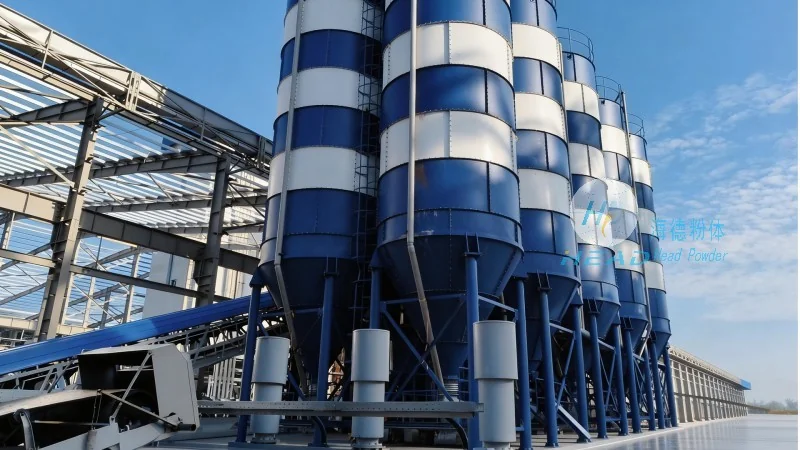
Working Scene Characteristics
The effectiveness of sugar powder conveying equipment is heavily influenced by the specific working environments in which they operate. These characteristics include the scale of production, the type of sugar being handled (e.g., white sugar, brown sugar, or raw sugar), and the overall process flow within the facility. In large-scale sugar processing plants, these systems are critical for integrating different stages of production, from raw sugar storage to processing lines, where it undergoes refining and crystallization. The working scenes may involve high-volume, continuous operation, requiring equipment that can handle large quantities of material without compromising on speed or accuracy. Additionally, the equipment must be adaptable to different sugar types, as each may have unique properties affecting flowability and dust generation. For instance, handling fine white sugar requires equipment with smooth surfaces and minimal friction to prevent caking, while processing coarser brown sugar may necessitate more robust components to withstand the increased abrasion.
Application in Industrial Settings
HeadPowder's sugar powder conveying equipment is widely applied in various industrial settings, including sugar refineries, food processing plants, and chemical manufacturing facilities. In sugar refineries, these systems are essential for transporting raw sugar from storage silos to processing lines, where it undergoes refining and crystallization. The equipment must be capable of handling high temperatures and moisture, as the sugar may be in a semi-moist state during processing. In food processing plants, the equipment is used to move sugar for confectionery production, ensuring a consistent supply to mixing and packaging lines. The working scenes in these environments often involve tight integration with other processing equipment, requiring precise control over flow rates and material distribution. Furthermore, the equipment must meet strict hygiene standards, as sugar products are often consumed directly by consumers. This necessitates the use of stainless steel components and easy-to-clean designs, which are standard features in HeadPowder's equipment.
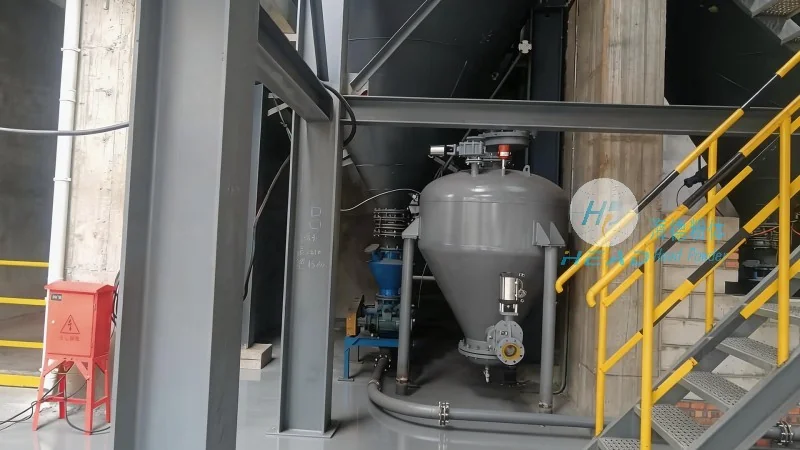
Advantages and Performance Metrics
When evaluating sugar powder conveying equipment, several key advantages and performance metrics are important to consider. These include the system's efficiency in terms of energy consumption, the ability to maintain material quality, and the ease of maintenance. HeadPowder's equipment is designed to minimize energy usage by optimizing the conveying speed and pressure, reducing operational costs for the end-user. The systems are also engineered to preserve the quality of the sugar, preventing contamination or degradation during transport. This is particularly important for high-value sugar products where purity is a critical factor. Maintenance is another critical aspect, as the equipment must be reliable and require minimal downtime. HeadPowder's designs incorporate easy access to components, allowing for quick inspections and repairs, which helps maintain consistent production schedules.