

Principles and Working Scene Characteristics of White Sugar Powder Conveying
White sugar powder conveying is a critical process in various industrial applications, particularly in the food and chemical sectors. The efficient and safe handling of white sugar powder requires a deep understanding of its conveying principles and the specific characteristics of different working environments. This article explores the fundamental principles behind white sugar powder conveying and highlights the key features of its application scenarios, providing insights into how these systems operate and where they are most effectively utilized.
Principles of White Sugar Powder Conveying
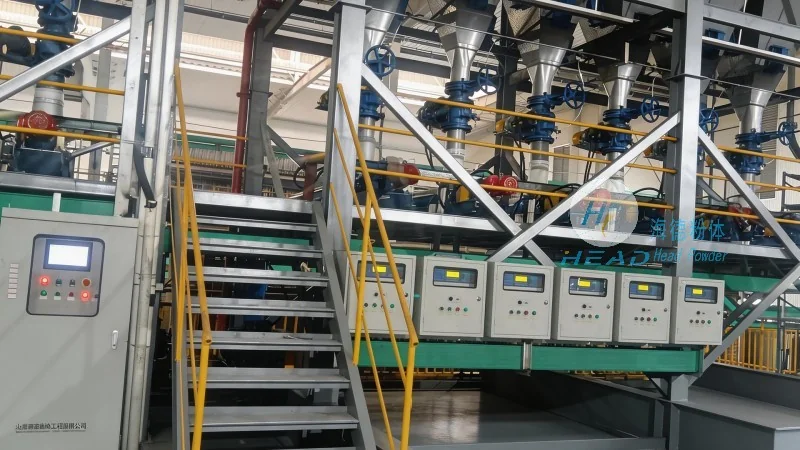
The core of white sugar powder conveying lies in the ability to transport fine particulate materials like white sugar from one location to another without compromising quality or safety. Two primary methods dominate the industry: pneumatic conveying and mechanical conveying. Pneumatic conveying uses air or gas to move the powder through a pipeline, while mechanical conveying employs equipment such as screw conveyors, belt conveyors, or bucket elevators to transport the material. Each method has its own advantages and is selected based on factors like material properties, distance, and system complexity. Pneumatic systems are particularly effective for long-distance transport and can handle fine powders that are prone to dusting or caking. Mechanical systems, on the other hand, are ideal for short distances and when the material needs to be handled in bulk, as they provide more direct control over the flow and can be integrated with other processing equipment.
Key Working Scene Characteristics
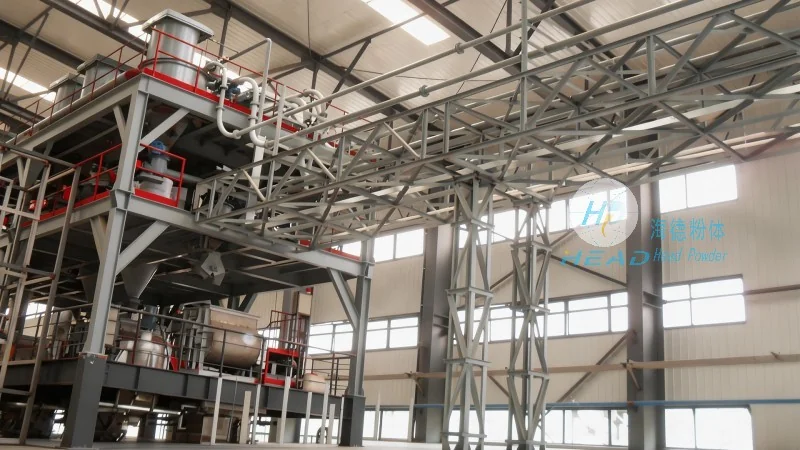
White sugar powder conveying systems are deployed in diverse working environments, each with unique requirements that influence system design and operation. In food processing facilities, for example, systems must adhere to strict hygiene standards and be easy to clean to prevent contamination. The working scene characteristics also include the scale of operation—whether it's a small-scale batch processing plant or a large-scale continuous production line—and the need for precise control over flow rates and material distribution. Additionally, the environmental conditions, such as temperature and humidity, play a role in determining the appropriate conveying technology and equipment materials. For instance, in tropical regions, systems may need to be designed to handle higher humidity levels to prevent moisture absorption by the white sugar, which could affect its quality and processing properties. In cold climates, insulation and temperature control may be necessary to maintain the sugar's crystalline structure and prevent freezing.
Company Introduction: Shandong HeadPowder Engineering Co., Ltd.
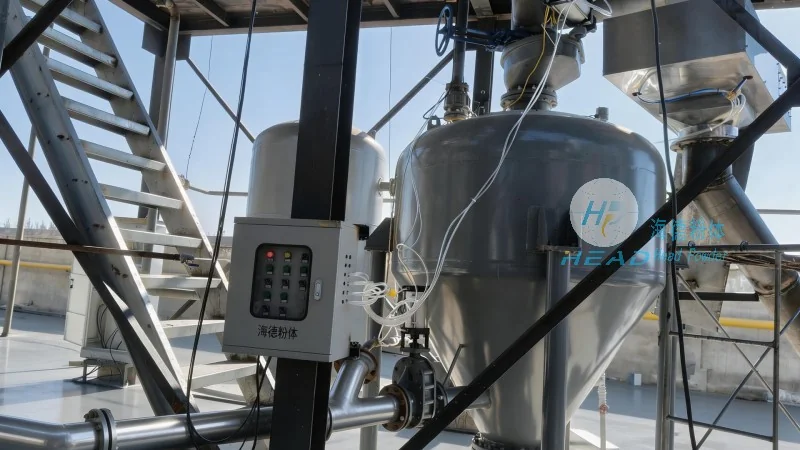
HeadPowder, a leading provider of powder handling solutions, specializes in designing and manufacturing advanced white sugar powder conveying systems. With a strong focus on innovation and customer-centric solutions, HeadPowder has established itself as a trusted partner in the industry. The company's expertise lies in integrating cutting-edge technology with practical application, ensuring that their systems not only meet but exceed the demands of modern white sugar processing facilities. HeadPowder's commitment to quality and reliability has made them a preferred choice for businesses seeking efficient and safe powder conveying solutions. The company's team of engineers and technicians work closely with clients to understand their specific needs and develop customized solutions that optimize performance and reduce operational costs.
Technical Advantages and Application Examples
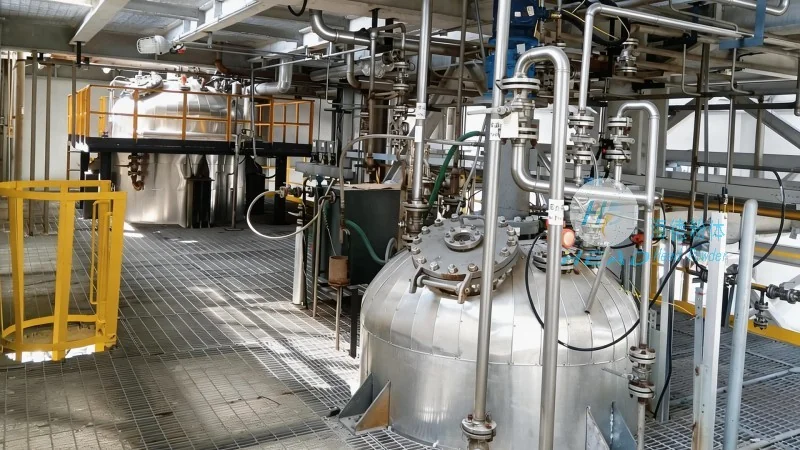
HeadPowder's white sugar powder conveying systems are engineered to address the specific challenges of handling fine, hygroscopic materials like white sugar. The systems are designed to minimize product degradation, prevent clogging, and maintain consistent flow rates. For instance, in large-scale sugar refineries, pneumatic conveying systems are used to transport white sugar from storage silos to processing lines, ensuring a continuous and reliable supply. In smaller food processing plants, mechanical conveyors may be employed for shorter distances or when space is limited. The versatility of HeadPowder's solutions allows them to adapt to various working scene characteristics, making them suitable for a wide range of applications. The company also offers advanced control systems that allow for real-time monitoring and adjustment of conveying parameters, enhancing operational efficiency and product quality. HeadPowder's commitment to continuous improvement ensures that their systems remain at the forefront of powder handling technology, providing clients with reliable and efficient solutions for their white sugar conveying needs.