

Working Principle and Features of Lithium Oxide Material Pneumatic Conveying System
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for handling lithium oxide materials. This article delves into the fundamental working principles and key characteristics of such systems, providing a comprehensive overview for industry professionals and potential clients.
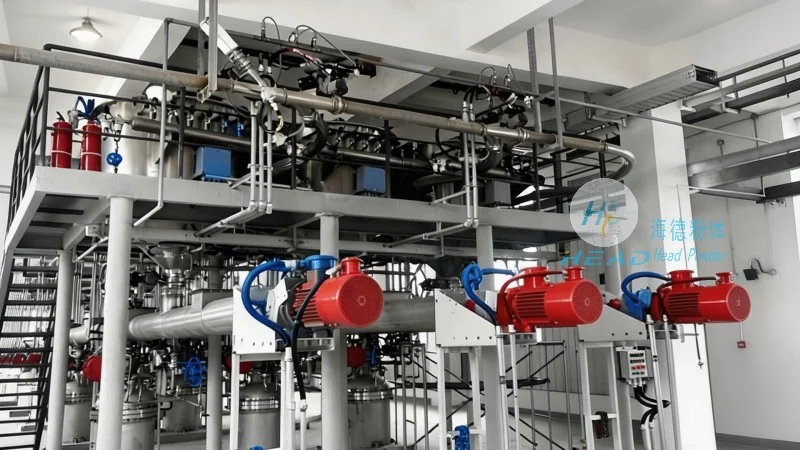
Understanding the Working Principle of Lithium Oxide Pneumatic Conveying Systems
The core mechanism of a lithium oxide pneumatic conveying system revolves around the use of compressed air or gas to transport bulk materials through a pipeline network. In this process, the material is introduced into the system at a feeding point, where it is then entrained by the moving air stream. The system typically operates under either positive or negative pressure, depending on the specific application requirements and material properties. For lithium oxide, which is often handled in powder or granular form, the system must be designed to prevent material degradation, caking, or dust generation, ensuring safe and efficient transport. The feeding mechanism, such as a rotary valve or a star feeder, controls the material flow rate, while the air flow is regulated by a blower or compressor to maintain optimal velocity and pressure within the pipeline. This combination of mechanical and pneumatic components ensures that the lithium oxide is conveyed smoothly from the source to the destination, minimizing downtime and operational risks.
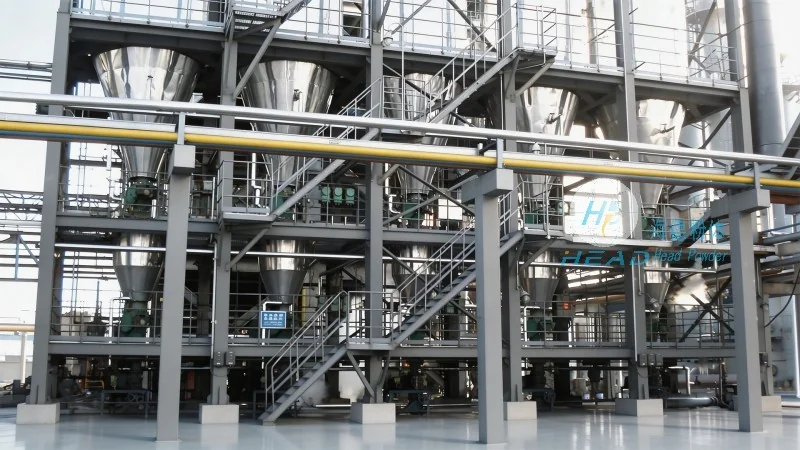
Key Features of Lithium Oxide Pneumatic Conveying Systems
Several distinct features make lithium oxide pneumatic conveying systems particularly suitable for handling this reactive and sensitive material. Firstly, the system is designed with high-precision components to maintain consistent material flow rates, which is crucial for maintaining product quality and preventing overloading or underloading of downstream equipment. Secondly, the use of corrosion-resistant materials, such as stainless steel or specialized alloys, protects the system from the chemical properties of lithium oxide, ensuring long-term durability and reliability. Thirdly, the system incorporates advanced filtration and dust control measures to comply with environmental regulations and maintain a safe working environment. Additionally, the modular design of these systems allows for easy integration with existing production lines and scalability to accommodate varying production volumes. These features collectively contribute to enhanced operational efficiency, reduced maintenance costs, and improved overall safety in lithium oxide processing facilities.
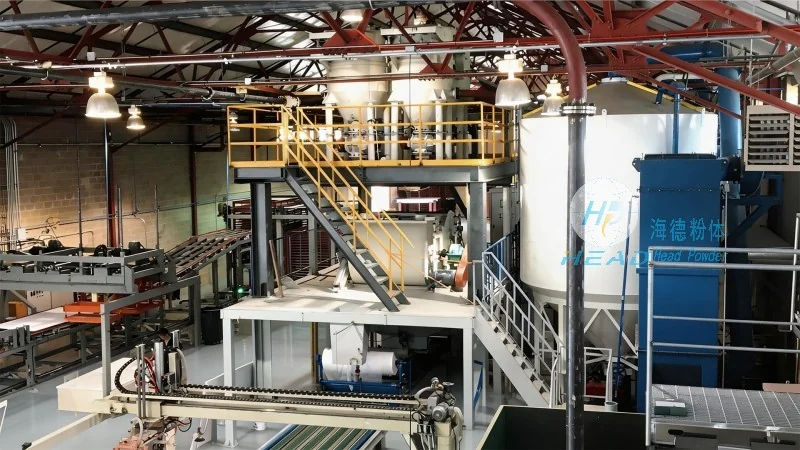
Application-Specific Considerations for Lithium Oxide Handling
When implementing a lithium oxide pneumatic conveying system, several application-specific factors must be considered to optimize performance. The particle size and moisture content of the lithium oxide are critical parameters, as they directly impact the air velocity required for effective transport. For example, finer particles may require higher air speeds to prevent clogging, while higher moisture content can lead to material agglomeration, necessitating additional drying or conditioning steps. The system's layout, including the number and length of pipelines, must be carefully planned to minimize pressure drops and energy consumption. Furthermore, the system should be equipped with safety features, such as pressure relief valves and emergency shut-off mechanisms, to prevent accidents during operation. By addressing these considerations, the system can be tailored to meet the unique demands of lithium oxide processing, ensuring reliable and efficient material handling.
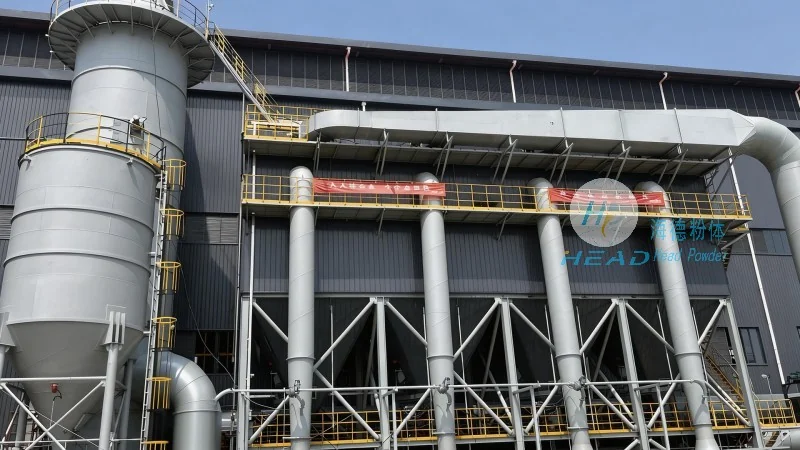
Advantages of Choosing HeadPowder for Lithium Oxide Pneumatic Conveying Solutions
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, offers comprehensive expertise in designing and manufacturing customized lithium oxide pneumatic conveying systems. The company's team of experienced engineers leverages advanced technology and industry best practices to develop solutions that meet the specific needs of clients. By partnering with HeadPowder, businesses can benefit from tailored system designs that enhance productivity, reduce operational costs, and ensure compliance with safety and environmental standards. The company's commitment to quality and customer satisfaction is reflected in its rigorous testing and validation processes, ensuring that each system is optimized for long-term performance and reliability. With a focus on innovation and customer-centric solutions, HeadPowder stands as a trusted partner for lithium oxide material handling in various industrial applications.