

Working Principle and Features of Vacuum Powder Feeding Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced vacuum powder feeding pneumatic conveying systems. These systems are engineered to efficiently handle and transport powders and bulk materials in various industrial applications. The following content will explore the working principle and key features of such equipment, providing a comprehensive understanding of its functionality and benefits.
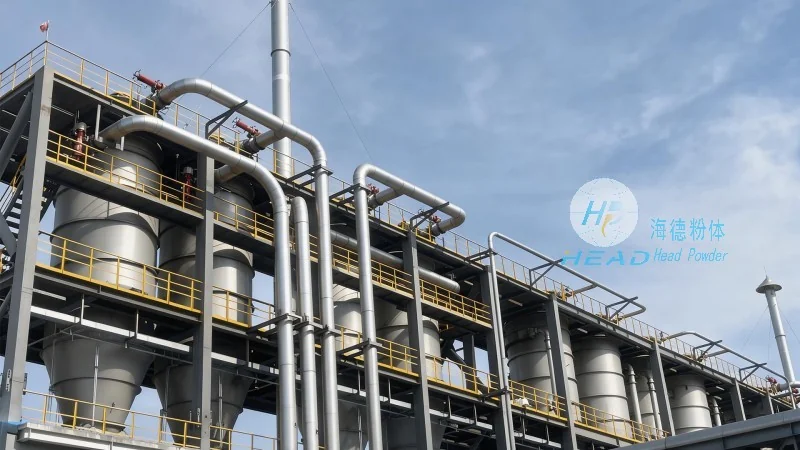
Working Principle of Vacuum Powder Feeding Pneumatic Conveying Equipment
The vacuum powder feeding pneumatic conveying system operates on the principle of creating a negative pressure environment within the conveying line. This is achieved by using a vacuum pump to draw air and the material particles from the source container into the system. The process begins with the material being fed into the hopper or the source vessel. As the vacuum pump runs, it generates a vacuum that pulls the material particles along with the air through the pipeline. The material is then separated from the air at the receiving end, typically through a cyclone separator or a filter, and deposited into the target container. This continuous cycle ensures efficient and reliable material transfer without the need for mechanical components like belts or screws, which are common in traditional conveying methods.
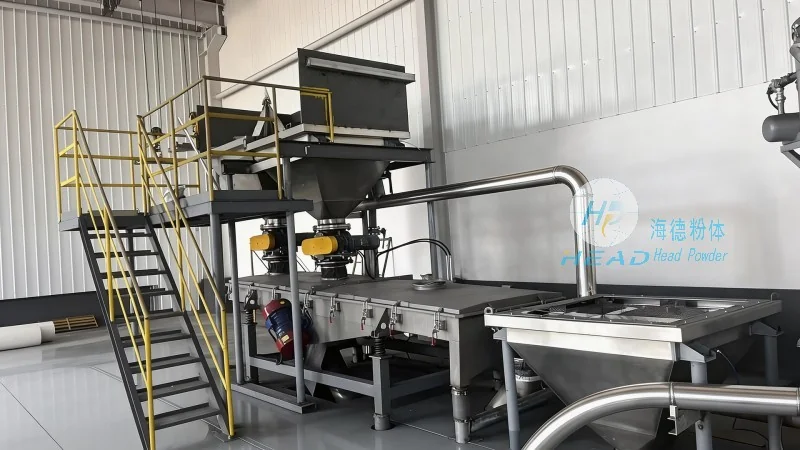
Key Features of Vacuum Powder Feeding Pneumatic Conveying Equipment
HeadPowder's vacuum powder feeding pneumatic conveying equipment is characterized by several distinct features that enhance its performance and applicability in industrial settings. Firstly, the system offers a flexible and versatile design, capable of handling a wide range of powder types, including fine powders, granules, and bulk materials. The adjustable vacuum pressure allows for precise control over the conveying speed and material flow, ensuring consistent and uniform transport. Secondly, the equipment is equipped with advanced filtration and separation systems, such as cyclone separators and bag filters, which effectively prevent material loss and contamination. This is crucial for maintaining product quality, especially in applications where purity is critical, like pharmaceuticals or food processing. Thirdly, the vacuum system is designed for low energy consumption and minimal maintenance, making it an economical and sustainable solution for long-term material handling operations. Additionally, the compact and modular design of the equipment allows for easy installation and integration into existing production lines, reducing downtime and installation costs. The system also features safety mechanisms, including pressure relief valves and overcurrent protection, to ensure safe operation and prevent accidents.
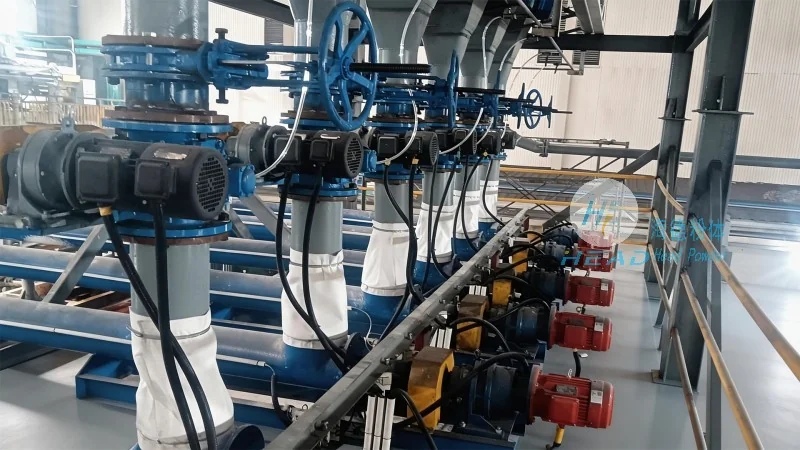
Applications and Benefits in Industrial Settings
Vacuum powder feeding pneumatic conveying equipment from HeadPowder is widely used in various industries, including chemical, pharmaceutical, food processing, and mining. In the chemical industry, it is used to transport raw materials and intermediates, improving process efficiency and reducing handling time. In pharmaceutical applications, the system ensures the hygienic and contamination-free transfer of active ingredients and excipients, meeting stringent regulatory requirements. The food processing industry benefits from the equipment's ability to handle food-grade powders, maintaining product safety and quality. The mining sector utilizes the system for transporting ore and minerals, enhancing productivity and reducing labor costs. The primary benefits of using this equipment include increased productivity through continuous operation, reduced labor costs due to automated material handling, improved product quality through consistent and controlled transport, and enhanced safety by eliminating manual handling of powders. Additionally, the system's low maintenance requirements and energy efficiency contribute to long-term cost savings and environmental sustainability.