

Working Principle and Features of Automatic Bulk Bag Unpacking Material Conveying Lines
Automatic bulk bag unpacking material conveying lines are advanced industrial systems designed to streamline the process of handling bulk materials from large bags, such as super sacks or big bags, into a continuous flow for further processing or storage. These systems are crucial in various industries, including chemical, food, pharmaceutical, and mining, where efficient material handling is essential for operational efficiency and cost reduction.
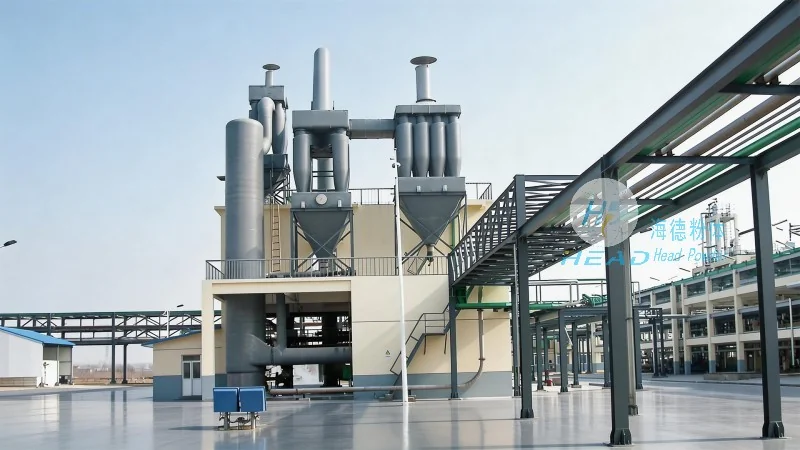
Introduction to the System
The core function of a bulk bag unpacking line is to automate the entire process of opening, emptying, and transferring bulk materials from a flexible container into a conveyor system. This automation eliminates manual labor, reduces the risk of material contamination, and ensures consistent and reliable material flow. The system typically integrates multiple components, including bag openers, discharge chutes, conveyor belts, and material handling equipment, all working in coordination to achieve seamless operation.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in the field of material handling solutions, specializes in designing and manufacturing high-quality automatic bulk bag unpacking and conveying systems. With a strong commitment to innovation and customer satisfaction, HeadPowder has established itself as a trusted partner for businesses seeking efficient and reliable material handling solutions. The company's headquarters is located in Shandong, China, where it leverages advanced technology and rigorous quality control to deliver top-tier products to global markets.
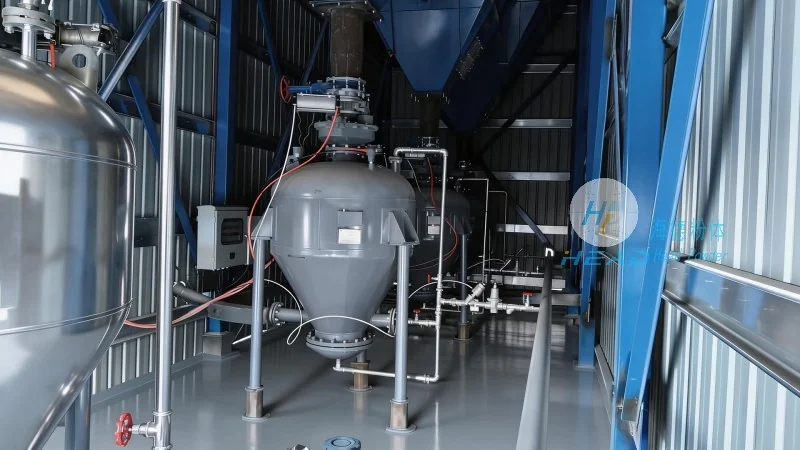
Working Principle of the Automatic Bulk Bag Unpacking Material Conveying Line
The operation of an automatic bulk bag unpacking material conveying line involves several key steps, each designed to ensure efficient material transfer. The process typically begins with the placement of a bulk bag onto a designated loading platform. The system then uses mechanical or pneumatic mechanisms to open the bag, allowing the contents to flow through a discharge chute. The material is then directed onto a conveyor belt, which transports it to the next stage of processing or storage. The entire process is controlled by an automated system, which monitors and adjusts parameters such as flow rate, pressure, and speed to maintain optimal performance.
Key Features and Advantages
Automatic bulk bag unpacking material conveying lines offer numerous advantages that contribute to improved operational efficiency and product quality. Some of the key features include:
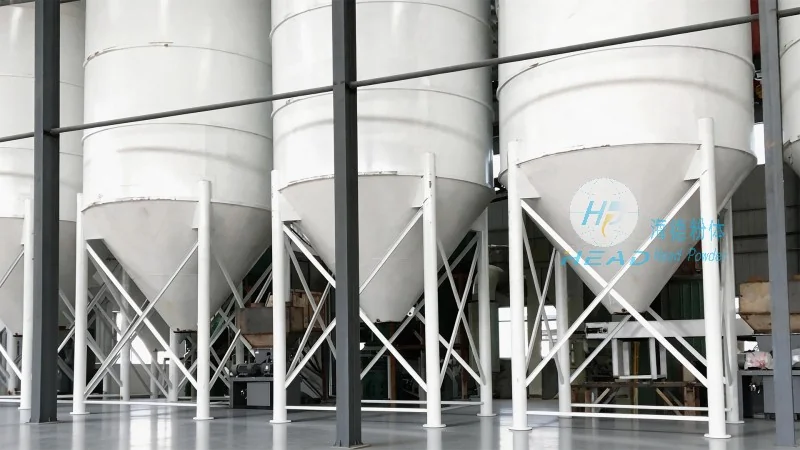
- Automation and Reduced Labor: By automating the bag opening and material transfer process, these systems significantly reduce the need for manual labor, thereby lowering labor costs and minimizing the risk of human error.
- Consistent Material Flow: The integrated design ensures a continuous and uniform flow of materials, which is crucial for maintaining consistent product quality and preventing material segregation.
- Reduced Contamination Risk: The enclosed system design minimizes the exposure of materials to external contaminants, ensuring that the final product meets stringent quality and safety standards.
- Space Efficiency: These systems are designed to be compact and space-efficient, making them suitable for installations in various industrial settings, including factories and warehouses.
- Customization Options: HeadPowder offers customizable solutions tailored to the specific needs of different industries and applications, ensuring that the system meets the unique requirements of each customer.
Applications and Industries
Automatic bulk bag unpacking material conveying lines are widely used in a variety of industries where bulk materials are handled. Some common applications include:
- Chemical Industry: For handling and transferring chemicals, powders, and granules used in manufacturing processes.
- Food and Beverage Industry: For processing and conveying food ingredients, such as flour, sugar, and spices, while maintaining hygiene and safety standards.
- Pharmaceutical Industry: For handling active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring compliance with regulatory requirements.
- Mining and Minerals Industry: For processing and conveying raw materials, such as ores and minerals, from bulk bags to processing equipment.
Conclusion
Automatic bulk bag unpacking material conveying lines are essential equipment for modern industrial operations, offering significant benefits in terms of efficiency, cost reduction, and product quality. With its advanced technology and commitment to customer satisfaction, Shandong HeadPowder Engineering Co., Ltd. provides reliable and effective solutions that meet the diverse needs of various industries. By investing in such systems, businesses can enhance their operational capabilities and stay competitive in today's market.