

Working Principle and Features of Gray Calcium Powder Conveying Equipment
Gray calcium powder conveying equipment is a specialized system engineered for the efficient and safe transportation of gray calcium powder, a widely used industrial material in sectors like construction, manufacturing, and chemical processing. This equipment is vital for maintaining consistent material flow, minimizing dust exposure, and optimizing operational efficiency in industrial settings. The following sections will delve into the working principle and key features of such equipment, offering insights into its design and functionality.
Working Principle of Gray Calcium Powder Conveying Equipment
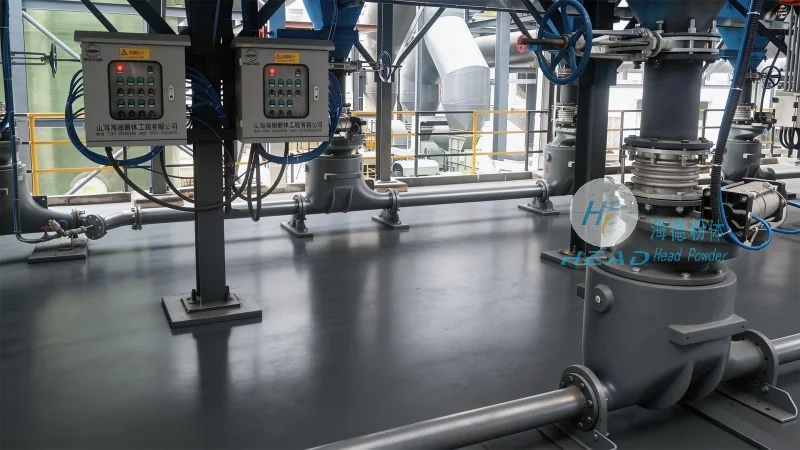
The fundamental working principle of gray calcium powder conveying equipment centers on the mechanical movement of bulk material from a source to a destination. These systems typically integrate components including hoppers for material storage, feeders for controlled discharge, and conveying mechanisms such as screw conveyors, pneumatic systems, or belt conveyors. The process initiates with gray calcium powder being fed into a hopper, where it is regulated before entering the conveying mechanism. The feeder then precisely controls the flow rate of the powder into the conveyor, ensuring a steady and controlled discharge. Depending on the specific design, the conveying mechanism may utilize mechanical force (e.g., rotating screws or belts) or pneumatic pressure (air or gas) to transport the powder through pipelines or open channels. The system is equipped with sensors and control valves to monitor and adjust the flow, preventing blockages or overloading and maintaining optimal performance. This integrated approach ensures efficient and safe transport of gray calcium powder, minimizing material degradation and environmental contamination risks.
Key Features of Gray Calcium Powder Conveying Equipment
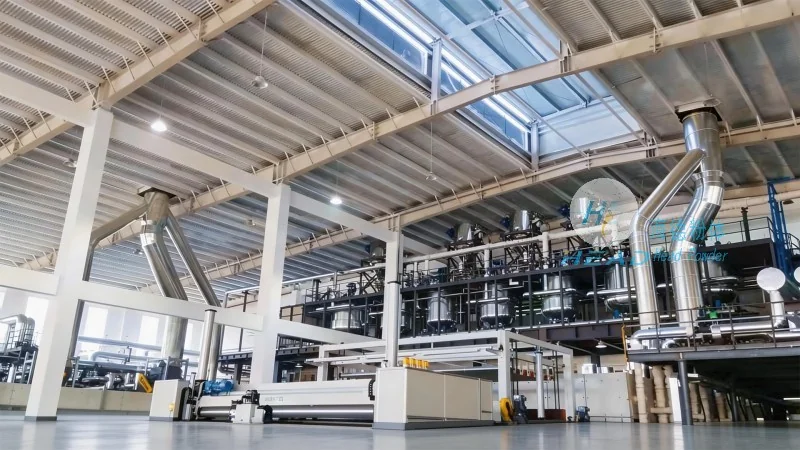
Gray calcium powder conveying equipment is distinguished by several critical features that enhance its performance and usability in industrial applications. A primary feature is its ability to handle fine, dusty materials like gray calcium powder without excessive dust generation or clogging. The equipment often incorporates dust-proof and sealed components, such as enclosed hoppers and conveyor systems, to reduce environmental impact and protect operators from inhalation hazards. Another key feature is adjustable flow control, allowing operators to regulate material transport speed and volume based on production requirements. This flexibility is essential for maintaining consistent product quality and preventing overloading of downstream processing equipment. Additionally, the equipment includes safety features like emergency stop buttons, overload protection, and material detection sensors to ensure safe operation and prevent accidents. The use of corrosion-resistant materials, such as stainless steel or specialized coatings, is common to withstand the chemical properties of gray calcium powder and extend equipment lifespan. These features collectively contribute to the reliability and efficiency of gray calcium powder conveying systems, making them a preferred choice for industries dealing with bulk powder materials.
Applications and Benefits
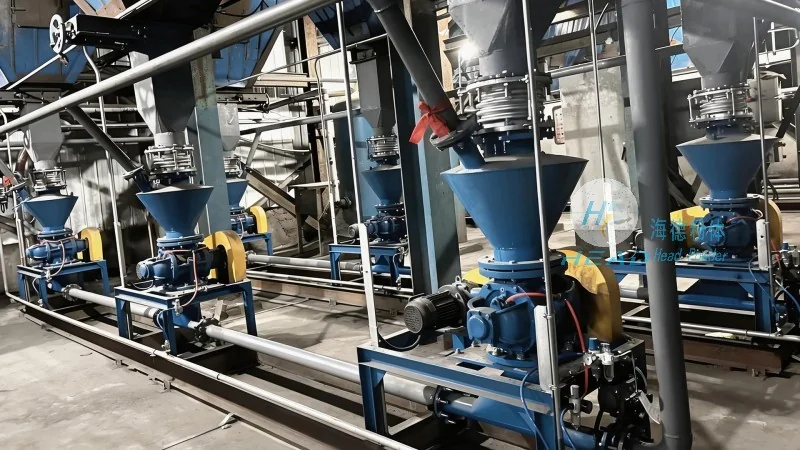
Gray calcium powder conveying equipment is widely utilized across various industrial sectors due to its efficiency in handling fine powders. In the construction industry, it transports gray calcium powder used in cement production and other building materials. In manufacturing, it facilitates the transport of calcium powder in chemical processing plants, where it serves as a raw material for producing diverse products. The equipment also finds applications in food processing and pharmaceutical industries, where safe and hygienic powder handling is critical. The primary benefits of using such equipment include improved operational efficiency, reduced labor costs, and enhanced safety by minimizing manual powder handling. It also helps maintain consistent material quality by preventing segregation and agglomeration during transport, leading to better product consistency and reduced waste. The ability to handle large material volumes at once boosts productivity and reduces downtime, making gray calcium powder conveying equipment a valuable asset for industrial operations.