

Working Principle and Features of Tonne Bag Powder Conveying Systems
Understanding the working principle and key features of tonne bag powder conveying systems is essential for industries that rely on efficient and reliable material handling. These systems are designed to handle bulk powders from large tonne bags, ensuring safe and effective transfer to processing equipment. This article provides an in-depth look at how these systems operate and the advantages they offer.
Overview of Tonne Bag Powder Conveying Systems
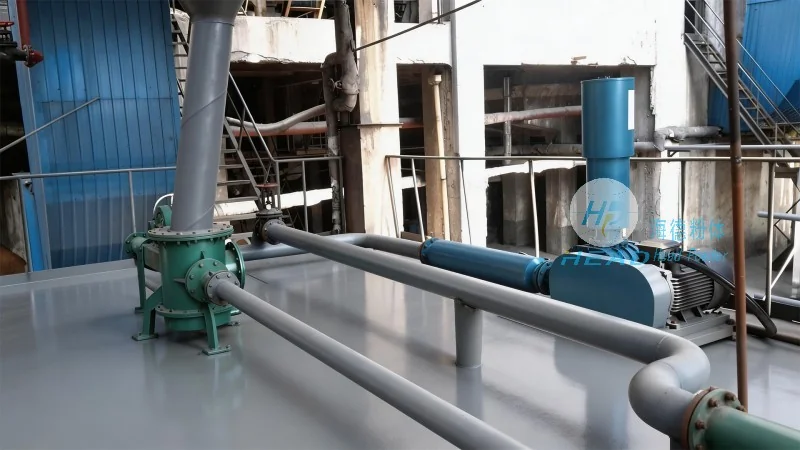
Tonne bag powder conveying systems are specialized equipment used in various industrial sectors, including chemical, food, pharmaceutical, and mining industries. The primary function of these systems is to transfer bulk powders from sealed tonne bags into storage silos, hoppers, or processing machinery. The system typically consists of several components, including a hopper, a feeding mechanism, a conveying device, and a control system. The design is tailored to handle different types of powders, ensuring minimal dust generation and product contamination.
Working Principle of Tonne Bag Powder Conveying Systems
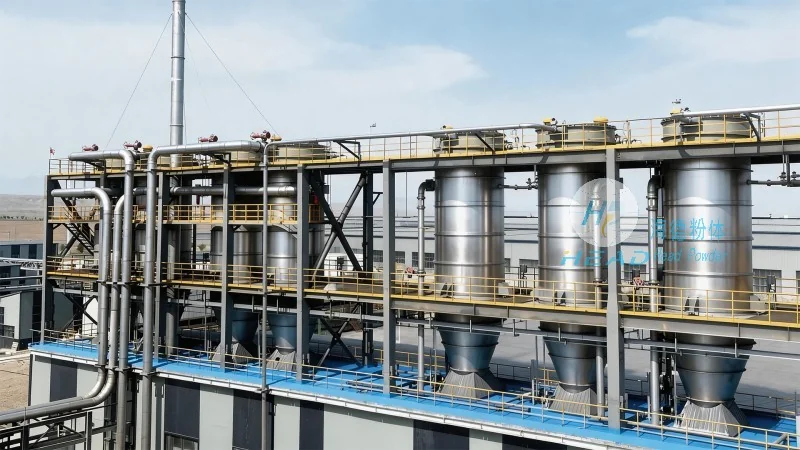
The working principle of a tonne bag powder conveying system involves a series of steps that ensure the safe and efficient transfer of material. The process begins with the placement of a tonne bag onto a support frame or a loading platform. The bag is then opened, and the powder is discharged into a hopper through a valve or a discharge chute. The hopper is equipped with a feeding device, such as a rotary valve or a screw feeder, which regulates the flow of powder into the conveying system. The conveying device, which can be a pneumatic or mechanical system, then transports the powder to the desired destination. The control system monitors the entire process, ensuring that the flow rate, pressure, and other parameters are maintained within optimal ranges. This integrated approach ensures that the material is handled with precision and minimal loss.
Key Features of Tonne Bag Powder Conveying Systems
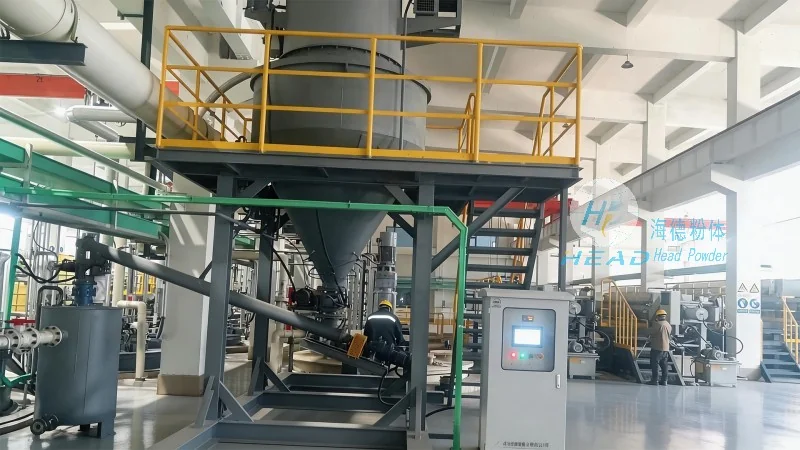
HeadPowder, a leading manufacturer of powder handling equipment, offers tonne bag powder conveying systems with several key features that enhance performance and reliability. One of the primary features is the use of a dust extraction system, which captures and filters airborne particles, reducing environmental impact and ensuring compliance with safety regulations. The systems are also equipped with a level sensor and a pressure sensor, which provide real-time monitoring of the material level and pressure within the hopper and conveying line. This allows for automatic control of the feeding rate, preventing overfilling or underfilling. Another important feature is the ability to handle a wide range of powder characteristics, including different particle sizes, moisture content, and flowability. The systems are designed to minimize product degradation and maintain product integrity throughout the handling process. Additionally, the equipment is constructed from high-quality materials, such as stainless steel, to resist corrosion and ensure long-term durability. The control system is user-friendly, with an intuitive interface that allows operators to monitor and adjust the system parameters easily. This feature enhances operational efficiency and reduces the risk of human error.
Applications and Benefits of Tonne Bag Powder Conveying Systems
Tonne bag powder conveying systems are widely used in various industries due to their versatility and efficiency. In the chemical industry, these systems are used to handle raw materials and intermediates, ensuring a continuous supply of material to production lines. In the food and pharmaceutical industries, the systems are critical for maintaining product quality and safety, as they minimize contamination and ensure consistent material flow. The mining industry also benefits from these systems, as they help in the efficient handling of ore and other bulk materials. The primary benefits of using tonne bag powder conveying systems include increased productivity, reduced labor costs, and improved safety. The systems eliminate the need for manual handling of tonne bags, which can be hazardous and time-consuming. Additionally, the automated control system reduces the risk of material loss and improves the overall efficiency of the production process. The dust extraction system also improves the working environment, reducing the risk of respiratory issues among workers. Overall, tonne bag powder conveying systems offer a cost-effective and reliable solution for bulk powder handling, enhancing the operational performance of industrial facilities.
Conclusion
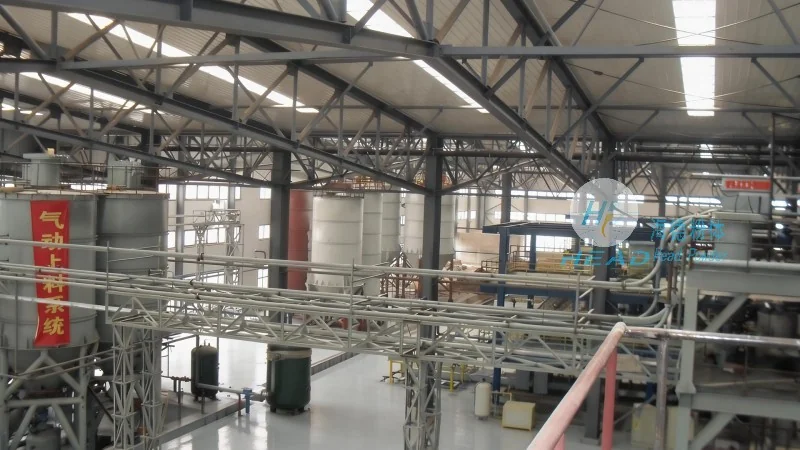
In conclusion, tonne bag powder conveying systems are essential equipment for industries that handle bulk powders. The working principle, which involves a series of integrated components, ensures efficient and safe material transfer. The key features offered by manufacturers like HeadPowder, such as dust extraction, real-time monitoring, and material flexibility, enhance the performance and reliability of the systems. The applications of these systems span across various industries, providing significant benefits in terms of productivity, safety, and cost-effectiveness. As industries continue to seek more efficient and sustainable material handling solutions, tonne bag powder conveying systems remain a critical component in modern industrial operations.