

Working Principle and Features of Cement Raw Material Pneumatic Conveying System Equipment
The cement industry relies heavily on efficient material handling systems to ensure smooth production processes. Among the various technologies available, pneumatic conveying systems for cement raw materials have emerged as a reliable and effective solution. These systems play a crucial role in transporting bulk materials like limestone, clay, and other raw ingredients from storage silos to the production lines with precision and minimal downtime.
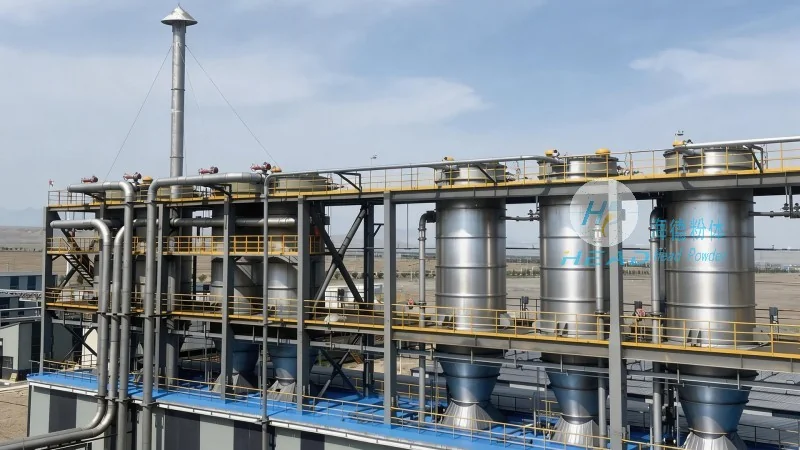
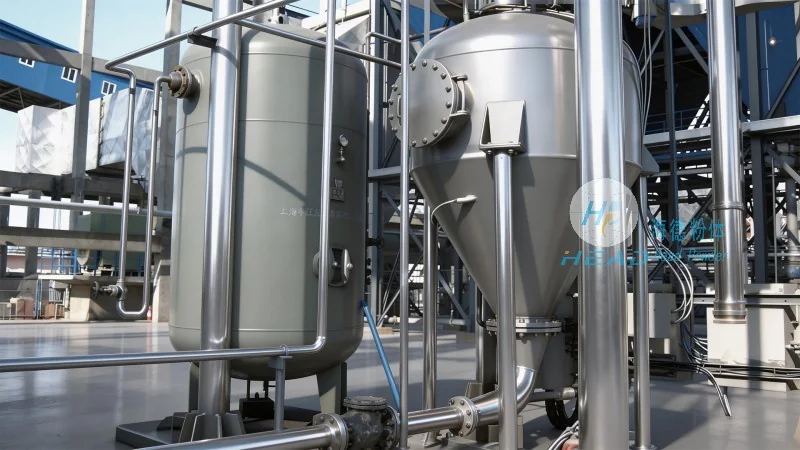
Working Principle of Cement Raw Material Pneumatic Conveying Systems
The working principle of a cement raw material pneumatic conveying system is based on the use of air as the conveying medium. The system typically consists of a hopper, a rotary valve, a conveying line, and a receiver. When the material is discharged from the hopper, it is fed into the conveying line through the rotary valve. Simultaneously, a fan or blower generates a high-pressure airflow within the line. This airflow carries the raw material particles forward, ensuring they are transported to the receiver. The system can operate in either positive or negative pressure modes, depending on the specific requirements of the cement plant. The positive pressure mode is commonly used for short-distance conveying, while the negative pressure mode is preferred for longer distances or when the system needs to be enclosed to prevent dust emissions.
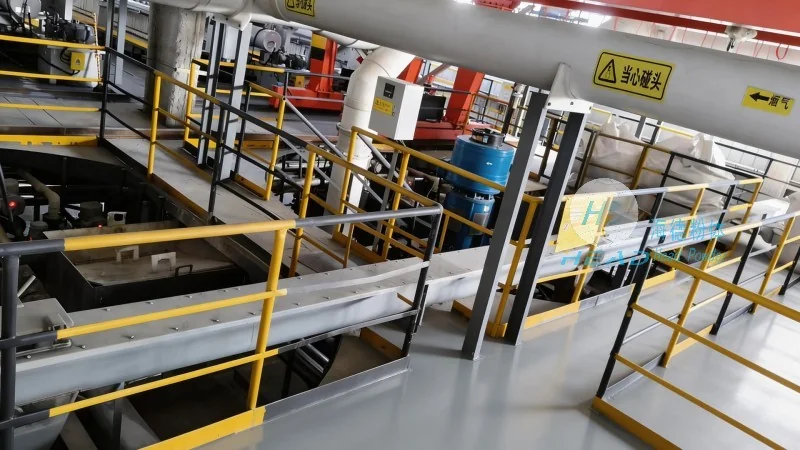
Key Features and Advantages
Key features of the cement raw material pneumatic conveying system include high efficiency in material transport, minimal product degradation due to gentle handling, and the ability to handle a wide range of raw materials with varying particle sizes. The system is also characterized by its compact design, which saves space in the plant layout, and its low maintenance requirements, reducing operational costs. Additionally, the system offers excellent dust control, contributing to a safer working environment and compliance with environmental regulations. Another notable advantage is the system's flexibility, as it can be easily integrated with existing production lines and adjusted to accommodate changes in material flow rates or plant expansions.

About HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer of industrial conveying solutions, specializes in providing customized pneumatic conveying systems tailored to the needs of the cement industry. With a strong presence in Shandong, China, HeadPowder Engineering Co., Ltd. leverages advanced engineering and manufacturing capabilities to deliver high-quality equipment that meets international standards. The company's commitment to innovation and customer satisfaction has made it a trusted partner for cement plants worldwide, ensuring reliable and efficient material handling solutions. HeadPowder's team of experienced engineers and technicians works closely with clients to understand their specific requirements and design systems that optimize performance and reduce downtime. The company's facilities in Shandong are equipped with state-of-the-art technology and adhere to strict quality control measures, ensuring that every product meets the highest standards before delivery.