

Working Principle and Features of Urea Granule Pneumatic Conveying Lines
Urea granule pneumatic conveying lines are essential equipment in the fertilizer and chemical industries, designed to transport urea granules efficiently and safely. These systems utilize air as the conveying medium to move urea granules from one location to another, offering a cost-effective and reliable solution for material handling. The technology behind these lines combines pneumatic transport principles with specialized engineering to ensure optimal performance in various industrial applications.
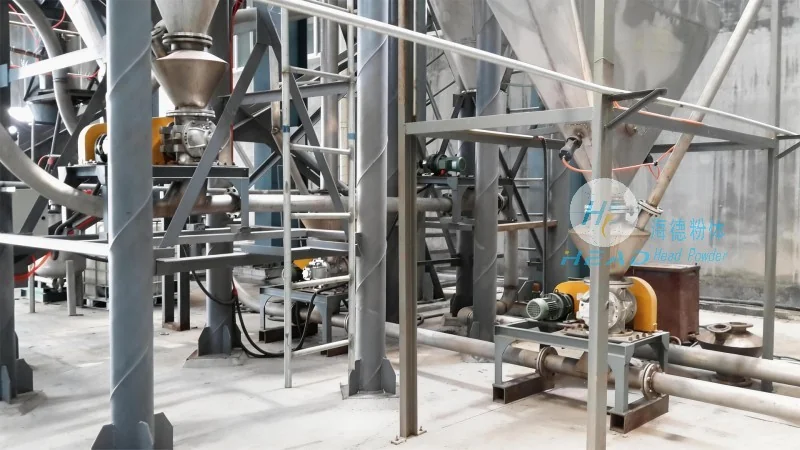
Working Principle of Urea Granule Pneumatic Conveying Lines
The working principle of a urea granule pneumatic conveying line involves several key components and processes. At its core, the system uses a blower or compressor to generate air pressure, which then propels the urea granules through a pipeline. The process typically begins with the urea granules being fed into a hopper or feeder, where they are then introduced into the conveying line. As the air flows through the pipeline, it creates a flow that carries the granules along the path. The velocity and pressure of the air are carefully controlled to ensure that the granules are transported without damage and with minimal loss. The system may include features such as cyclones or filters to separate the granules from the air at the end of the line, allowing for the recovery of the material and the release of clean air.
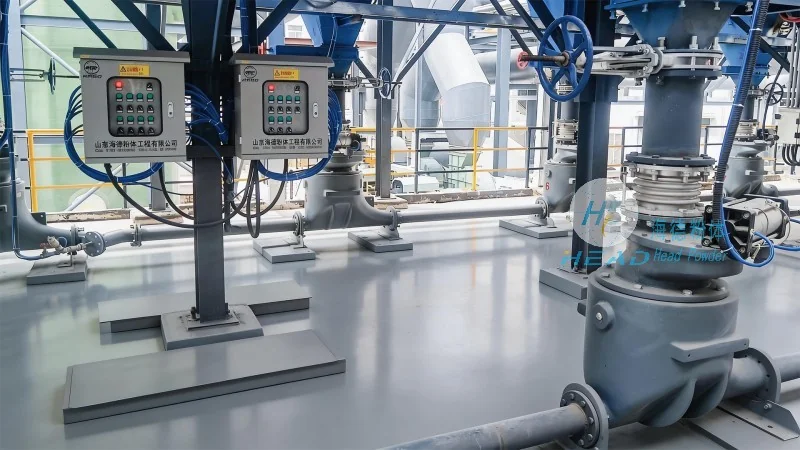
Key Features of Urea Granule Pneumatic Conveying Lines
Urea granule pneumatic conveying lines offer several advantages that make them a preferred choice for industrial material handling. One of the primary features is their ability to handle abrasive materials like urea granules without causing wear and tear on the equipment. The design of the conveying line, including the use of high-quality materials and robust components, ensures long-term durability and low maintenance costs. Another important feature is the system's flexibility, as it can be configured to accommodate different flow rates and distances, making it suitable for various production scales. Additionally, the pneumatic conveying method minimizes the risk of dust contamination and provides a clean and hygienic environment, which is crucial for industries where product purity is essential. The system also offers energy efficiency, as it uses air as the primary conveying medium, reducing the need for mechanical conveyors that may require more power and maintenance.
Applications and Benefits in Industrial Settings
Urea granule pneumatic conveying lines are widely used in the fertilizer manufacturing industry, where they play a critical role in transporting urea granules from storage silos to processing units or packaging facilities. The efficiency of these systems helps to streamline production processes, reduce downtime, and improve overall operational productivity. In addition to fertilizer production, the technology is also applied in other sectors such as chemical processing and agricultural supply chains, where the need to move bulk materials quickly and reliably is paramount. The benefits of using pneumatic conveying systems include reduced labor costs, improved safety by eliminating manual handling of heavy or dusty materials, and enhanced product quality through minimized contamination and damage during transport.
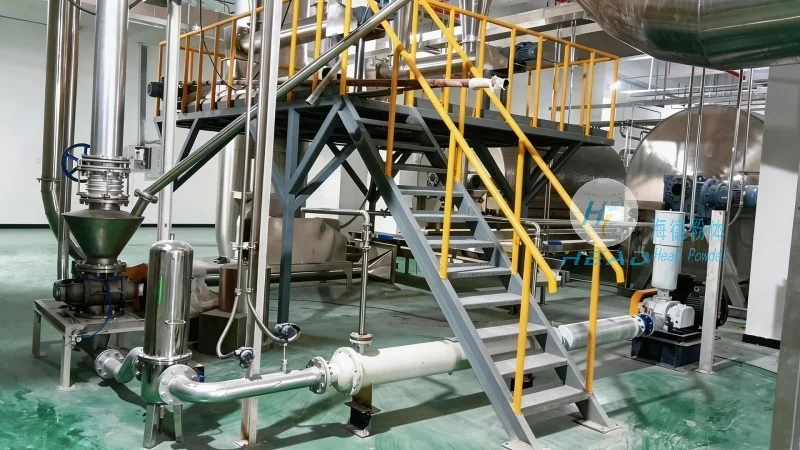
Engineering and Manufacturing by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the field, specializes in the design, development, and production of urea granule pneumatic conveying lines. With a strong focus on quality and innovation, the company utilizes advanced engineering techniques to ensure that its products meet the highest industry standards. The company's facilities are located in Shandong, China, where it leverages local expertise and resources to deliver reliable and efficient solutions to clients worldwide. By combining years of experience in material handling and pneumatic transport technology, HeadPowder Engineering provides customized solutions tailored to the specific needs of each client, ensuring optimal performance and long-term value. The company's commitment to customer satisfaction and technical excellence has established it as a trusted partner in the industry, offering comprehensive support from initial consultation to installation and maintenance of the conveying lines.