

Working Principle and Features of Dry Flue Gas Desulfurization Ash Pneumatic Conveying Equipment
Pneumatic conveying systems play a crucial role in the efficient handling and transportation of dry flue gas desulfurization (FGD) ash. This equipment is essential for industrial facilities that employ wet or dry flue gas desulfurization processes to reduce sulfur dioxide emissions. The FGD ash, also known as gypsum or calcium sulfate, must be transported from the desulfurization unit to storage or disposal sites. Traditional methods like belt conveyors or trucks can be inefficient, costly, and environmentally unfriendly due to dust generation and material degradation. Pneumatic conveying offers a more effective solution by utilizing air to move the ash through pipelines, ensuring a clean, dust-free operation and reducing operational costs.
Working Principle of the Equipment
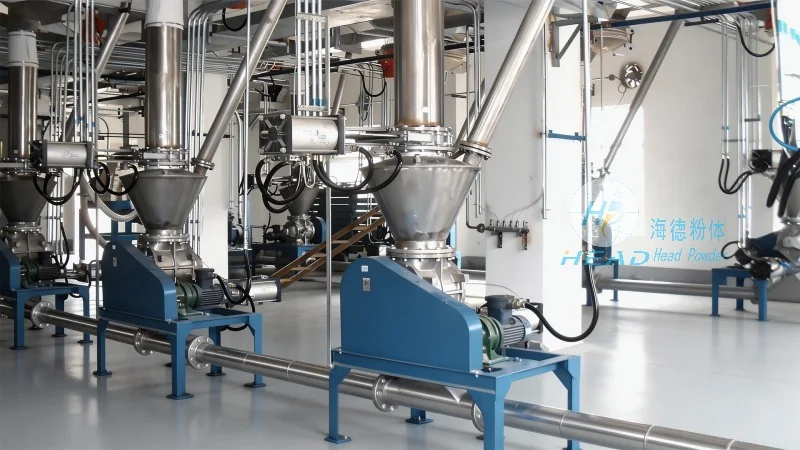
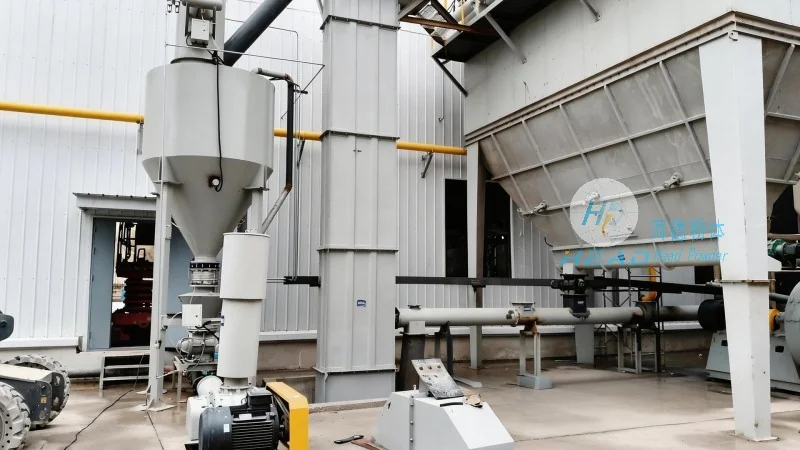
The dry flue gas desulfurization ash pneumatic conveying equipment operates on the principle of air-driven transport. The system typically consists of a dust collector, a conveying pipeline, a blower or air compressor, and a discharge unit. The process begins with the ash being fed into the dust collector, where it is separated from any residual moisture or impurities. The ash then falls into a hopper connected to the conveying pipeline. The blower generates a high-velocity airflow that propels the ash particles through the pipeline. The air velocity is carefully controlled to ensure the ash is fully suspended and transported without clogging the system. The discharge unit at the end of the pipeline collects the ash and deposits it into a storage container or transport vehicle. This continuous process allows for a seamless and automated handling of FGD ash, minimizing manual intervention and enhancing operational efficiency.
Key Features of the Equipment
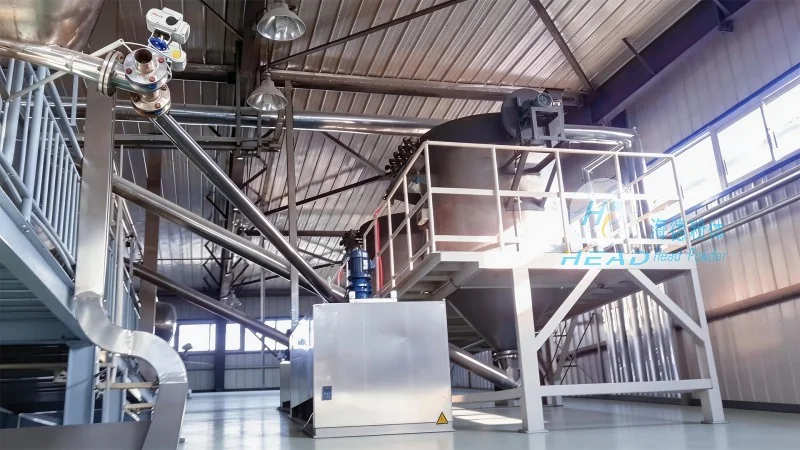
Several key features make the dry flue gas desulfurization ash pneumatic conveying equipment an ideal choice for industrial applications. Firstly, it offers a dust-free operation, which is critical for maintaining a safe and healthy working environment. The enclosed pipeline system prevents ash from escaping into the atmosphere, reducing the risk of respiratory issues and environmental contamination. Secondly, the equipment is highly efficient in terms of energy consumption. By using a blower to generate the necessary airflow, the system minimizes energy waste compared to traditional mechanical conveyors. Thirdly, it provides flexibility in terms of layout and installation. The pipeline can be arranged in various configurations, including vertical, horizontal, or a combination of both, to suit the specific requirements of the facility. Additionally, the system is easy to maintain and repair, with accessible components that can be serviced without extensive downtime. Another important feature is its ability to handle a wide range of ash types and particle sizes, ensuring compatibility with different FGD processes. The equipment also offers scalability, allowing it to be expanded or modified as the facility's needs grow.
About HeadPowder: Your Trusted Partner for Pneumatic Conveying Solutions
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of pneumatic conveying equipment in China. With a strong focus on innovation and quality, the company has established itself as a reliable partner for industrial facilities worldwide. HeadPowder specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of clients. The company's team of experienced engineers and technicians ensures that each project is handled with precision and attention to detail. HeadPowder's products are known for their durability, efficiency, and compliance with international standards. The company's headquarters is located in Shandong, China, providing a strategic base for serving both domestic and international markets. By choosing HeadPowder, clients can expect high-quality equipment that meets their operational requirements while adhering to environmental regulations. The company's commitment to customer satisfaction and technological advancement has made it a preferred choice for industries relying on efficient FGD ash handling solutions.