

What is a White Sugar Powder Conveying System Equipment? Exploring Its Design Principles
White sugar, a fundamental ingredient in the food and beverage industry, demands efficient and reliable handling from production to distribution. The white sugar powder conveying system equipment is crucial for ensuring the smooth and safe transport of this fine powder. This article explores the specifics of such equipment, delving into its design principles and the key factors that contribute to its effectiveness.
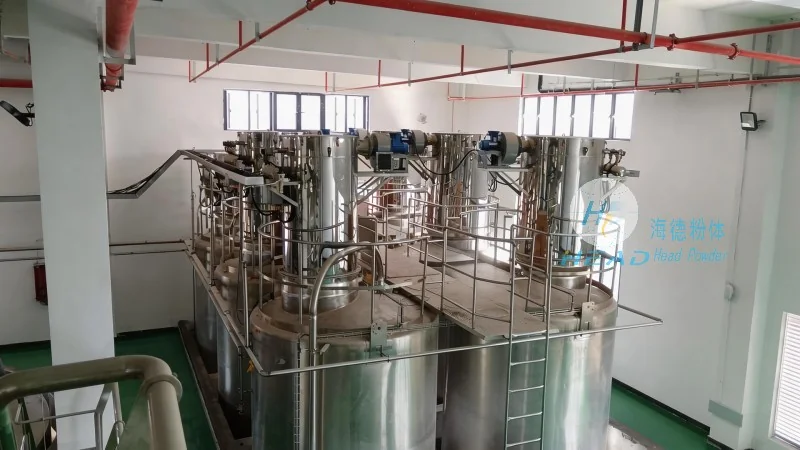
Introduction to White Sugar Powder Conveying Systems
The white sugar powder conveying system equipment is engineered to address the unique properties of white sugar, including its fine particle size, hygroscopic nature, and tendency to form lumps or agglomerates. Traditional conveying methods often fail to handle these characteristics effectively, leading to blockages, product degradation, or contamination. Specialized equipment designed for white sugar ensures the powder is transported without compromising its quality or integrity.
Key Components of the Conveying System
The white sugar powder conveying system typically integrates several components that work in concert to achieve efficient transport. These components include feed hoppers, conveyor belts or screw conveyors, airlock valves, and dust collection systems. Each part is carefully selected and designed to mitigate the specific challenges associated with white sugar powder, such as material buildup and product loss.
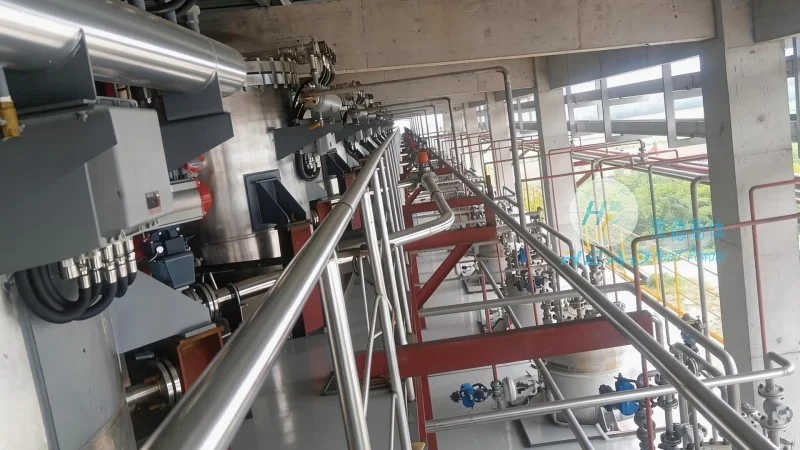
Design Principles for Efficient White Sugar Conveying
The design of a white sugar powder conveying system is guided by principles focused on maximizing efficiency, minimizing product loss, and ensuring safety. A primary consideration is the prevention of material buildup and blockages, achieved through smooth, non-stick surfaces and gentle handling mechanisms that prevent sugar adhesion. Additionally, the system incorporates features that maintain hygienic standards required in food processing, including easy-to-clean surfaces and sealed components.
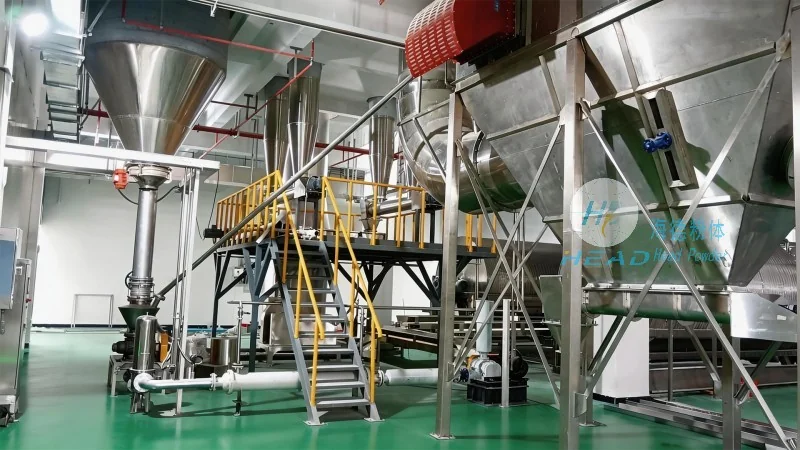
How the System Preserves Product Integrity
Preserving white sugar's quality is paramount, and the conveying system is designed with this in mind. The equipment minimizes exposure to air and moisture, which can cause clumping or moisture absorption. Positive pressure systems and sealed conveying lines help maintain sugar purity and prevent cross-contamination. Monitoring and control features allow operators to adjust conveying speed and pressure, ensuring optimal performance.
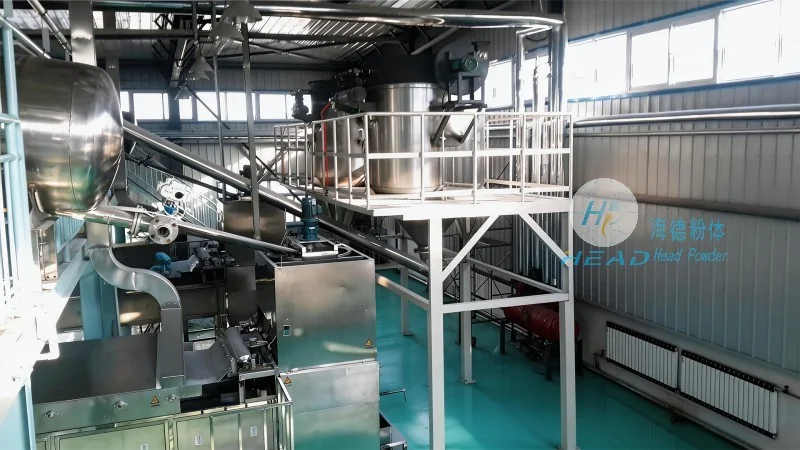
About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer in powder handling equipment, specializes in developing customized solutions for industries requiring precise and reliable powder transport. With a focus on innovation and quality, the company has established itself as a trusted partner for businesses in the food, pharmaceutical, and chemical sectors. HeadPowder's expertise lies in understanding unique powder properties and designing systems tailored to client needs.
Conclusion
In summary, the white sugar powder conveying system equipment is a sophisticated piece of machinery that combines advanced engineering with practical design to address the challenges of handling fine, hygroscopic powders. By understanding key components and design principles, users can appreciate how these systems contribute to efficient and safe transport of white sugar. For those seeking such equipment, companies like Shandong HeadPowder Engineering Co., Ltd. offer tailored solutions ensuring optimal performance and product integrity.