

What is a Dilute Phase Powder Conveyor? And What Are Its Design Principles?
A dilute phase powder conveyor is a specialized industrial equipment designed for the efficient transport of bulk powders over long distances. Unlike dense phase systems, which operate with higher solid concentrations, dilute phase conveyors rely on air or gas to suspend the powder particles, enabling them to move through pipelines with minimal pressure drop and energy consumption. This technology is widely used in various industries, including chemical, pharmaceutical, food processing, and mining, where the safe and reliable transfer of powders is critical.
Key Design Principles of Dilute Phase Powder Conveyors
The design of a dilute phase powder conveyor is governed by several fundamental principles that ensure optimal performance and efficiency. The primary principle is the creation of a pneumatic suspension, where the powder is entrained in a high-velocity air stream. This suspension allows the particles to be carried through the pipeline, reducing friction and preventing clogging. The velocity of the air stream is a critical parameter, as it must be sufficient to keep the powder particles suspended but not so high as to cause excessive energy consumption or particle degradation.
Another key design principle is the selection of appropriate components, such as the air compressor, pipeline diameter, and material of construction. The air compressor must be capable of generating the required pressure and flow rate to maintain the suspension. The pipeline diameter is determined by the flow rate and particle size, ensuring that the air velocity remains within the optimal range for suspension. The material of construction is chosen based on the type of powder being conveyed, with considerations for corrosion resistance, wear resistance, and compatibility with the powder's properties.
Components and Working Mechanism
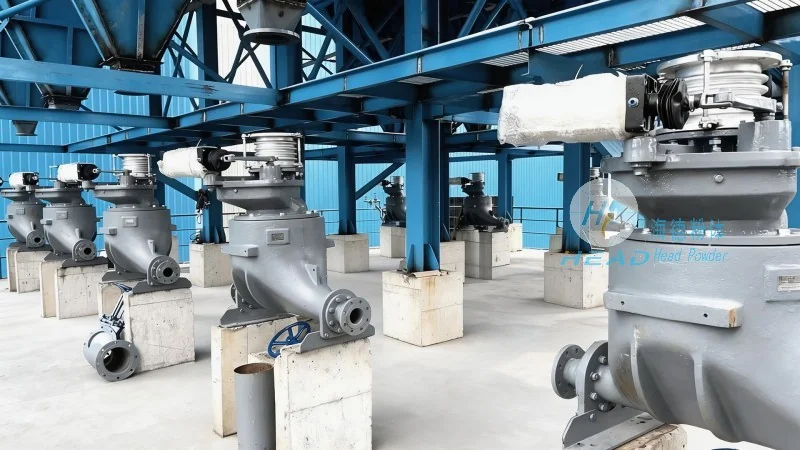
A typical dilute phase powder conveyor system consists of several key components, including a material feeder, air compressor, pipeline, and discharge device. The material feeder is responsible for introducing the powder into the system at a controlled rate. It may be a rotary valve, screw feeder, or other type of feeder that can handle the specific characteristics of the powder, such as moisture content, particle size distribution, and flowability. The air compressor provides the necessary air pressure and flow to entrain the powder particles and transport them through the pipeline.
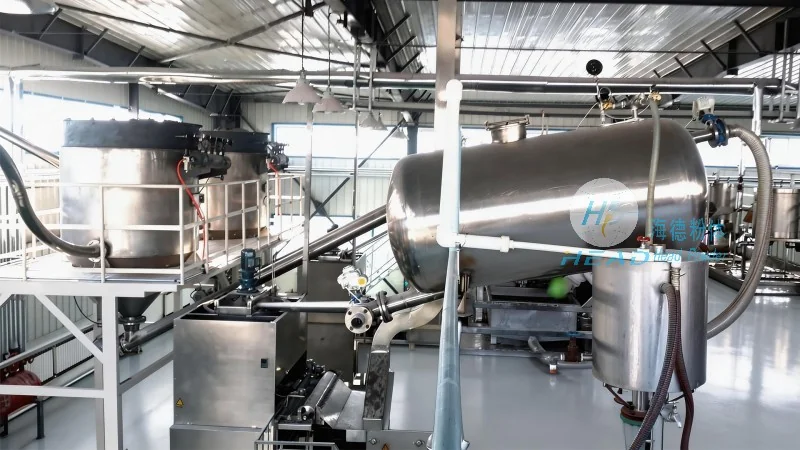
The pipeline is the main component of the conveyor, and its design is critical to the system's performance. The pipeline is typically made of stainless steel or other corrosion-resistant materials, depending on the powder's properties. The diameter of the pipeline is selected based on the required flow rate and the air velocity needed to maintain suspension. The pipeline may include bends, elbows, and other fittings, which are designed to minimize pressure loss and prevent particle deposition.
The discharge device is responsible for releasing the powder from the pipeline at the destination point. It may be a rotary valve, cyclone separator, or other type of device that can handle the powder's characteristics and ensure a smooth discharge. The discharge device is typically located at the end of the pipeline and is designed to prevent backflow and maintain the integrity of the powder.
Advantages of Dilute Phase Powder Conveyors
Dilute phase powder conveyors offer several advantages over other powder handling systems. One of the main advantages is their ability to transport powders over long distances with minimal energy consumption. The use of air as the conveying medium reduces the need for mechanical components, such as belts or buckets, which can be prone to wear and maintenance. Additionally, dilute phase systems can handle a wide range of powder types, including fine powders, which are difficult to transport using other methods.
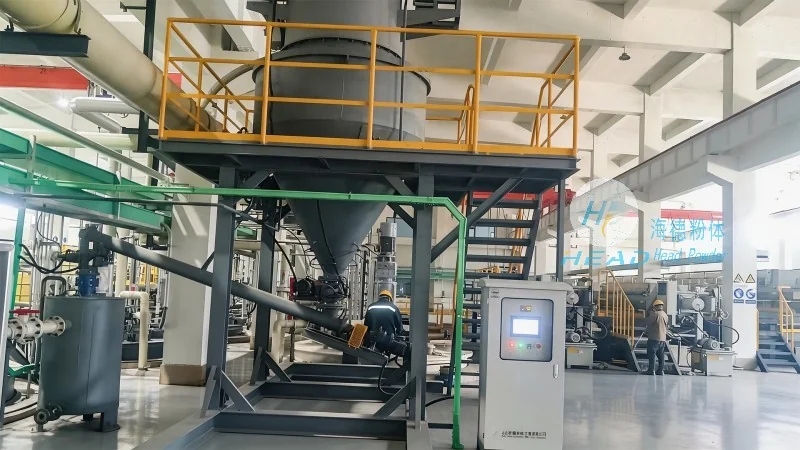
Another advantage is the ability to maintain the quality of the powder during transport. The pneumatic suspension prevents the powder from settling or caking, which can affect its properties and performance. This is particularly important for powders used in pharmaceutical and food industries, where purity and consistency are critical. The system also allows for easy integration with other processing equipment, such as mixers or reactors, enabling a seamless flow of materials.
Applications and Industries
Dilute phase powder conveyors are used in a variety of industries and applications. In the chemical industry, they are used to transport raw materials and finished products, such as powders used in the production of plastics, fertilizers, and pharmaceuticals. In the pharmaceutical industry, they are used to transport active ingredients and excipients, ensuring that the powders are handled in a sterile and controlled environment. In the food processing industry, they are used to transport ingredients such as flour, sugar, and spices, maintaining the quality and freshness of the products.
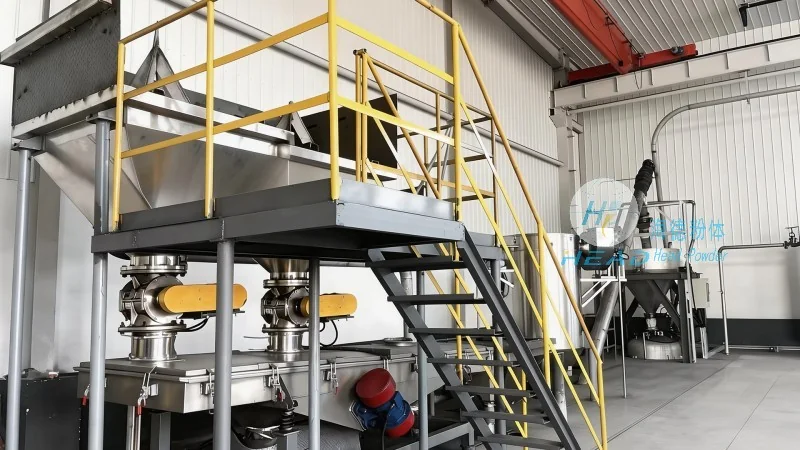
In the mining industry, dilute phase conveyors are used to transport ore and other minerals from the mine to processing facilities. The system allows for the efficient and safe transport of large quantities of material over long distances, reducing the need for trucks and other transportation methods. In the agricultural industry, they are used to transport fertilizers and other agricultural products, ensuring that the materials are delivered to the fields in a timely and efficient manner.
Conclusion
Dilute phase powder conveyors are an essential component of modern industrial operations, providing an efficient and reliable method for transporting bulk powders. The design principles and components of these systems are carefully engineered to ensure optimal performance, energy efficiency, and product quality. As the demand for bulk powder handling continues to grow, dilute phase conveyors will remain a critical technology in various industries, enabling the safe and effective transfer of materials.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of powder handling equipment, specializes in the design and production of dilute phase powder conveyors. With years of experience and expertise in the field, the company provides high-quality, reliable equipment that meets the specific needs of its customers. HeadPowder's dilute phase conveyors are designed to handle a wide range of powder types and applications, ensuring that customers receive the best possible solution for their powder handling needs. The company's commitment to quality and customer satisfaction has made it a trusted partner in the industry, providing reliable and efficient solutions for powder transport and processing.