

Negative Pressure Dilute Phase Powder Conveying System: What It Is and Its Design Principles
A negative pressure dilute phase powder conveying system is a specialized industrial solution designed to transport bulk powders through a pipeline under reduced pressure conditions. This technology is widely used in various industries, including chemical, pharmaceutical, food processing, and mining, where efficient and reliable powder handling is critical. The system operates by creating a vacuum or negative pressure within the pipeline, which draws the powder particles into the air stream and transports them to the destination. This method is particularly effective for handling fine or abrasive powders, as it minimizes particle degradation and ensures consistent flow rates.
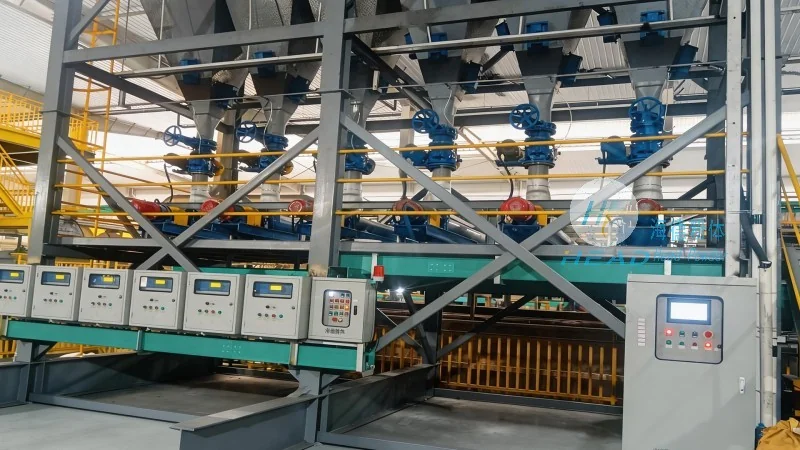
About HeadPowder: A Leading Provider of Powder Handling Solutions
HeadPowder, an abbreviation for Shandong HeadPowder Engineering Co., Ltd., is a professional manufacturer and supplier of advanced powder conveying equipment. With its headquarters located in Shandong, China, the company has established itself as a trusted partner in the powder handling industry, offering customized solutions tailored to meet the specific needs of clients. HeadPowder's expertise lies in the design, development, and installation of high-quality negative pressure dilute phase systems, ensuring optimal performance and durability in demanding industrial environments.
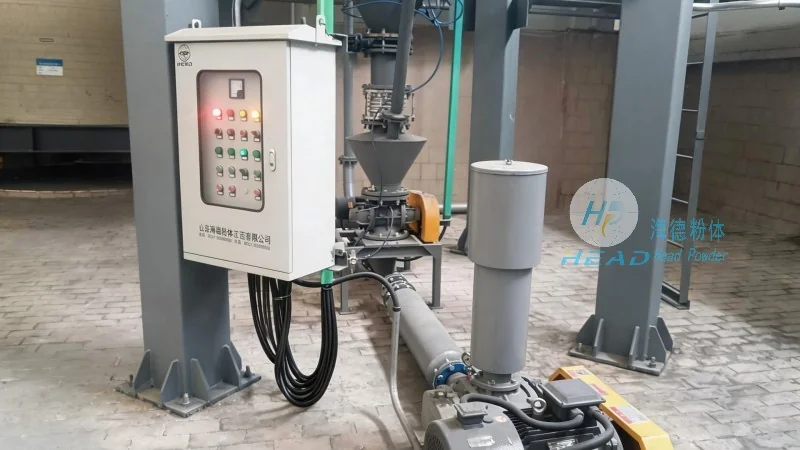
Design Principles of Negative Pressure Dilute Phase Powder Conveying Systems
The design of a negative pressure dilute phase powder conveying system involves several key principles that ensure efficient and safe operation. First, the system must maintain a consistent negative pressure throughout the pipeline to draw the powder particles into the air stream. This is achieved through the use of vacuum pumps or other pressure-reducing devices. Second, the air velocity within the pipeline must be sufficient to keep the powder particles in suspension, preventing settling or blockages. The air velocity is typically maintained at a level that is higher than the terminal velocity of the powder particles, ensuring stable transport. Third, the system incorporates appropriate filtration and separation equipment to remove any entrained air or fine particles from the conveyed material, maintaining product purity and system efficiency. Additionally, the design considers factors such as pipeline length, elevation changes, and the physical properties of the powder being conveyed, to optimize the system's performance and energy consumption.
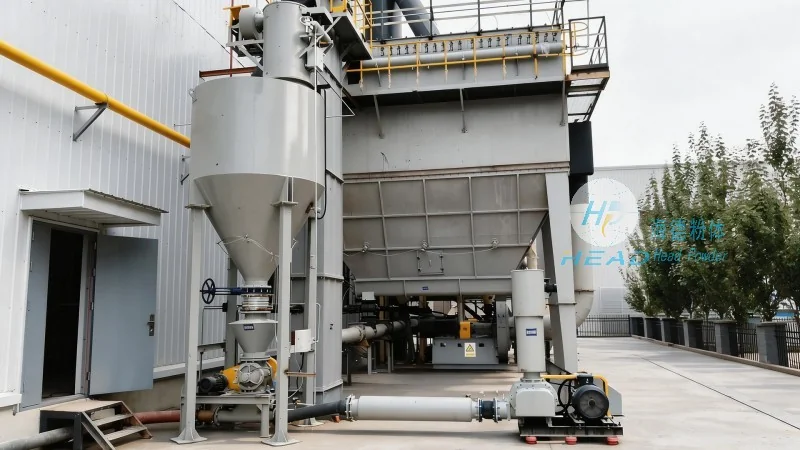
Key Components and Their Functions in the System
Several critical components are integral to the operation of a negative pressure dilute phase powder conveying system. The primary components include the pipeline network, vacuum pumps, feeders, and filtration units. The pipeline is typically made of materials such as stainless steel or PVC, chosen for their resistance to corrosion and wear from the powder particles. Vacuum pumps are responsible for creating the negative pressure within the system, with options including rotary vane pumps, liquid ring pumps, or Roots blowers, depending on the system's requirements. Feeders, such as rotary valves or screw feeders, introduce the powder into the pipeline at a controlled rate, ensuring a consistent flow. Filtration units, including cyclones or bag filters, are used to separate the powder from the air stream, preventing dust emissions and maintaining product quality. Each component is carefully selected and integrated to ensure the system operates efficiently and reliably.
Advantages of Negative Pressure Dilute Phase Powder Conveying Systems
Compared to other powder conveying methods, negative pressure dilute phase systems offer several advantages. One of the primary benefits is the ability to handle fine or abrasive powders without causing particle degradation or equipment wear. The low pressure and high air velocity minimize the impact of particles on the pipeline and components, extending their service life. Another advantage is the system's flexibility, as it can be easily adapted to different powder types and processing requirements. The negative pressure operation also reduces the risk of dust emissions, making it suitable for applications where environmental compliance is a priority. Additionally, the system's energy efficiency is improved through optimized air velocity and pressure control, leading to lower operational costs over time.
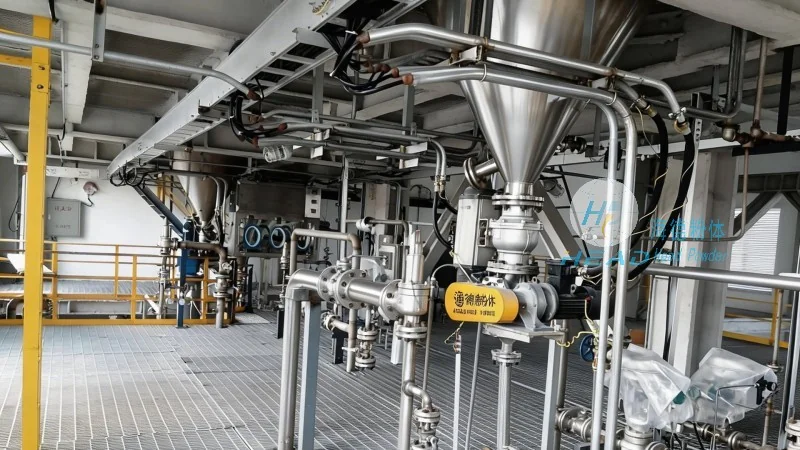
Applications and Industries Using Negative Pressure Dilute Phase Systems
Negative pressure dilute phase powder conveying systems are used in a wide range of industries due to their versatility and effectiveness. In the chemical industry, they are used to transport raw materials and finished products, such as powders used in pharmaceuticals or specialty chemicals. The pharmaceutical industry benefits from the system's ability to handle sterile or sensitive powders, ensuring product purity and compliance with regulatory standards. In the food processing industry, the system is used to convey ingredients like flour, sugar, or spices, maintaining product quality and preventing contamination. The mining industry also utilizes these systems to transport ore powders from processing facilities to storage or further processing. Other applications include the handling of cement, coal, and other bulk materials in construction and energy sectors. The adaptability of the system makes it suitable for various industrial processes, providing reliable powder transport solutions.