

The Role of Pneumatic Conveying in Micropowder Handling
For industries dealing with fine powders, efficient material handling is crucial. Pneumatic conveying systems offer a reliable solution to transport micropowders with precision and minimal loss. This article explores the role of pneumatic conveying in micropowder handling, highlighting its benefits and applications in various industrial settings.
Understanding Micropowder Handling Challenges
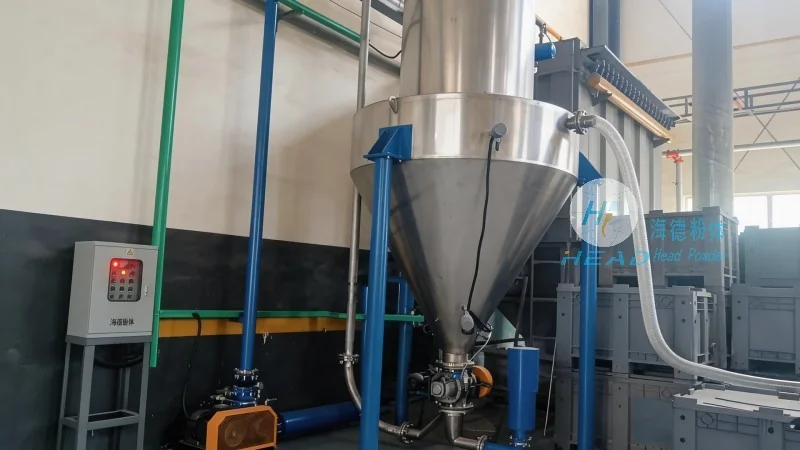
Micropowders, typically defined as particles with a diameter less than 500 micrometers, pose unique challenges during transportation. Their small size leads to high surface area, which can cause issues such as agglomeration, caking, and increased friction. Traditional bulk handling methods like gravity or mechanical conveyors may result in uneven flow, leading to blockages and material loss. Additionally, micropowders are often sensitive to moisture and temperature changes, making it essential to maintain stable conditions during transfer. Pneumatic conveying addresses these challenges by providing a controlled environment where air flow and pressure are precisely regulated to ensure smooth and consistent movement of the powder.

How Pneumatic Conveying Works
Pneumatic conveying systems operate by creating a pressure differential to move powders. There are two main types: dilute-phase and dense-phase systems. Dilute-phase systems use low air velocity to transport powders over long distances, while dense-phase systems use higher air velocity and lower flow rates to achieve more controlled and gentle handling, ideal for sensitive micropowders.
Key Benefits of Pneumatic Conveying for Micropowders
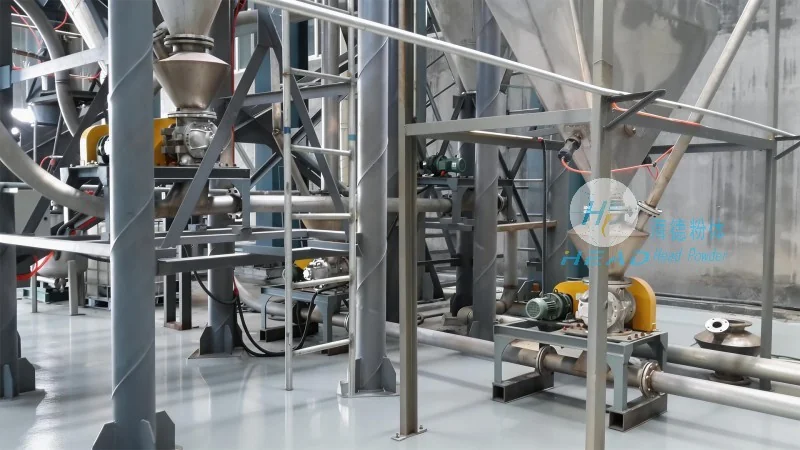
Implementing pneumatic conveying for micropowder handling offers several key benefits that enhance operational efficiency and product quality. Firstly, the enclosed system minimizes product contamination and degradation, which is critical for applications in pharmaceuticals, food, and specialty chemicals. Unlike open systems, pneumatic conveying prevents exposure to external contaminants and reduces the risk of cross-contamination between different batches. Secondly, it significantly reduces dust emissions and improves workplace safety. By containing the powder within a sealed pipeline, it eliminates the need for dust collection systems and reduces the risk of respiratory hazards for operators. Thirdly, pneumatic conveying allows for flexible and scalable solutions. The system can be easily adjusted to accommodate varying production volumes, from small-scale laboratory applications to large-scale industrial production. This adaptability makes it suitable for both batch and continuous processing. Finally, it offers energy efficiency compared to some traditional methods, as the air flow can be optimized to minimize energy consumption while maintaining optimal conveying performance.
Applications in Different Industries
The versatility of pneumatic conveying makes it a preferred choice for various industries dealing with micropowders. In the pharmaceutical sector, it is widely used to handle active pharmaceutical ingredients (APIs) and excipients, ensuring that the final product meets strict purity and quality standards. The enclosed system prevents contamination from environmental factors, which is essential for drug manufacturing. In the food industry, it handles fine powders like sugar, flour, and spices with precision, maintaining the product's flavor and texture. The gentle handling of pneumatic conveying prevents damage to delicate particles, preserving the quality of the final product. In the chemical industry, it transports specialty chemicals and pigments, such as titanium dioxide and carbon black, without compromising their color and chemical properties. The controlled environment ensures that the pigments remain evenly distributed and free from clumping. Additionally, it is used in the ceramics and metal powders sectors for consistent particle size distribution, which is critical for achieving uniform product quality. The ability to adjust air velocity and pressure allows for precise control over the powder's movement, ensuring that the final product meets the required specifications.
Customized Solutions by Shandong HeadPowder Engineering Co., Ltd.
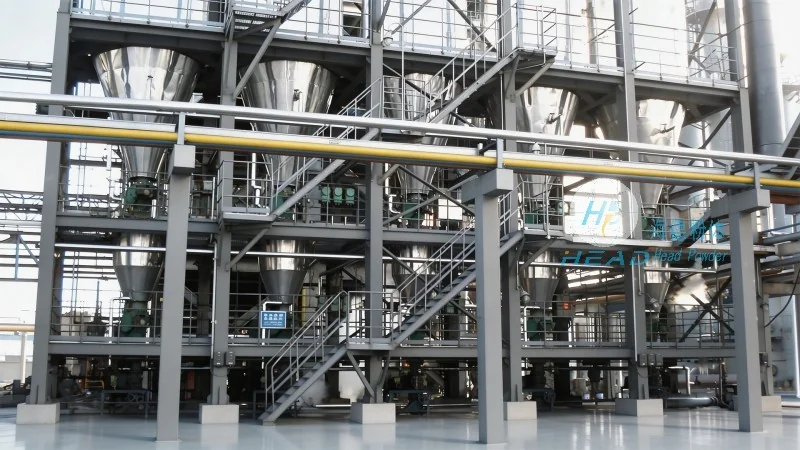
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of pneumatic conveying systems, specializes in providing customized solutions for micropowder handling. With over [years] of industry experience, the company has developed expertise in both dilute-phase and dense-phase technologies, enabling them to design systems that meet the unique needs of each client. Their team of engineers works closely with clients to understand their specific requirements, including particle size, flow rate, and material properties, to develop tailored solutions. The company's systems are engineered to handle a wide range of micropowders, from fine pharmaceutical powders to coarse metal powders, ensuring optimal performance in diverse applications. Shandong HeadPowder Engineering Co., Ltd. also offers after-sales support and maintenance services to ensure the long-term reliability and efficiency of their systems. This commitment to customer satisfaction and technical excellence has made them a trusted partner for industries worldwide.