

Types and Characteristics of Sodium Bicarbonate Pneumatic Conveying Systems
Understanding the various types, key features, and practical applications of sodium bicarbonate pneumatic conveying systems is essential for industries that rely on efficient material handling. This article explores the distinct characteristics of different pneumatic conveying methods, highlighting how they can be applied to the transport of sodium bicarbonate, a widely used chemical compound. The information provided here is tailored to assist professionals in selecting the most suitable conveying solution for their operational needs.
Introduction to Sodium Bicarbonate Pneumatic Conveying
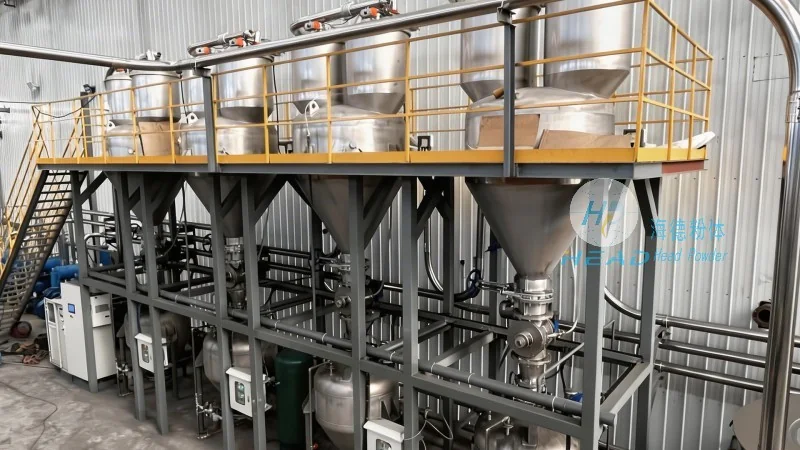
Sodium bicarbonate, also known as baking soda, is a versatile chemical used in food processing, pharmaceuticals, and industrial applications. Its light weight and fine particle size make it an ideal candidate for pneumatic conveying, which offers advantages such as dust-free operation, reduced contamination risk, and the ability to transport materials over long distances without the need for complex mechanical equipment. Pneumatic conveying systems for sodium bicarbonate typically involve the use of air or other gases to move the material through a pipeline, ensuring a clean and efficient transfer process.
Key Types of Pneumatic Conveying Systems for Sodium Bicarbonate
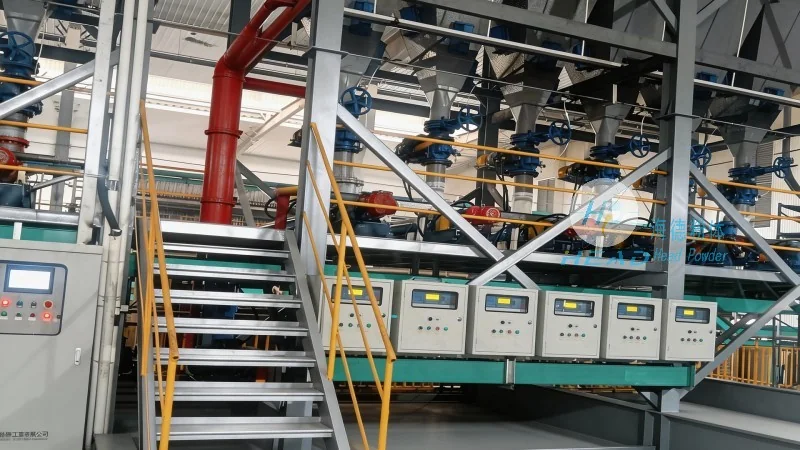
There are several primary types of pneumatic conveying systems designed for handling sodium bicarbonate, each with its own set of advantages and limitations. The most common systems include pressure, vacuum, and combined pressure-vacuum designs. Pressure systems use compressed air to push the material through the pipeline, while vacuum systems employ a vacuum to draw the material from the source. Combined systems offer the flexibility to handle both loading and unloading operations efficiently.
Features and Advantages of Sodium Bicarbonate Pneumatic Conveying
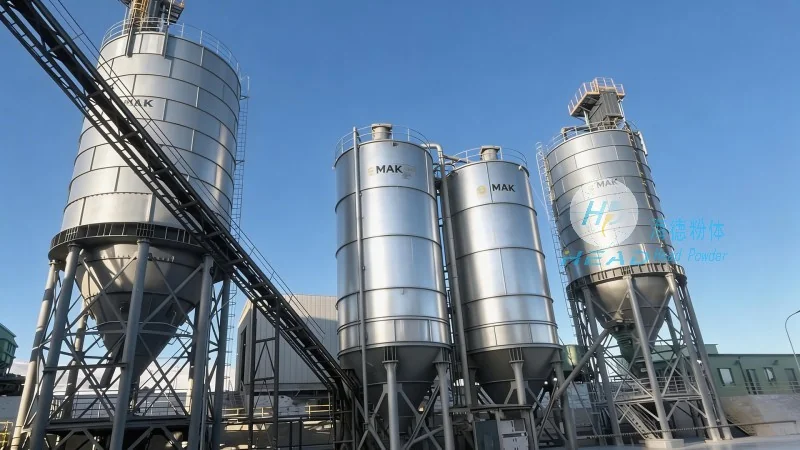
When considering the application of pneumatic conveying for sodium bicarbonate, several key features stand out. One of the most significant advantages is the ability to maintain a dust-free environment, which is crucial for industries where product purity is paramount. The system also allows for precise control over material flow rates, ensuring consistent delivery to processing equipment. Additionally, pneumatic conveying reduces the risk of product contamination from external sources, as the material is contained within a sealed pipeline. Another notable feature is the system's adaptability to different particle sizes and moisture levels, making it suitable for a wide range of sodium bicarbonate applications.
Application Ranges of Sodium Bicarbonate Pneumatic Conveying
The application range of sodium bicarbonate pneumatic conveying systems is broad and encompasses various industrial sectors. In the food industry, these systems are commonly used to transport sodium bicarbonate for baking, baking powder production, and other food processing applications. The pharmaceutical industry also relies on pneumatic conveying to handle sodium bicarbonate in the manufacturing of tablets, powders, and other dosage forms. Additionally, in the chemical and industrial sectors, the systems are used for bulk handling of sodium bicarbonate in storage and distribution operations. The versatility of pneumatic conveying makes it an ideal solution for both small-scale and large-scale operations, ensuring efficient material movement from storage to processing or packaging areas.
Conclusion and Company Overview
Choosing the right pneumatic conveying system for sodium bicarbonate is critical to optimizing operational efficiency and maintaining product quality. The systems discussed above offer distinct advantages, and the selection should be based on factors such as material characteristics, distance of transport, and operational requirements. For businesses seeking reliable and efficient solutions, Shandong HeadPowder Engineering Co., Ltd. provides expert guidance and customized systems tailored to specific needs. With a focus on quality and customer satisfaction, the company has established itself as a leader in the field of pneumatic conveying technology, serving clients across China and beyond. Based in Shandong, China, HeadPowder Engineering Co., Ltd. leverages its expertise to deliver innovative solutions that enhance the performance of sodium bicarbonate handling processes.