

Types, Features, and Applications of Headpowder Pneumatic Conveying Systems
Headpowder, an industry leader in pneumatic conveying technology, offers a comprehensive range of solutions tailored to diverse industrial needs. The company, formally known as Shandong HeadPowder Engineering Co., Ltd., is headquartered in Shandong, China, and specializes in designing, manufacturing, and implementing advanced pneumatic conveying systems. This article explores the key types, distinctive features, and broad application scopes of Headpowder's pneumatic conveying solutions, providing insights into how these systems enhance operational efficiency and material handling capabilities across various sectors.
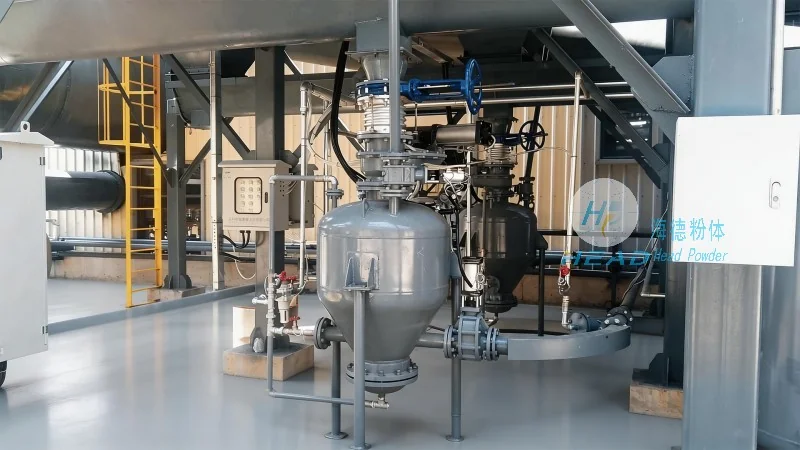
Overview of Headpowder Pneumatic Conveying Systems
Headpowder's pneumatic conveying systems are engineered to transport bulk materials such as powders, granules, and fine particles through a pressurized or vacuum environment. The core principle involves using air or gas to move materials from a source to a destination, eliminating the need for mechanical components like belts or buckets in many cases. This approach not only reduces maintenance costs but also minimizes material contamination, making it ideal for applications where product purity is critical.
Types of Pneumatic Conveying Systems
Headpowder offers several distinct types of pneumatic conveying systems, each designed to address specific operational requirements and material characteristics. The primary categories include:
1. Dilute Phase Pneumatic Conveying
Dilute phase systems are characterized by a low material-to-air ratio, typically operating at velocities of 20-30 meters per second. These systems are suitable for long-distance transport of light to medium-density materials. The design minimizes pressure drops and energy consumption, making them efficient for applications requiring high throughput over extended distances. Headpowder's dilute phase systems are equipped with advanced control mechanisms to maintain consistent flow rates and prevent material buildup in the pipeline.
2. Dense Phase Pneumatic Conveying
In contrast, dense phase systems operate at higher material-to-air ratios, often using lower velocities (5-15 meters per second) to achieve a more concentrated material flow. This method is particularly effective for transporting sensitive or abrasive materials, as it reduces particle impact and friction within the system. Headpowder's dense phase solutions are optimized for applications where material degradation or product quality must be preserved, such as in pharmaceutical or food processing industries.
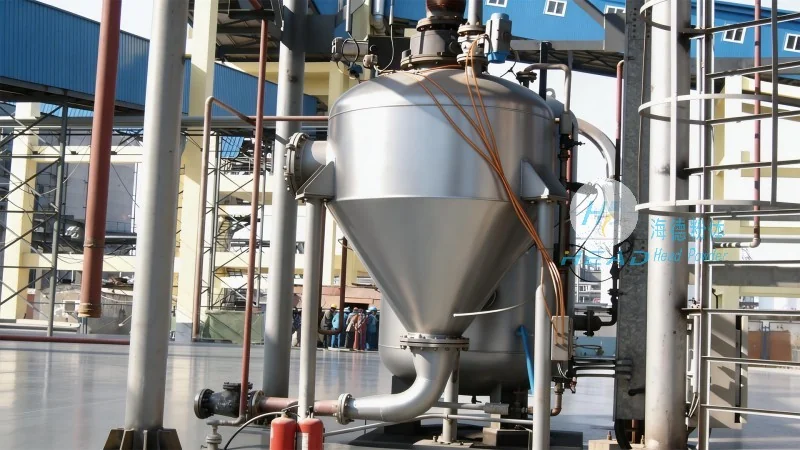
3. Vacuum Conveying Systems
Vacuum conveying systems utilize suction to draw materials from a source into a collection vessel. This approach is ideal for handling materials in confined spaces or for transferring materials from multiple points to a central location. Headpowder's vacuum systems are designed with high-efficiency suction nozzles and robust filtration to ensure clean and efficient material transfer, even for fine powders that are prone to clogging.
4. Pressure Conveying Systems
Pressure conveying systems operate by forcing air or gas through a pressurized pipeline to move materials. These systems are suitable for short to medium-distance transport of bulk materials and are commonly used in industries like chemical processing and cement production. Headpowder's pressure systems feature durable components and precise pressure control to ensure reliable operation and minimize energy waste.
Key Features of Headpowder Pneumatic Conveying Systems
Headpowder's pneumatic conveying systems are distinguished by several key features that enhance performance, reliability, and user experience. These features include:
1. Customizable Design and Integration
Each system is tailored to meet the specific needs of the client, whether it involves integrating with existing infrastructure or accommodating unique material properties. Headpowder's engineering team works closely with clients to develop solutions that align with their operational goals, ensuring optimal performance and minimal downtime.
2. Advanced Control and Monitoring
Modern pneumatic conveying systems require sophisticated control mechanisms to maintain consistent flow rates and detect potential issues in real-time. Headpowder's systems are equipped with digital control panels, sensors, and data logging capabilities, allowing operators to monitor performance and make adjustments as needed. This level of automation enhances efficiency and reduces the risk of material loss or system failure.
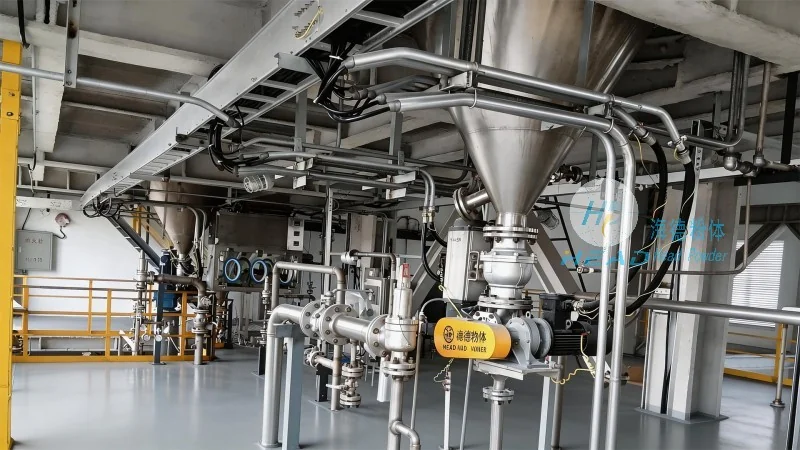
3. Durable and Low-Maintenance Components
Headpowder uses high-quality materials and components in the construction of its systems, ensuring longevity and reduced maintenance requirements. The use of corrosion-resistant materials and robust seals minimizes the risk of system failure due to wear or environmental factors. This focus on durability translates into lower operational costs over the system's lifespan.
4. Energy Efficiency and Environmental Compliance
With growing emphasis on sustainability, Headpowder's systems are designed to be energy-efficient, reducing operational costs and environmental impact. Advanced aerodynamic designs and optimized air flow management minimize energy consumption while maintaining effective material transport. Additionally, the systems comply with relevant environmental regulations, ensuring that they meet industry standards for emissions and waste management.
Application Ranges of Headpowder Pneumatic Conveying Systems
Headpowder's pneumatic conveying systems find applications across a wide range of industries, each addressing specific material handling challenges. The following are some of the primary sectors where these systems are utilized:
1. Chemical and Pharmaceutical Industries
In the chemical and pharmaceutical sectors, the need for clean, contamination-free material handling is paramount. Headpowder's systems are widely used to transport powders and granules used in drug manufacturing, ensuring that products remain free from contaminants and meet stringent quality standards. The systems' ability to maintain product integrity and prevent cross-contamination makes them indispensable in these industries.
2. Food and Beverage Processing
The food and beverage industry requires systems that are hygienic, easy to clean, and compliant with food safety regulations. Headpowder's pneumatic conveying solutions are designed with stainless steel components and sanitary connections, making them suitable for handling ingredients like flour, sugar, and spices. The systems' low maintenance and ability to prevent material contamination ensure that food products remain safe for consumption.
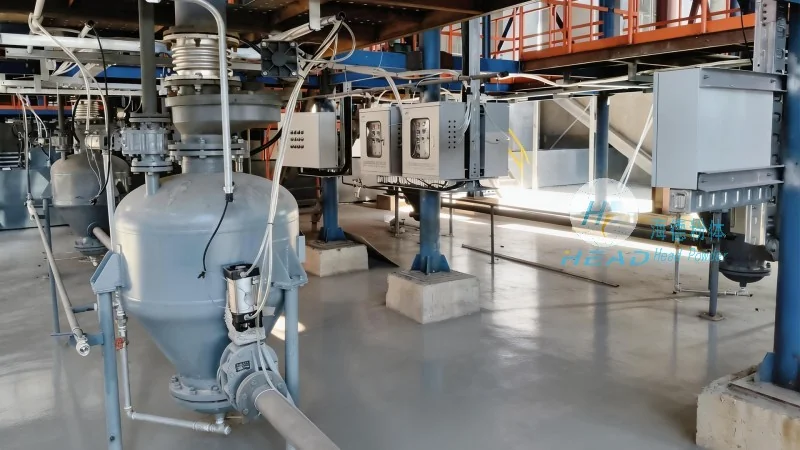
3. Cement and Construction Materials
For the cement and construction materials industry, efficient bulk material transport is critical to maintaining production schedules and reducing costs. Headpowder's systems are used to convey raw materials such as limestone, clay, and gypsum, as well as finished products like cement. The high throughput and reliability of these systems help construction companies meet project deadlines and improve overall operational efficiency.
4. Mining and Minerals Processing
In the mining sector, pneumatic conveying systems are used to transport minerals and ores from processing plants to storage or shipping facilities. Headpowder's robust systems are designed to handle abrasive and heavy materials, with components that can withstand the harsh conditions of mining operations. The systems' durability and low maintenance requirements make them a cost-effective solution for long-term material handling.
5. Plastics and Rubber Manufacturing
The plastics and rubber industry relies on efficient material transport to maintain production flow. Headpowder's systems are used to convey raw materials such as plastic pellets, rubber powders, and additives. The systems' ability to handle a wide range of materials and maintain consistent flow rates ensures that manufacturing processes run smoothly and without interruptions.
Conclusion
Headpowder's pneumatic conveying systems represent a sophisticated and versatile solution for bulk material handling across various industries. By offering a range of system types, customizable designs, and advanced features, Headpowder caters to the diverse needs of its clients. The company's commitment to quality, efficiency, and sustainability ensures that its systems not only meet current operational requirements but also adapt to future industry demands. Whether for chemical processing, food production, or construction, Headpowder's pneumatic conveying solutions provide reliable, cost-effective, and environmentally responsible material transport solutions.