

Airborne Conveying Systems Effectively Solve Sodium Hypochlorite Transportation Challenges
HeadPowder Engineering, a leading provider of specialized engineering solutions, specializes in the design and implementation of advanced airborne conveying systems tailored to address complex material handling challenges. With a focus on industrial applications, the company's expertise lies in developing safe, efficient, and reliable systems for transporting hazardous and corrosive materials such as sodium hypochlorite. This article explores how the company's innovative air conveying technology effectively mitigates the difficulties associated with sodium hypochlorite transportation, ensuring compliance with safety standards and operational efficiency.
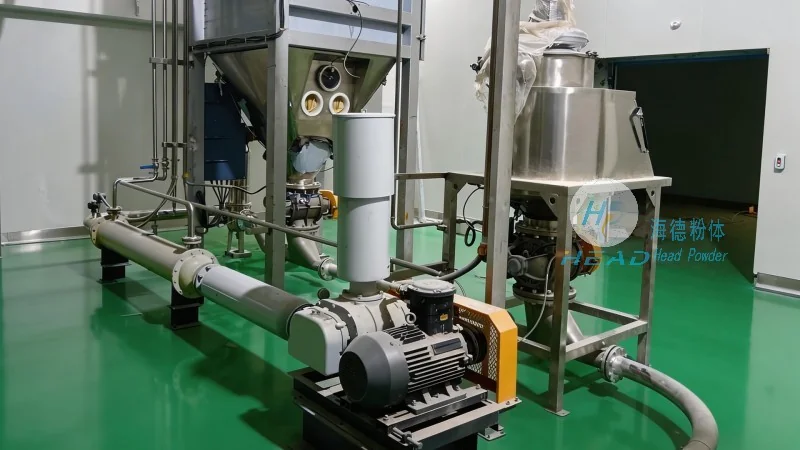
Understanding the Challenges of Sodium Hypochlorite Transportation
Sodium hypochlorite, commonly used as a disinfectant and bleaching agent in various industries, presents unique challenges when it comes to traditional transportation methods. This chemical is highly corrosive, reactive, and requires strict safety measures to prevent leaks, spills, and exposure risks. Traditional methods like pumping or trucking often involve open systems that expose personnel and the environment to hazardous conditions. Additionally, the need for continuous monitoring and control of the material's temperature and pressure adds complexity to the logistics. These factors make the selection of an appropriate conveying system critical for industries relying on sodium hypochlorite.
HeadPowder Engineering's Airborne Conveying Solutions
HeadPowder Engineering has developed state-of-the-art airborne conveying systems that offer a comprehensive solution to the transportation challenges of sodium hypochlorite. The core technology involves the use of air as the conveying medium, which allows for the safe and efficient movement of the chemical from storage to processing units. The system operates by creating a controlled airflow that transports the material through a network of pipes, ensuring complete containment and minimal exposure to personnel. This approach not only enhances safety but also reduces the risk of contamination and environmental impact.
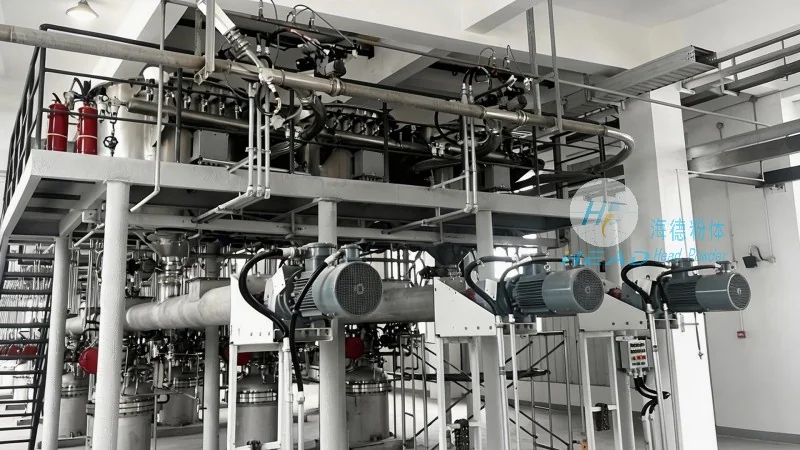
Key Features and Advantages of the Airborne Conveying System
The airborne conveying system implemented by HeadPowder Engineering incorporates several key features that make it ideal for sodium hypochlorite transport. Firstly, the system is designed with corrosion-resistant materials, such as stainless steel and specialized coatings, to withstand the chemical's aggressive properties. This ensures long-term durability and minimal maintenance requirements. Secondly, the system includes advanced control mechanisms that monitor and regulate the flow rate, pressure, and temperature of the material, maintaining optimal conditions throughout the conveying process. Thirdly, the enclosed design of the system prevents leaks and spills, aligning with stringent safety regulations and environmental standards. These features collectively contribute to a more reliable and cost-effective transportation solution.
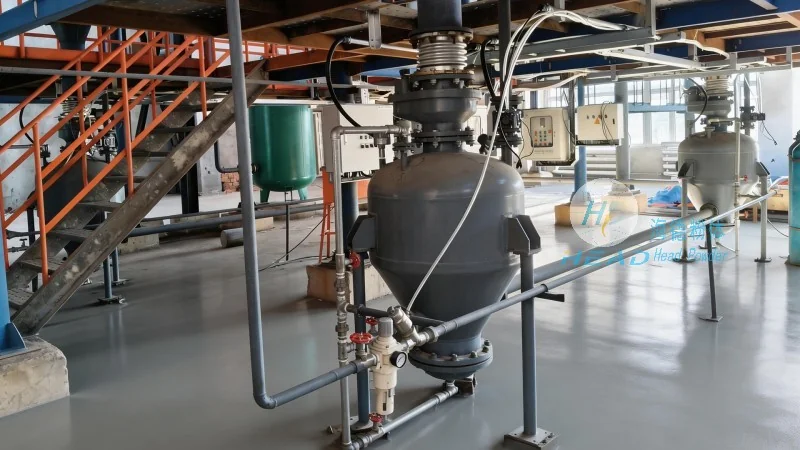
Enhancing Operational Efficiency and Safety
By adopting HeadPowder Engineering's airborne conveying system, industries can significantly improve their operational efficiency while maintaining high safety standards. The system's ability to handle sodium hypochlorite in a closed environment reduces downtime caused by maintenance or safety incidents. Additionally, the reduced need for manual handling and direct contact with the chemical minimizes the risk of accidents and exposure-related health issues. The system's scalability also allows for integration with existing infrastructure, making it a practical upgrade for both new and existing facilities. Overall, the solution provides a robust and sustainable approach to sodium hypochlorite transportation that meets the demands of modern industrial operations.
Conclusion and Company Overview
HeadPowder Engineering, based in Shandong, China, continues to lead the industry in providing innovative and effective solutions for material handling challenges. The company's commitment to research and development ensures that its airborne conveying systems remain at the forefront of technology, addressing the evolving needs of industries that rely on sodium hypochlorite. By combining advanced engineering with rigorous safety protocols, HeadPowder Engineering offers a reliable partner for businesses seeking to optimize their sodium hypochlorite transportation processes. The company's expertise and dedication to quality make it a trusted choice for industries looking to enhance efficiency, safety, and sustainability in their operations.