

Efficient High-Temperature Ash Transport via Pneumatic Conveying Systems
High-temperature ash transport is a critical challenge in industrial applications, particularly in power plants and thermal processing facilities. Traditional methods often face significant limitations when dealing with the extreme temperatures and abrasive properties of high-temperature ash. This article explores how pneumatic conveying systems, specifically designed for such demanding conditions, provide an effective solution to these challenges.
Challenges in High-Temperature Ash Transport
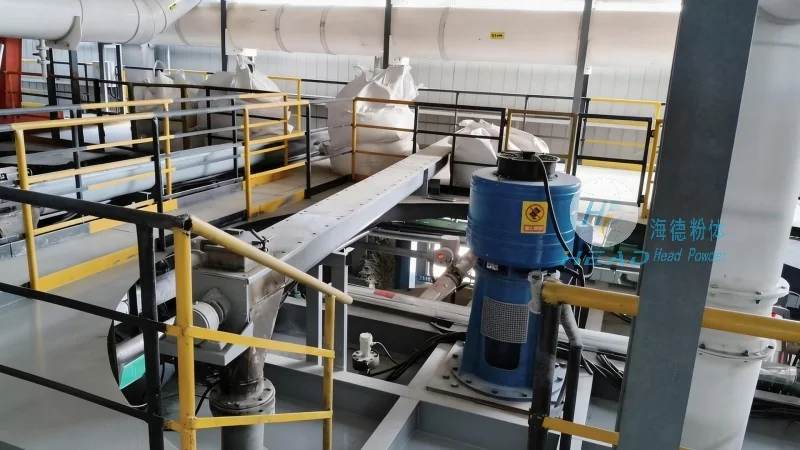
High-temperature ash, typically generated from coal combustion or other thermal processes, presents unique challenges for material handling. These challenges include extreme temperatures, which can range from several hundred to over a thousand degrees Celsius, and the abrasive nature of the ash particles. Conventional transport methods, such as mechanical conveyors or gravity-based systems, may suffer from equipment wear, material degradation, and operational inefficiencies under these harsh conditions. Additionally, the need for safe and reliable transport of ash to disposal or utilization sites adds another layer of complexity.
Pneumatic Conveying Systems: An Effective Solution
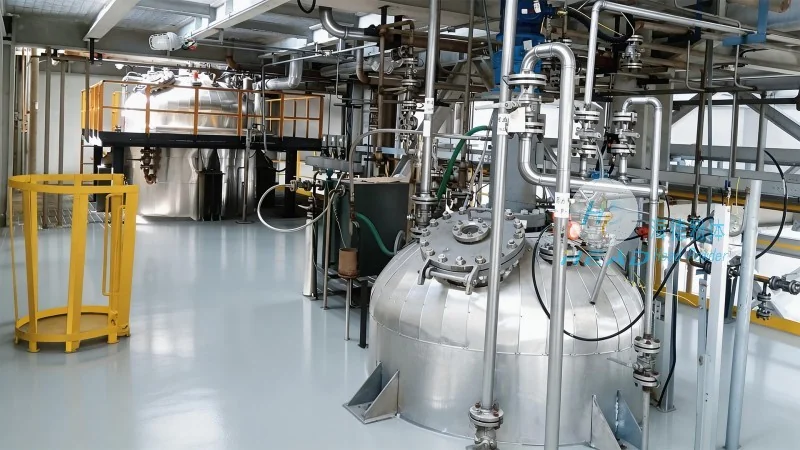
Shandong HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems tailored for high-temperature ash transport. These systems utilize compressed air or gas to transport bulk materials through a pipeline network, offering several advantages over traditional methods. The primary benefit is the ability to handle materials at elevated temperatures without the need for mechanical contact, thereby minimizing equipment wear and extending service life. Furthermore, pneumatic conveying systems provide a flexible and scalable solution, capable of transporting ash over long distances with minimal maintenance requirements.
How Pneumatic Conveying Systems Work
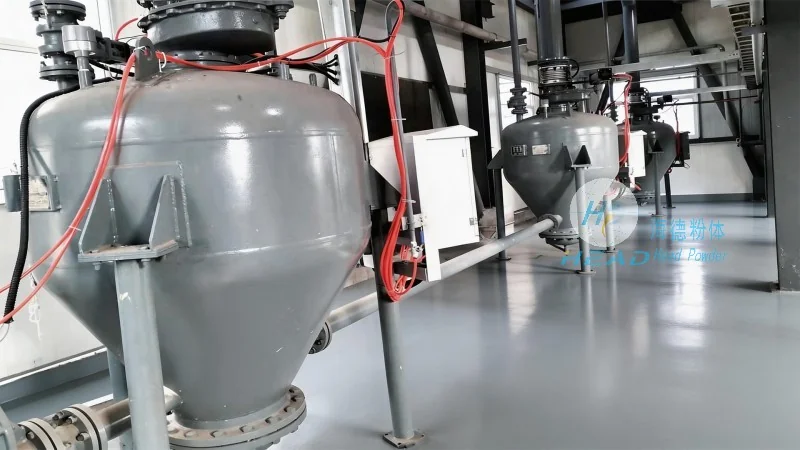
The core of a pneumatic conveying system for high-temperature ash involves a series of components working in concert. A primary air source, such as a blower or compressor, generates the necessary pressure to move the ash particles through the pipeline. The system typically includes a hopper or feeder to introduce the ash into the pipeline, a filter or separator to remove any excess air or particulate matter, and a discharge point where the ash is deposited at the destination. The design of the system, including the selection of materials for the pipeline and components, is critical to withstand the high temperatures and abrasive nature of the ash. For example, the use of heat-resistant materials like stainless steel or specialized alloys ensures the system's durability and reliability in harsh environments.
Key Advantages of High-Temperature Pneumatic Conveying
Implementing a pneumatic conveying system for high-temperature ash transport offers numerous benefits. First, it significantly reduces operational costs by minimizing equipment downtime and maintenance expenses. The absence of moving parts in the pipeline reduces wear and tear, leading to lower replacement costs over time. Second, the system enhances safety by eliminating the need for manual handling of hot ash, reducing the risk of burns or other injuries. Third, the flexibility of the system allows for easy integration with existing infrastructure, making it a cost-effective upgrade for existing facilities. Additionally, the ability to transport ash over long distances without the need for intermediate storage or handling points improves overall operational efficiency.
About Shandong HeadPowder Engineering Co., Ltd.
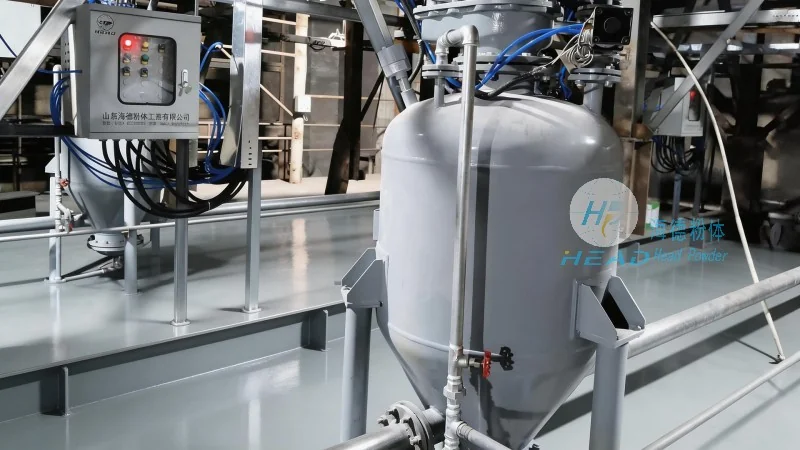
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of specialized engineering solutions for bulk material handling. With a focus on innovation and quality, the company has developed advanced pneumatic conveying systems that address the unique challenges of high-temperature ash transport. Headpowder's expertise lies in designing customized solutions that meet the specific requirements of industrial clients, ensuring reliable and efficient operation. The company's headquarters is located in Shandong, China, where it continues to advance its technology and serve the global market with cutting-edge solutions.