

Long - distance Pneumatic Conveying System for Dry Pebbles
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for the efficient transport of dry pebbles over extended distances. The company's expertise lies in creating robust, reliable solutions that meet the demanding requirements of modern material handling operations.
System Overview and Core Technology
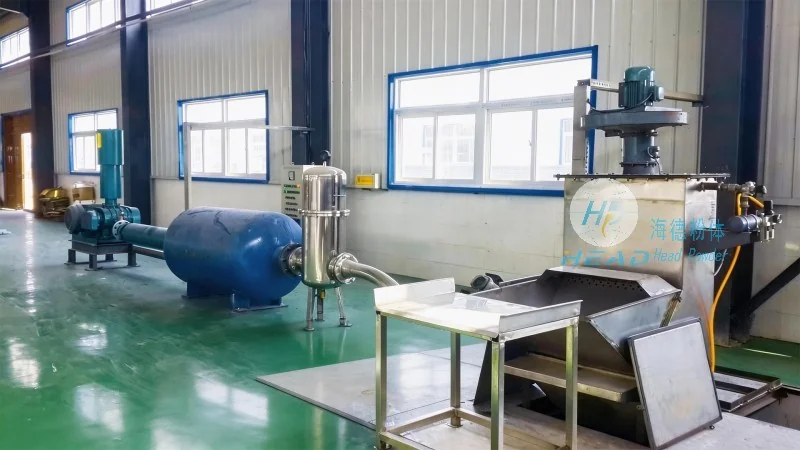
The long - distance pneumatic conveying system for dry pebbles is engineered to handle the unique challenges associated with transporting granular materials like pebbles. By utilizing compressed air as the primary driving force, the system efficiently moves dry pebbles from the source to the destination without the need for mechanical components such as belts or buckets. This approach not only minimizes maintenance but also ensures a clean and dust - free operation, which is crucial for applications where material purity is a priority.
Key Components and Design Features
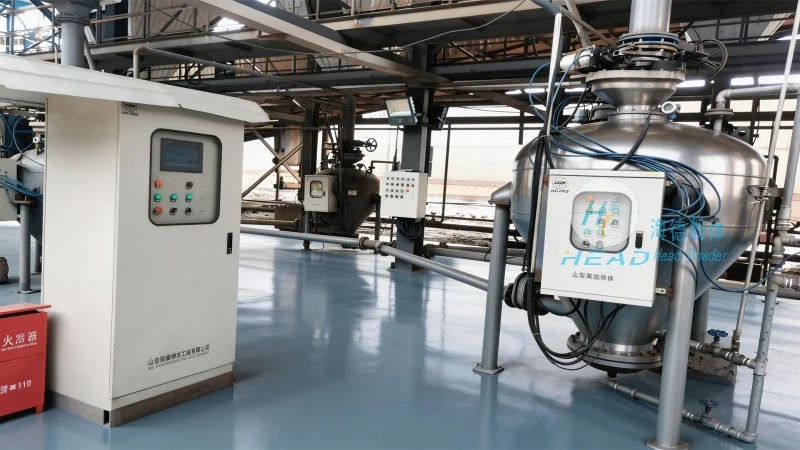
At the heart of the system are several critical components that work in tandem to ensure optimal performance. The feed hopper is designed to accommodate bulk dry pebbles, providing a consistent flow of material into the conveying line. The air compressor, a high - efficiency unit, generates the necessary pressure to propel the pebbles through the pipeline. The pipeline itself is constructed from durable materials, such as stainless steel or specialized polymers, to withstand the abrasive nature of pebbles and resist corrosion. Additionally, the system incorporates a series of control valves and sensors that monitor pressure, flow rate, and material level, allowing for real - time adjustments and ensuring safe operation.
Advantages and Applications
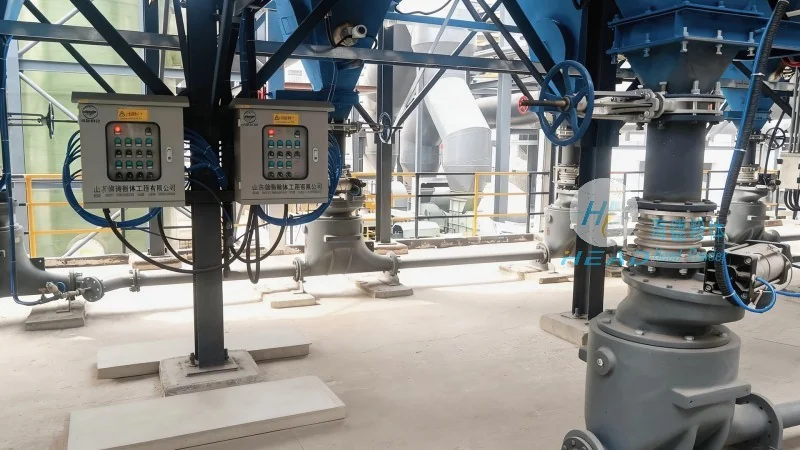
HeadPowder's long - distance pneumatic conveying system for dry pebbles offers numerous advantages over traditional mechanical conveying methods. The primary benefit is the reduction in labor costs and maintenance expenses, as there are no moving parts that require frequent servicing. Furthermore, the system is highly flexible, capable of transporting pebbles over distances ranging from several hundred meters to several kilometers, making it suitable for various industrial applications. Common uses include the transport of pebbles from mining sites to processing facilities, from storage silos to production lines, and even for material transfer between different parts of a manufacturing plant. The system's ability to maintain the integrity of the pebbles, preventing breakage or contamination, makes it ideal for applications where the quality of the material is paramount.
Customization and Installation Services
HeadPowder understands that each project has unique requirements. Therefore, the company offers comprehensive customization services to tailor the pneumatic conveying system to the specific needs of the client. This includes selecting the appropriate air compressor capacity, determining the optimal pipeline diameter and length, and integrating additional features such as dust collection or material separation systems. The engineering team at HeadPowder works closely with clients to assess their operational needs, conduct feasibility studies, and develop detailed system designs. Once the design is finalized, the company provides full - service installation and commissioning, ensuring that the system is installed correctly and operates at peak efficiency from the start. The company's commitment to quality and customer satisfaction is reflected in its rigorous testing procedures and post - installation support, which helps to minimize downtime and maximize the system's lifespan.
Quality Assurance and Reliability
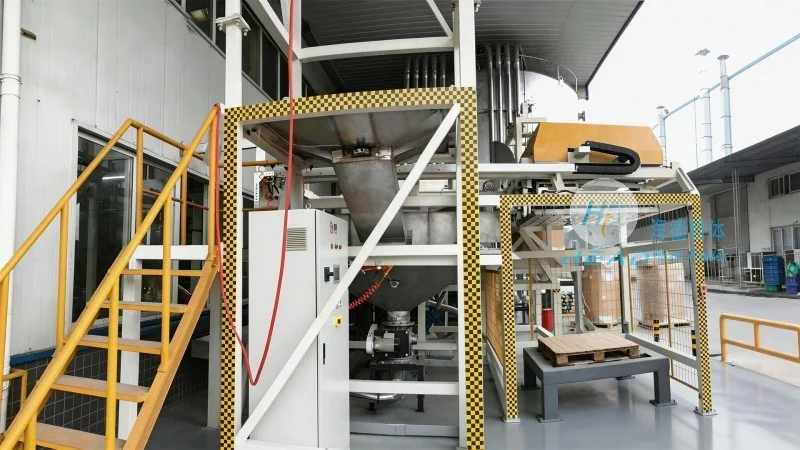
HeadPowder places a strong emphasis on quality assurance throughout the entire production and installation process. All components used in the pneumatic conveying system are sourced from reputable manufacturers and undergo strict quality checks to ensure they meet or exceed industry standards. The company adheres to international quality management systems, such as ISO 9001, to maintain consistent quality in its products and services. This commitment to quality is reflected in the high reliability of the systems, which are designed to operate continuously with minimal interruptions. HeadPowder's systems have a proven track record of long - term performance, with many installations still in operation after years of service, providing clients with a reliable and cost - effective solution for their material handling needs.