

Operation Process and Working Principle of Dilute Phase Powder Pneumatic Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd., a professional manufacturer based in Shandong, China, specializes in the design, development, and production of dilute phase powder pneumatic conveying equipment. This equipment is widely used in various industrial sectors for efficient and reliable powder material transportation. The following content provides a detailed overview of the operation process and working principle of such equipment, highlighting its key features and practical applications.
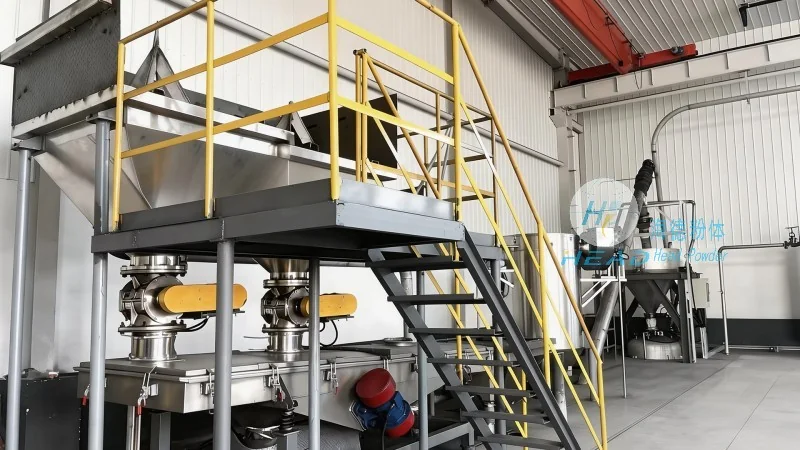
Overview of Dilute Phase Pneumatic Conveying Systems
Dilute phase pneumatic conveying systems are designed to transport bulk powder materials through a pipeline using a stream of air or gas. Unlike dense phase systems, which operate at higher material concentrations, dilute phase systems typically maintain a low concentration of powder in the conveying medium. This approach is particularly effective for long-distance and high-capacity material transport, making it suitable for a wide range of industries including chemical, pharmaceutical, food processing, and mining.
Key Components of the Equipment
The dilute phase powder pneumatic conveying equipment consists of several critical components that work in tandem to ensure efficient operation. These components include the material feeder, the air compressor or blower, the conveying pipeline, the separation and collection system, and the control unit. Each component plays a vital role in the overall performance and reliability of the system.
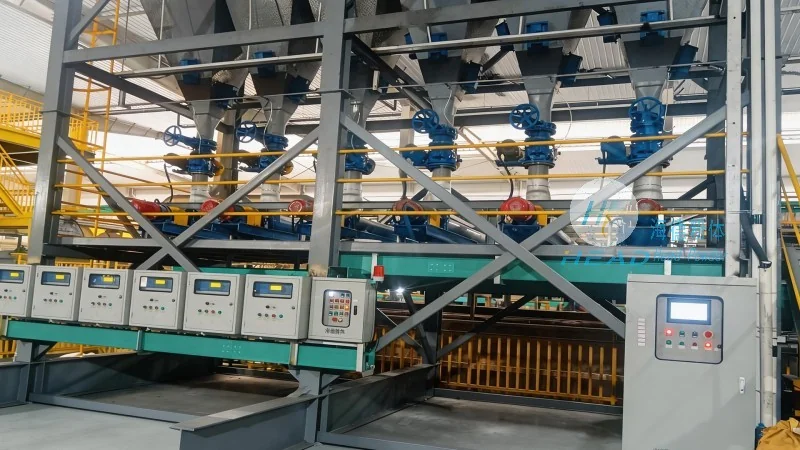
Operation Process of the Dilute Phase System
The operation process of a dilute phase powder pneumatic conveying system begins with the material being fed into the system. The feeder, which can be a rotary valve, screw feeder, or other type of feeder, ensures a consistent and controlled flow of the powder into the pipeline. Simultaneously, the air compressor or blower generates a high-pressure air stream that is introduced into the pipeline at the feeding point. As the air and powder mixture moves through the pipeline, the material is suspended and carried by the air flow. The conveying process continues until the material reaches the end of the pipeline, where it is separated from the air and collected in a storage or processing unit.
Working Principle of the Dilute Phase System
The working principle of the dilute phase system is based on the principle of fluidization and suspension. The air flow in the pipeline creates a low-pressure zone that draws the powder particles into the conveying stream. The velocity of the air is maintained at a level sufficient to keep the powder particles suspended, preventing them from settling or clogging the pipeline. The system operates under a pressure differential, with the air compressor providing the necessary pressure to overcome the resistance in the pipeline and the gravitational forces acting on the powder particles. The separation and collection system at the end of the pipeline uses cyclones, filters, or other devices to separate the powder from the air, ensuring that the material is collected in a clean and efficient manner.
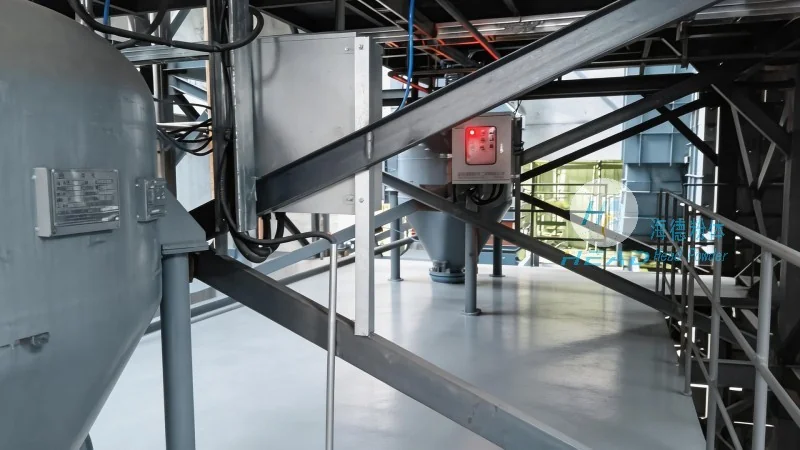
Advantages and Applications
Dilute phase powder pneumatic conveying equipment offers several advantages over traditional methods of material transport, such as mechanical conveying or manual handling. These advantages include high transport efficiency, minimal material degradation, and the ability to handle a wide range of powder types and sizes. The system is also flexible and can be easily integrated into existing industrial processes. Due to these benefits, the equipment is widely used in various applications, including the transport of raw materials in chemical plants, the delivery of pharmaceutical powders in pharmaceutical manufacturing, and the handling of food ingredients in food processing facilities.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. provides high-quality dilute phase powder pneumatic conveying equipment that is designed to meet the specific needs of various industrial applications. The equipment operates efficiently and reliably, ensuring that powder materials are transported safely and effectively. With its advanced design and robust construction, the equipment is suitable for long-term use in demanding industrial environments. By understanding the operation process and working principle of dilute phase pneumatic conveying systems, users can make informed decisions about their material handling needs and select the most appropriate equipment for their specific requirements.