

Principle and Working Scene Characteristics of Stone Aggregate Powder Pneumatic Conveying System
For industries dealing with stone aggregate powders, efficient material handling is crucial. The pneumatic conveying system, particularly designed for stone aggregate powders, offers a reliable solution that integrates principles of fluidization and air dynamics to transport bulk materials over varying distances. This article explores the fundamental principles behind such systems and highlights key working scene characteristics that make them suitable for diverse industrial applications.
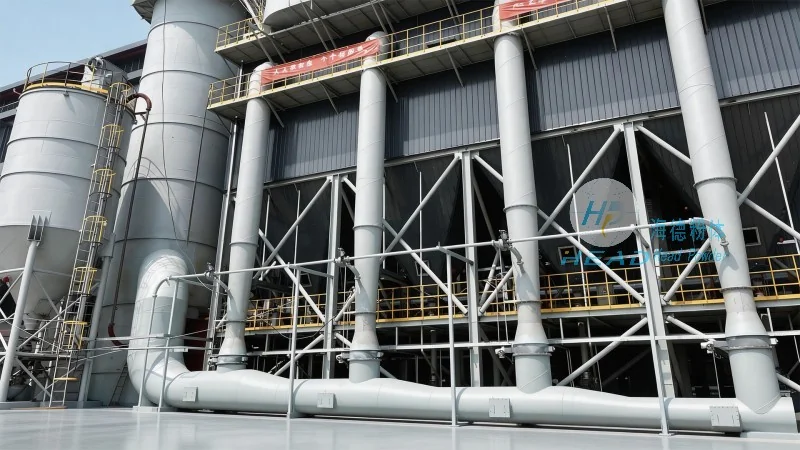
Core Principles of Pneumatic Conveying for Stone Aggregate Powders
The operation of a stone aggregate powder pneumatic conveying system is based on the principle of transporting particulate materials using a stream of air or gas. The system typically consists of a hopper, a conveyor line, and a receiver. The material is fed into the hopper, where it is pneumatically lifted by the air stream. The air velocity is carefully controlled to ensure that the particles remain suspended and move through the pipeline without settling or clogging. Key factors influencing the system's performance include particle size distribution, moisture content, and the air pressure or velocity used. By optimizing these parameters, the system can achieve high efficiency in transporting stone aggregate powders, minimizing material loss and operational downtime.
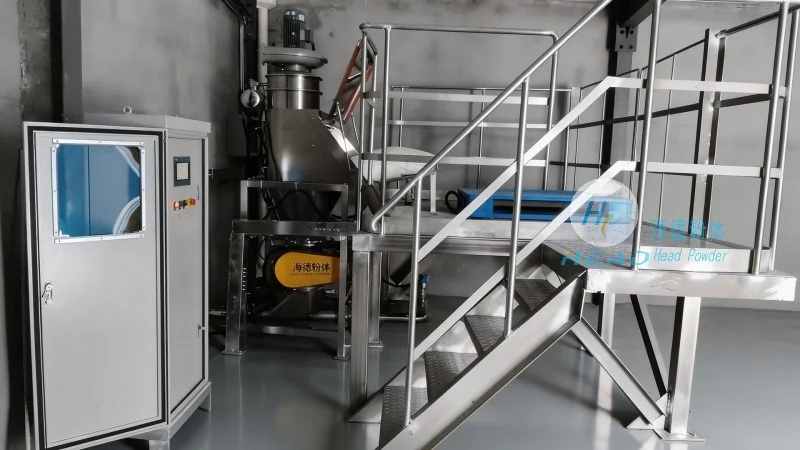
Working Scene Characteristics and Applications
The stone aggregate powder pneumatic conveying system is widely applied in various industrial scenarios. In construction material processing, it is used to transport crushed stone, sand, and other aggregates from storage silos to processing plants or construction sites. The system's ability to handle large volumes of material with minimal space requirements makes it ideal for urban construction projects where space is limited. Additionally, in mining operations, the system is employed to transport crushed ore and fine powders from processing facilities to storage or shipping areas. The system's adaptability to different particle sizes and moisture levels allows it to handle a wide range of stone aggregate powders, from coarse gravel to fine sand. In the chemical industry, it is used to convey raw materials such as limestone and silica powders, which are essential components in the production of cement and other building materials. The system's low maintenance requirements and ability to operate in harsh environments further enhance its suitability for these applications.
Advantages and Operational Considerations
Implementing a stone aggregate powder pneumatic conveying system offers several advantages over traditional methods like belt conveyors or trucks. One of the primary benefits is the reduction in material handling costs, as the system eliminates the need for manual loading and unloading. Additionally, the system provides a more hygienic and dust-free environment, which is crucial for industries where material contamination is a concern. The system also allows for better control over material flow, enabling precise dosing and batching. However, operational considerations must be taken into account to ensure optimal performance. For instance, the system's design must account for the specific properties of the stone aggregate powders, such as their density and abrasiveness, to prevent pipeline wear and tear. Regular maintenance of the air filtration system and pipeline is also essential to prevent dust accumulation and ensure consistent air quality. By addressing these considerations, the system can operate efficiently and reliably, delivering consistent performance over extended periods.
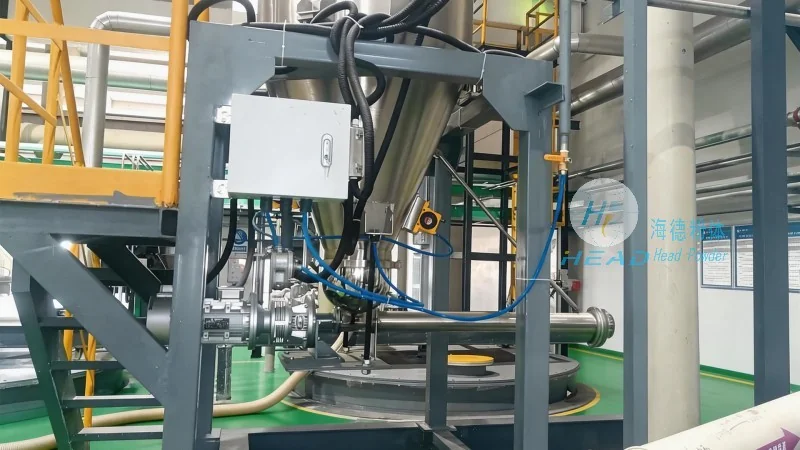
Conclusion and Company Overview
The stone aggregate powder pneumatic conveying system is a sophisticated solution that leverages principles of fluid dynamics to efficiently transport bulk materials. Its versatility and adaptability make it suitable for a wide range of industrial applications, from construction to mining and chemical processing. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of clients. With a focus on innovation and quality, the company ensures that its systems meet the highest standards of performance and reliability. Based in Shandong, China, HeadPowder offers comprehensive solutions that enhance material handling efficiency and reduce operational costs for industries dealing with stone aggregate powders. By understanding the unique characteristics of each application, the company provides tailored systems that optimize material flow and minimize downtime, contributing to the overall productivity and success of its clients' operations.