

Working Principle and Features of Sulfur Tablet Powder Pneumatic Conveying Equipment
For industrial applications involving the handling of sulfur tablets, efficient and reliable material transport is crucial. The sulfur tablet powder pneumatic conveying equipment, provided by Shandong HeadPowder Engineering Co., Ltd., is a specialized system designed to address these needs. This equipment ensures safe and effective transportation of sulfur tablet powders, minimizing material loss and operational risks.
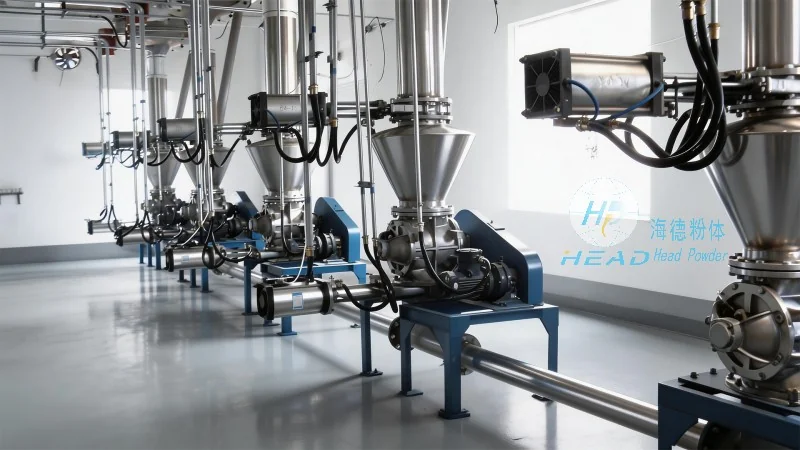
Working Principle of Sulfur Tablet Powder Pneumatic Conveying Equipment
The core operation of the sulfur tablet powder pneumatic conveying system relies on the principles of air flow and pressure differentials. The system typically consists of a hopper for material storage, a blower or compressor to generate airflow, and a pipeline network that transports the sulfur tablets. As the sulfur tablets are fed into the hopper, the air is introduced at a controlled pressure, creating a vacuum or positive pressure environment that propels the material through the pipes. The design ensures that the tablets are conveyed without excessive breakage or degradation, maintaining the integrity of the material.
During the conveying process, the air velocity is carefully managed to prevent blockages and ensure smooth flow. The system may incorporate features such as cyclone separators or filters to separate the conveyed material from the air, allowing for the collection of the sulfur tablets at the destination point. This separation process is critical for maintaining product purity and preventing contamination. The entire operation is automated, with sensors and controls monitoring pressure, flow rates, and material levels to optimize performance and ensure consistent operation.
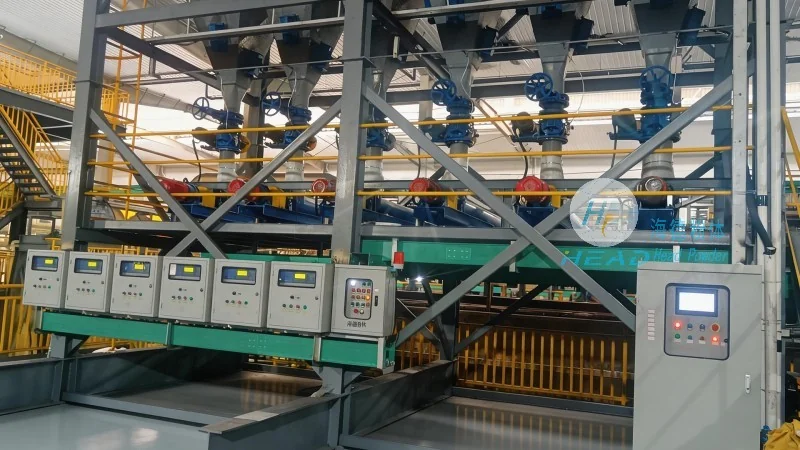
Key Features of Sulfur Tablet Powder Pneumatic Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd. offers several distinctive features that enhance the functionality and efficiency of the sulfur tablet powder pneumatic conveying equipment. One of the primary advantages is the ability to handle abrasive or delicate materials like sulfur tablets without causing damage. The system's design minimizes friction and impact, preserving the tablet's shape and quality. Additionally, the equipment is equipped with advanced control systems that allow for precise regulation of air pressure and flow, ensuring consistent and reliable transport.
Another notable feature is the system's flexibility in terms of layout and integration. It can be customized to fit various industrial settings, with options for vertical or horizontal conveying paths. The equipment also includes safety features, such as pressure relief valves and emergency shut-off mechanisms, to prevent accidents and protect personnel. Furthermore, the use of high-quality materials in construction ensures durability and longevity, reducing maintenance costs over time.
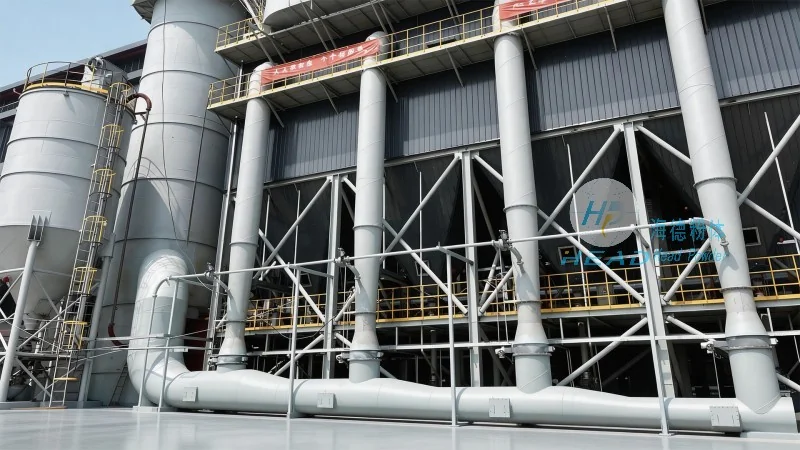
Benefits for Industrial Applications
The implementation of sulfur tablet powder pneumatic conveying equipment brings numerous benefits to industrial operations. By eliminating the need for manual handling, the system reduces labor costs and minimizes the risk of workplace injuries. The automated process also improves operational efficiency, allowing for continuous material flow without interruptions. Additionally, the system's ability to maintain product integrity ensures that the sulfur tablets remain in optimal condition, which is essential for downstream processing or storage.
From a safety perspective, the pneumatic conveying system reduces exposure to dust and airborne particles, creating a healthier work environment. The enclosed design also prevents cross-contamination, which is particularly important in industries where product purity is critical. Overall, the equipment from Shandong HeadPowder Engineering Co., Ltd. provides a comprehensive solution for the efficient and safe transportation of sulfur tablets, supporting the smooth operation of industrial processes.