

Working Principle and Features of Activated Carbon Material Handling System Equipment
HeadPowder, a leading provider of industrial material handling solutions, specializes in the design and manufacturing of activated carbon material handling systems. This article delves into the working principle and key features of such equipment, offering insights into its functionality and advantages for various industrial applications.
Introduction to Activated Carbon Material Handling Systems
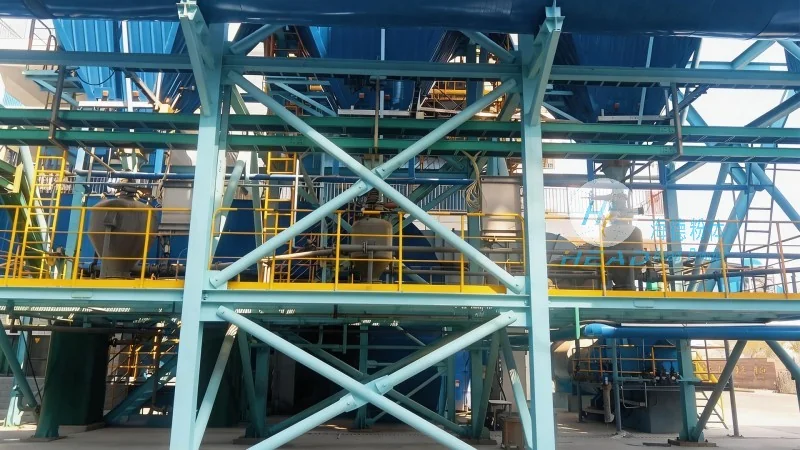
Activated carbon is widely used in industrial processes for adsorption, filtration, and purification. Efficient handling of this material is crucial to ensure optimal performance and safety in operations. The activated carbon material handling system equipment, developed by Shandong HeadPowder Engineering Co., Ltd., addresses these needs by integrating advanced technology and robust engineering. Based in Shandong, China, HeadPowder leverages local expertise and resources to deliver high-quality solutions tailored to client requirements.
The Working Principle of Activated Carbon Material Handling Equipment
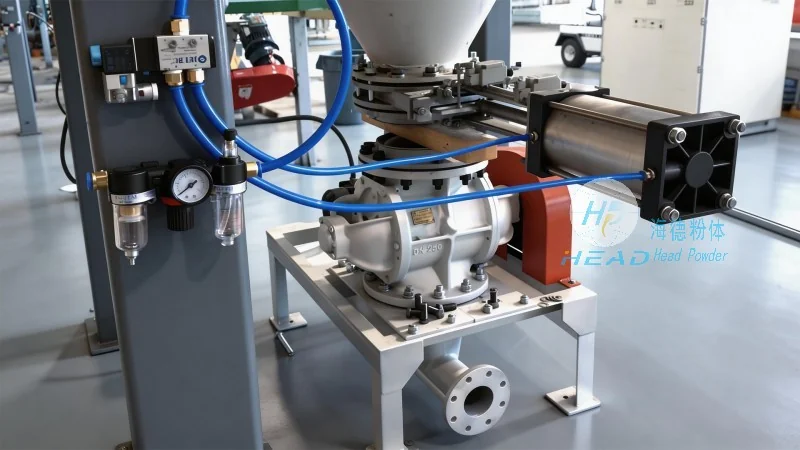
The core working principle of the activated carbon material handling system involves the seamless transfer and processing of activated carbon from storage to processing units. The system typically comprises several key components, including storage silos, conveyor systems, feeding mechanisms, and control panels. The process begins with the activated carbon being stored in bulk in the silos. A feeding mechanism, often equipped with a screw conveyor or pneumatic system, then transports the material from the silo to the processing line. The conveyor system ensures a continuous and controlled flow of the material, minimizing dust generation and ensuring uniform distribution. The control panel allows operators to monitor and adjust the flow rate, pressure, and other parameters to maintain optimal performance. This integrated approach ensures that the activated carbon is handled safely and efficiently, reducing the risk of spills, contamination, and operational disruptions.
Key Features of the Activated Carbon Material Handling System
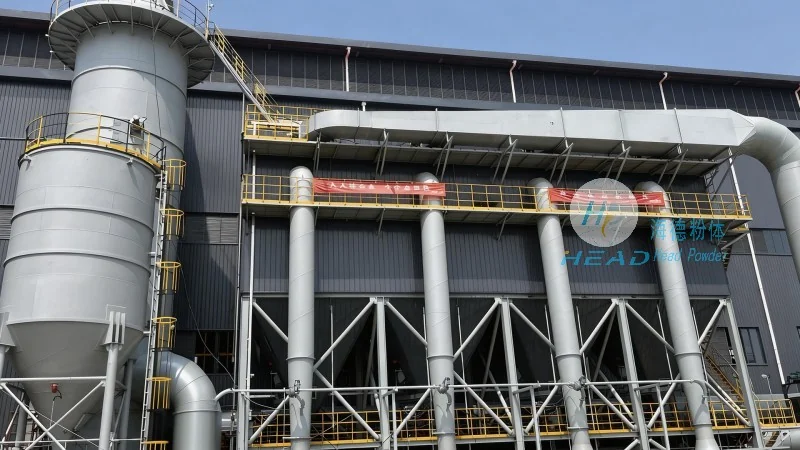
The activated carbon material handling system by Shandong HeadPowder Engineering Co., Ltd. is distinguished by several key features that enhance its performance and usability. Firstly, the system is designed for high efficiency and reliability, with components engineered to withstand the demands of continuous industrial operation. The use of robust materials and advanced manufacturing techniques ensures durability and long service life. Secondly, the system offers flexibility in handling different types of activated carbon, including various grades and particle sizes. This adaptability allows it to be integrated into diverse industrial processes, such as water treatment, air purification, and chemical processing. Thirdly, the equipment is equipped with advanced safety features, including dust suppression systems, emergency stop mechanisms, and real-time monitoring capabilities. These features help to maintain a safe working environment and comply with industrial safety regulations. Additionally, the system incorporates user-friendly control interfaces, making it easy for operators to manage and adjust the operation. The integration of automation and sensors further enhances operational efficiency, reducing the need for manual intervention and minimizing human error.
Applications and Benefits
The activated carbon material handling system is widely used in various industrial sectors, including environmental protection, chemical manufacturing, and pharmaceuticals. In water treatment plants, it helps to remove impurities and contaminants from water, improving water quality. In air purification systems, it absorbs harmful gases and odors, providing clean air. In chemical processing, it aids in the purification of chemicals and the removal of byproducts. The benefits of using this system include improved operational efficiency, reduced downtime, and enhanced safety. By automating the material handling process, it minimizes the risk of human error and ensures consistent performance. The system also helps to reduce labor costs and improve overall productivity. Furthermore, the use of advanced technology ensures that the system meets the highest standards of quality and performance, making it a reliable choice for industrial applications.
Conclusion
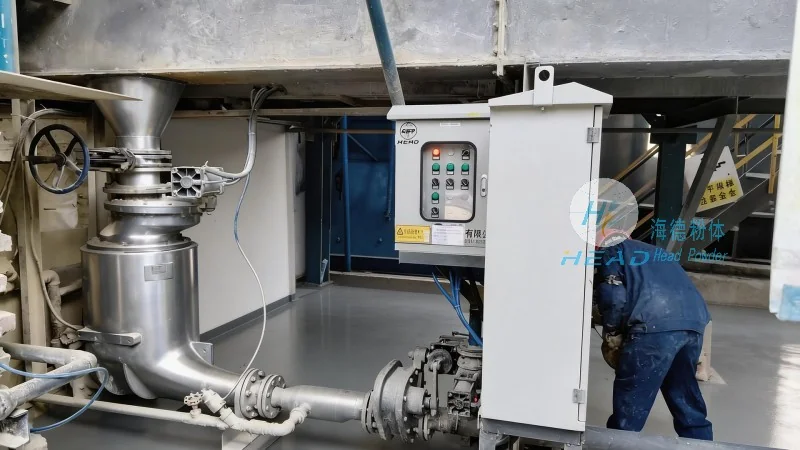
Shandong HeadPowder Engineering Co., Ltd. offers a comprehensive activated carbon material handling system that combines advanced technology with robust engineering. The system's working principle and key features make it an efficient and reliable solution for handling activated carbon in various industrial applications. With its focus on safety, efficiency, and adaptability, the system is designed to meet the evolving needs of the industry. HeadPowder's commitment to quality and customer satisfaction ensures that clients receive a product that not only meets but exceeds their expectations. As a leading provider of industrial material handling solutions, HeadPowder continues to innovate and deliver solutions that enhance operational performance and safety in industrial settings.