

Working Principle and Features of Cement Aggregate Powder Conveyors
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced cement aggregate powder conveyors. These systems are engineered to efficiently handle bulk materials like cement, aggregates, and other fine powders, playing a crucial role in various industrial applications. This article explores the working principle and key features of these conveyors, highlighting their importance in material handling processes.
Working Principle of Cement Aggregate Powder Conveyors
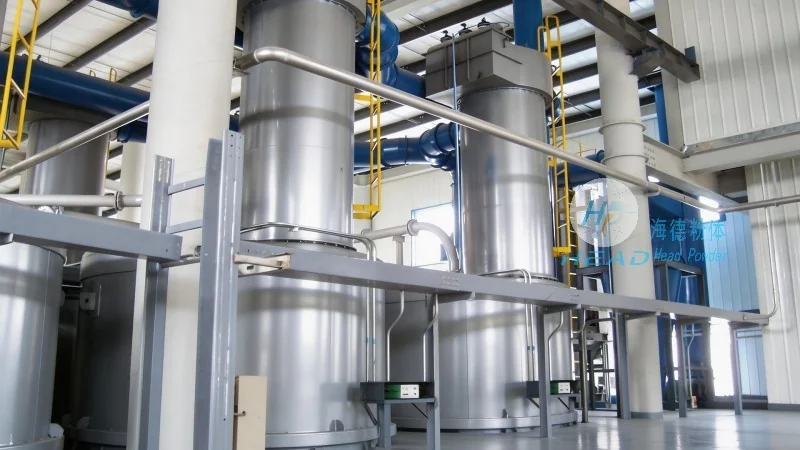
The core working principle of cement aggregate powder conveyors involves the use of a continuous belt or screw mechanism to transport dry bulk materials. The system typically consists of a hopper for material storage, a conveyor belt or screw that moves the material along a designated path, and a discharge outlet for material release. As the material is fed into the hopper, it is drawn into the conveyor system by the rotating components. The continuous motion of the conveyor ensures a steady flow of material, minimizing downtime and enhancing operational efficiency. The design incorporates features such as adjustable speed controls and material flow monitoring to optimize performance and prevent blockages. The conveyor may also include a dust collection system to maintain a clean and safe working environment, which is critical in industrial settings where fine powders are handled.
Key Features and Advantages
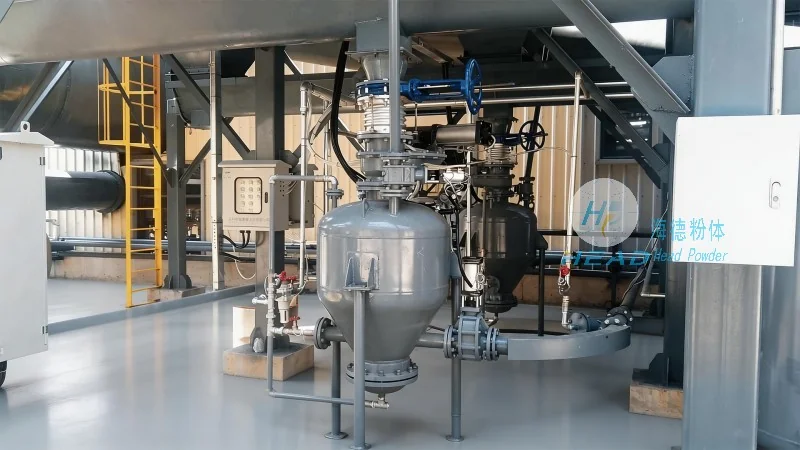
Cement aggregate powder conveyors from HeadPowder are equipped with several distinctive features that set them apart in the market. One of the primary advantages is their high capacity and reliability, capable of handling large volumes of material with minimal maintenance. The systems are designed for durability, using robust materials and components that can withstand the rigors of continuous operation in demanding environments. Another notable feature is the modular design, which allows for easy installation and integration into existing production lines. This modularity also facilitates maintenance and repairs, as individual components can be replaced without disrupting the entire system. The conveyors are also equipped with advanced control systems, including variable speed drives and real-time monitoring, enabling operators to adjust the flow rate according to specific requirements. This adaptability ensures optimal performance and reduces energy consumption. Additionally, the systems are designed to minimize dust emissions, incorporating sealed housing and efficient filtration to comply with environmental regulations and ensure workplace safety.
Technical Specifications and Design Considerations
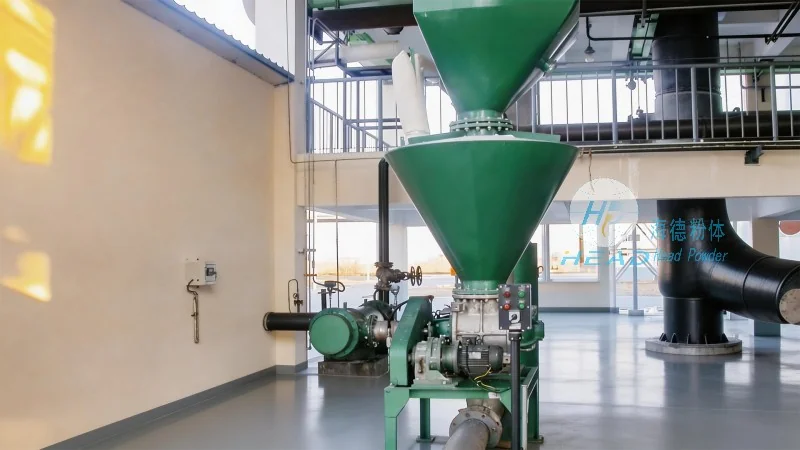
HeadPowder's cement aggregate powder conveyors are engineered with precision, adhering to strict technical specifications to ensure performance and safety. The conveyor systems are available in various configurations, including belt conveyors, screw conveyors, and pneumatic conveyors, each tailored to specific material characteristics and application needs. The belt conveyors are ideal for transporting bulk materials over short to medium distances, while screw conveyors are suitable for vertical or inclined transport. Pneumatic conveyors, on the other hand, use air pressure to move fine powders, offering flexibility in material handling. The design incorporates features such as adjustable inclination angles, which allow for vertical lifting of materials, and variable speed controls to regulate the flow rate. The systems are also equipped with safety features, including emergency stop buttons and overload protection, to prevent accidents and ensure operator safety. The materials used in the construction of the conveyors are selected for their resistance to corrosion and wear, ensuring long-term durability and minimal maintenance.
Application Scenarios and Industry Use Cases
Cement aggregate powder conveyors are widely used in various industries, including construction, mining, and manufacturing. In the construction industry, these systems are essential for transporting cement, sand, and aggregates to construction sites, ensuring a steady supply of materials for concrete production. The mining industry utilizes these conveyors to transport ore and other bulk materials from mines to processing facilities, improving operational efficiency and reducing transportation costs. In manufacturing, the conveyors are used to handle raw materials and finished products, streamlining production processes and enhancing overall productivity. The versatility of these systems makes them suitable for a wide range of applications, from small-scale operations to large industrial facilities. The ability to handle different materials and adjust to varying production demands makes cement aggregate powder conveyors a valuable asset in any industrial setting.
Company Profile and Contact Information
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a reputable manufacturer specializing in the production of high-quality material handling equipment. With years of experience in the industry, the company has established itself as a leader in the design and manufacturing of cement aggregate powder conveyors. HeadPowder's commitment to quality and innovation has enabled them to develop advanced systems that meet the evolving needs of the market. The company's products are known for their reliability, efficiency, and durability, making them a preferred choice for industrial applications. For more information about their cement aggregate powder conveyors and other products, please contact HeadPowder Engineering Co., Ltd. at their address in Shandong, China.