

Working Principle and Features of Powdered Electrolyte Powder Conveying Systems
Powdered electrolyte powder conveying systems are critical components in various industrial applications, particularly in the battery manufacturing and material processing sectors. These systems are designed to efficiently transport fine powders, such as those used in lithium-ion batteries, ensuring consistent flow and minimal material loss. The technology behind these systems combines advanced engineering principles with precision control mechanisms to meet the stringent requirements of modern production lines. In battery production, for instance, the electrolyte powder is a key component that must be delivered to the mixing and coating stages with high accuracy. The conveying system plays a vital role in maintaining the quality and consistency of the final battery products. By ensuring that the powder is transported without agglomeration or degradation, the system contributes to the overall performance and reliability of the batteries.
Working Principle of the Powdered Electrolyte Powder Conveying System
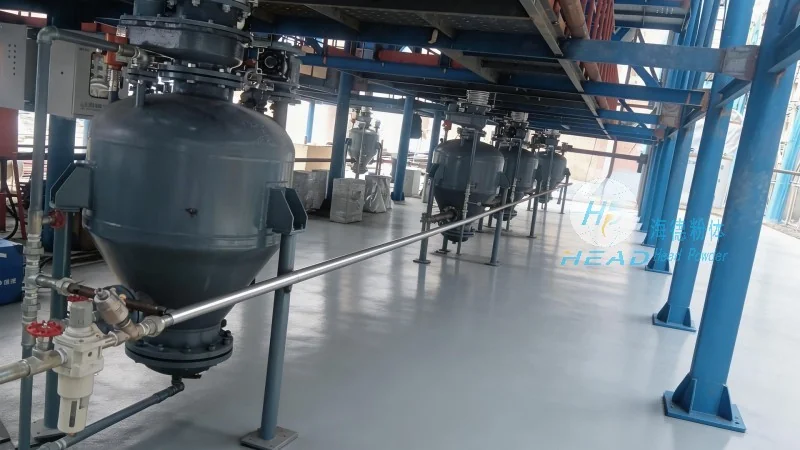
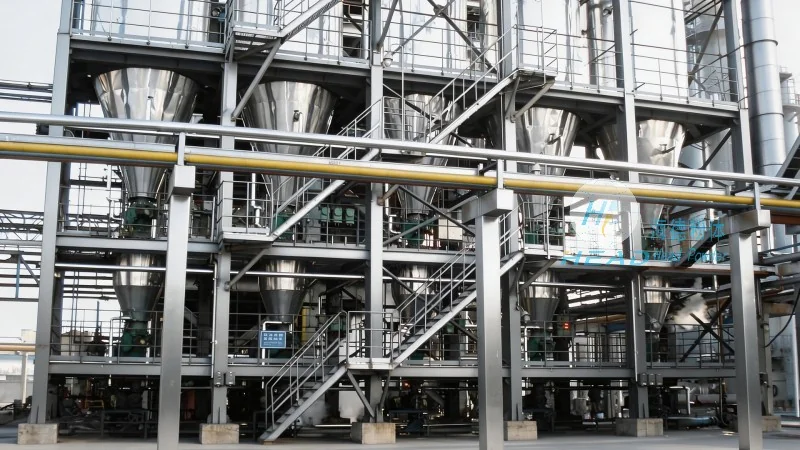
The core working principle of the system involves a series of interconnected components that work in tandem to move the electrolyte powder from the source to the destination. At the heart of the system is a hopper or storage container that holds the electrolyte powder. A feeding mechanism, often a rotary valve or a screw feeder, regulates the flow of powder into the conveyor pipeline. The conveyor itself may utilize pneumatic or mechanical methods to transport the powder. For example, pneumatic conveying systems use compressed air to create a flow of powder through a pipeline, while mechanical systems employ screws or belts to move the material. The system also includes control valves and sensors to monitor and adjust the flow rate, ensuring that the powder is conveyed at the optimal speed and pressure. The entire process is automated, with feedback loops that maintain consistent performance and prevent blockages or overloading. The system may also include a dust collection system to capture any airborne particles, ensuring a clean and safe working environment. Additionally, the system is equipped with temperature and humidity controls to maintain the optimal conditions for the electrolyte powder, preventing moisture absorption or degradation.
Key Features of the Powdered Electrolyte Powder Conveying System
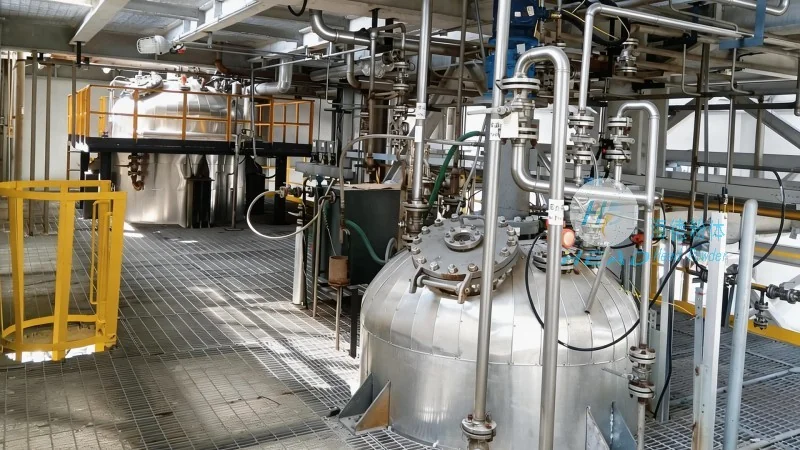
Several key features distinguish the powdered electrolyte powder conveying system from other conveying technologies. First, it offers high efficiency in material handling, with minimal product degradation due to gentle handling and low shear forces. The system is designed to maintain the integrity of the electrolyte powder, which is crucial for battery performance. Second, it provides precise control over the flow rate, allowing for accurate dosing and consistent quality control. This is achieved through advanced control systems that integrate sensors and actuators to adjust the conveyor speed and pressure in real-time. The system can deliver the powder at a consistent rate, even under varying load conditions, ensuring that the downstream processes receive a uniform feed. Third, the system is highly flexible and can be adapted to different production scales, from small-scale laboratory applications to large-scale industrial manufacturing. It can handle various powder types and particle sizes, making it versatile for different electrolyte formulations. For instance, it can handle fine powders with particle sizes as small as 1 micron, ensuring that no particles are lost during the conveying process. Fourth, the system is equipped with safety features to prevent dust explosions and ensure operator safety. These include explosion-proof designs, dust collection systems, and emergency shut-off mechanisms. The system may also include a fire suppression system to prevent the spread of fire in case of an accident. Finally, the system is easy to maintain and clean, with modular components that can be replaced or serviced without disrupting the entire production line. The system's design allows for quick disassembly and reassembly, reducing downtime and maintenance costs.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
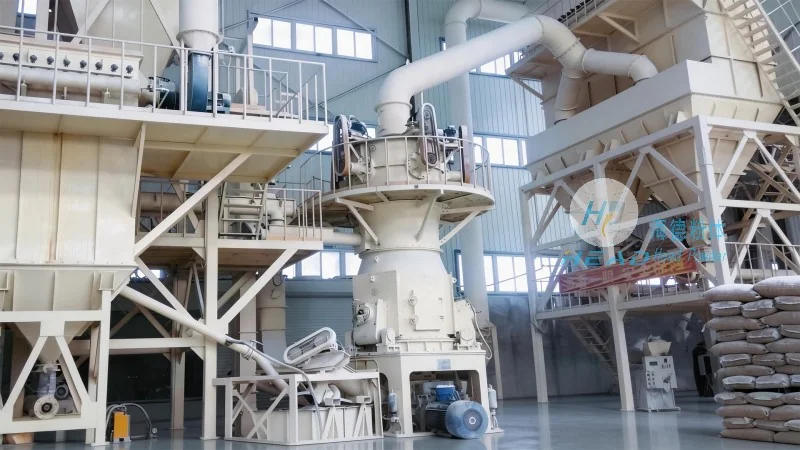
HeadPowder, the manufacturer of the powdered electrolyte powder conveying system, is a leading company in the field of powder handling technology. Based in Shandong, China, the company specializes in designing and manufacturing advanced conveying and processing systems for various industries. With years of experience and a team of skilled engineers, HeadPowder has developed a reputation for delivering high-quality, reliable products that meet international standards. The company's commitment to innovation and customer satisfaction has made it a trusted partner for many businesses in the battery and material processing sectors. HeadPowder's systems are known for their durability, efficiency, and ease of use, making them a preferred choice for companies looking to optimize their production processes. The company adheres to strict quality control standards, ensuring that each product is tested and validated before delivery. HeadPowder also provides comprehensive after-sales support, including installation, training, and technical assistance, to help customers maximize the performance of their systems. The company's research and development team continuously works on improving the technology, incorporating the latest advancements in powder handling to enhance the efficiency and reliability of the systems. HeadPowder's dedication to customer needs and technological excellence has positioned it as a key player in the global powder handling market.