

Working Principle and Characteristics of Ammonia Fertilizer Powder Conveying
Ammonia fertilizer, as a vital component in modern agricultural practices, demands efficient and reliable methods for powder handling and transport. The process of ammonia fertilizer powder conveying involves specialized systems engineered to manage the material's properties, such as its high reactivity and fine particle size. Understanding the working principle and key characteristics of these systems is essential for optimizing operational efficiency and ensuring safety in industrial applications.
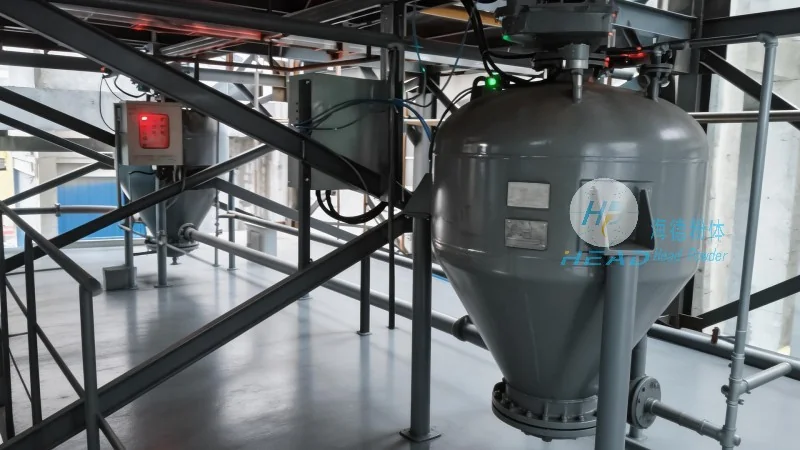
Working Principle of Ammonia Fertilizer Powder Conveying Systems
The core working principle of ammonia fertilizer powder conveying systems typically revolves around pneumatic or mechanical transport technologies. Pneumatic conveying systems utilize compressed air to move the powder through pipelines, proving highly effective for fine, dry powders like ammonia-based fertilizers. This method minimizes material degradation and contamination by suspending particles in air flow. The system generally includes a hopper for storage, a rotary valve or feeder to control flow rate, a conveying line with regulated air velocity, and a receiver for discharged material. Air flow is maintained at consistent velocity to ensure smooth transport without clogging or degradation.
Alternatively, mechanical conveying systems—such as screw or belt conveyors—may be employed for specific applications. Screw conveyors use a rotating screw to push material forward, while belt conveyors rely on a moving belt. Mechanical systems are often preferred in environments with air quality concerns or where dust generation is high. However, they may require more maintenance and are less suitable for highly reactive or fine powders compared to pneumatic systems.
Key Characteristics of Ammonia Fertilizer Powder Conveying Systems
Several critical characteristics define the performance and suitability of ammonia fertilizer powder conveying systems. One is the system's efficiency in material handling, enabling large volumes to be transported over long distances with minimal energy consumption and downtime—essential for industrial-scale operations seeking continuous production and reduced labor costs.
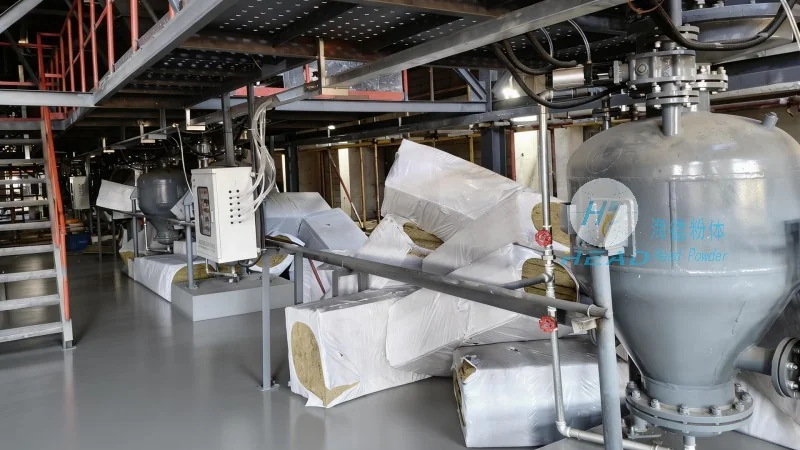
Another key characteristic is the system's ability to maintain material integrity and prevent contamination. Ammonia fertilizers are highly reactive and can degrade or react with moisture or air. Conveying systems incorporate sealed pipelines, moisture-resistant components, and air filtration to preserve material quality. This is vital for maintaining fertilizer effectiveness and preventing safety hazards like ammonia gas release.
Safety is a paramount consideration. Systems are designed to prevent dust explosions, achieved through explosion-proof components, proper ventilation, and safety protocols. Monitoring and control systems detect abnormalities (e.g., pressure fluctuations or blockages) to ensure safe, reliable operation.
Environmental considerations also play a role. Modern systems minimize emissions and noise pollution, with pneumatic systems using air filtration/recycling and mechanical systems incorporating sound-dampening materials. These features ensure compliance with environmental regulations and maintain a safe working environment.
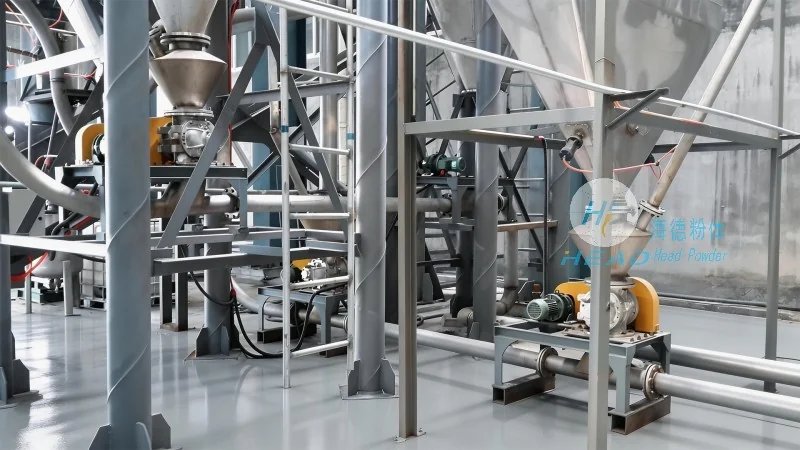
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized engineering solutions for powder handling and conveying systems. Focused on innovation and customer-centric design, HeadPowder has established itself as a trusted partner in agriculture and industry. The company specializes in developing customized solutions tailored to ammonia fertilizer production and transport, ensuring optimal performance, safety, and efficiency.
HeadPowder's commitment to quality and reliability is reflected in its state-of-the-art manufacturing facilities and rigorous testing processes. Adhering to international standards, the company ensures products meet the highest industry benchmarks. With experienced engineers and technicians, HeadPowder offers comprehensive support—from system design and installation to maintenance and troubleshooting. This approach delivers high-quality equipment and long-term solutions that enhance operational capabilities.
HeadPowder operates from Shandong, China, leveraging local resources and expertise to serve a global market. Its headquarters and manufacturing facilities are strategically located for efficient distribution and client support worldwide. By combining advanced technology with local knowledge, HeadPowder continues to deliver exceptional solutions for ammonia fertilizer powder conveying and other powder handling applications, advancing agricultural productivity and industrial efficiency.