

Working Principle and Features of Paper Chip Pneumatic Conveying Systems
When it comes to efficiently transporting paper chips, the pneumatic conveying system has emerged as a reliable and efficient solution. This technology, developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, offers a comprehensive approach to material handling in various industrial applications.
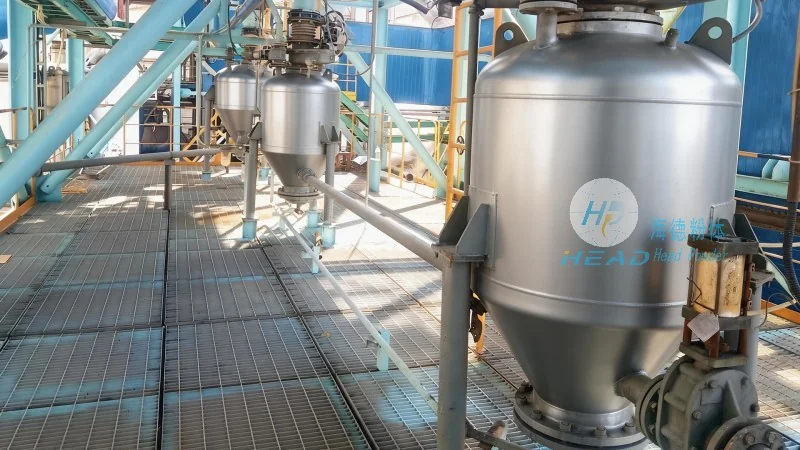
Understanding the Working Principle of Paper Chip Pneumatic Conveying Systems
The core of a paper chip pneumatic conveying system lies in its ability to transport bulk materials through a pressurized or vacuum environment. The system typically consists of a hopper for material storage, a conveyor line, and a control unit. As paper chips are fed into the hopper, they are drawn into the conveyor line by a fan or blower. The air flow, either under pressure or suction, moves the chips along the pipeline to the desired destination. This process eliminates the need for mechanical components like belts or chains, reducing maintenance and operational costs.
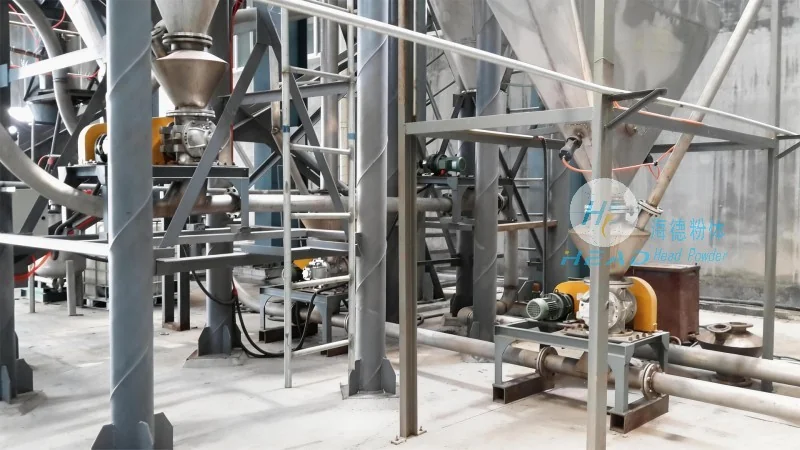
Key Features of the Paper Chip Pneumatic Conveying System
Shandong HeadPowder Engineering Co., Ltd. has designed the paper chip pneumatic conveying system with several distinct features that enhance its performance and adaptability. Firstly, the system is highly flexible, allowing for horizontal, vertical, or inclined transport routes. This flexibility enables it to fit into existing industrial layouts without major modifications. Secondly, it offers excellent material handling capabilities, ensuring minimal product degradation and consistent flow rates. The system also incorporates advanced control mechanisms that monitor air pressure, flow rate, and material level, providing real-time feedback and preventing system failures. Additionally, the design prioritizes energy efficiency, with optimized air consumption and reduced power usage compared to traditional conveying methods.
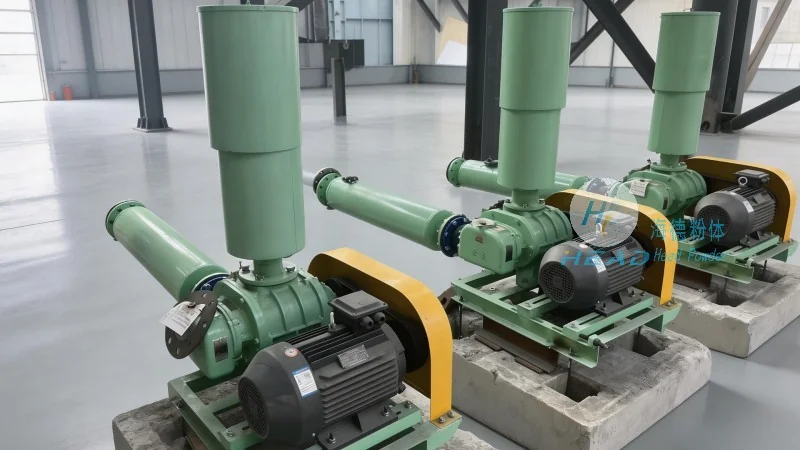
Benefits of Implementing a Paper Chip Pneumatic Conveying System
Adopting a paper chip pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. brings numerous advantages to industrial operations. The primary benefit is the significant reduction in labor costs, as the system automates the entire material transport process. It also minimizes the risk of material contamination and damage, which is crucial for maintaining product quality. Furthermore, the system enhances workplace safety by eliminating manual handling of heavy or bulky paper chips. From an operational standpoint, the system offers high reliability and low downtime, ensuring continuous production. The energy efficiency of the system also contributes to lower operational expenses and a reduced environmental footprint.
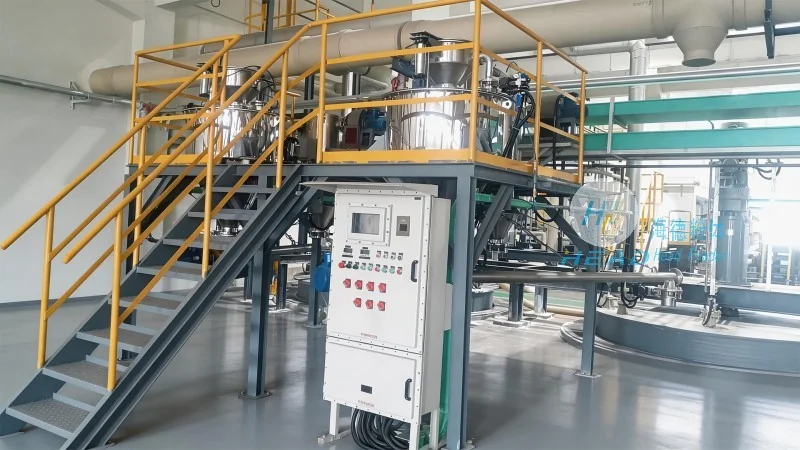
Customization and Application Scope
Shandong HeadPowder Engineering Co., Ltd. understands that different industrial settings have unique requirements. Therefore, the paper chip pneumatic conveying system is available in various configurations to suit specific needs. Whether for small-scale paper processing plants or large-scale manufacturing facilities, the system can be customized in terms of pipeline length, material capacity, and control features. The system is widely used in paper mills, where it efficiently transports raw paper chips from storage to processing units. It is also applicable in recycling facilities, where it handles recycled paper materials. The versatility of the system makes it suitable for a range of applications where efficient and clean material transport is essential.