

[Cereal Dregs Pneumatic Conveying: Types, Features, and Application Scope]
As a specialized manufacturer in the field of material handling equipment, Shandong HeadPowder Engineering Co., Ltd. has been committed to providing efficient and reliable solutions for the transportation of cereal dregs. Cereal dregs, also known as bran or bran residue, are byproducts generated during the processing of grains such as wheat, barley, and rice. These materials are often characterized by their high moisture content, irregular shapes, and abrasive properties, making traditional conveying methods less effective and potentially damaging to equipment. Pneumatic conveying systems have emerged as a superior alternative for handling cereal dregs, offering advantages in terms of hygiene, flexibility, and energy efficiency.
Types of Cereal Dregs Pneumatic Conveying Systems
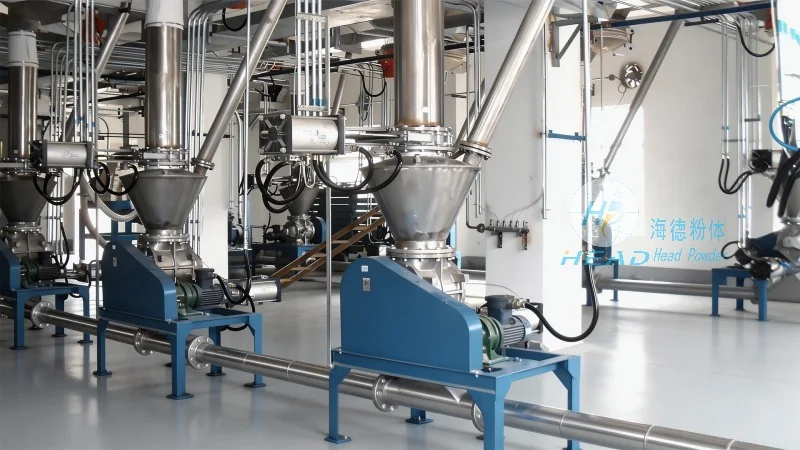
There are primarily two types of pneumatic conveying systems used for cereal dregs: dilute-phase and dense-phase systems. Dilute-phase systems operate by suspending the material in a high-velocity air stream, allowing for long-distance transport with minimal pressure drops. This type is suitable for applications where the material is relatively dry and free-flowing. Dense-phase systems, on the other hand, use lower air velocities and higher material concentrations, resulting in a more controlled and gentle transport process. This method is ideal for handling materials that are more abrasive or have higher moisture content, as it reduces the risk of product degradation and equipment wear.
Key Features of Cereal Dregs Pneumatic Conveying
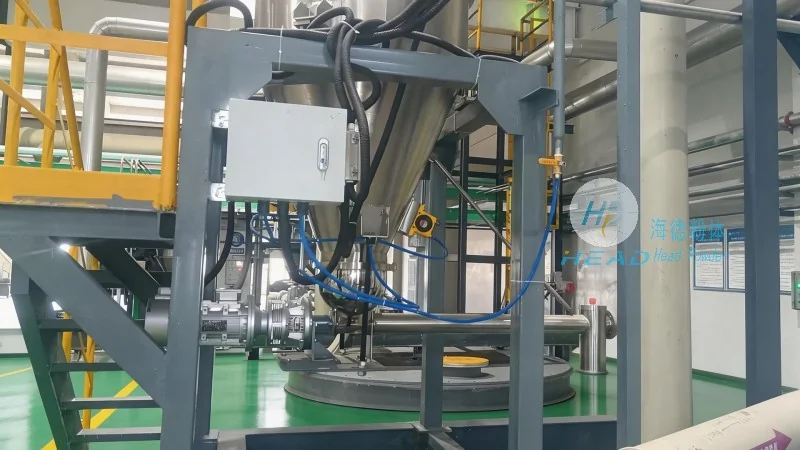
Efficient and hygienic material handling is a critical feature of cereal dregs pneumatic conveying systems. The enclosed design of these systems prevents dust and contaminants from entering the environment, ensuring compliance with food safety regulations. Additionally, the systems are designed to minimize product degradation, preserving the nutritional value and quality of the cereal dregs. Another notable feature is the flexibility in system configuration, allowing for integration with existing production lines or expansion as production needs grow. The use of high-quality materials and robust construction ensures long service life and low maintenance costs, contributing to overall operational efficiency.
Application Scope of Cereal Dregs Pneumatic Conveying
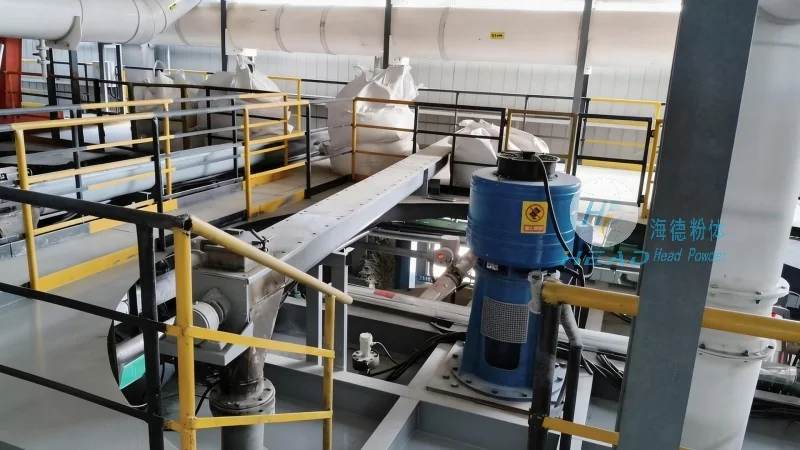
The application scope of cereal dregs pneumatic conveying systems is broad and encompasses various industries. In the food processing sector, these systems are widely used in flour mills, breweries, and grain processing plants to transport bran and other byproducts to storage silos or processing units. The systems are also employed in the animal feed industry, where cereal dregs are used as a valuable ingredient in feed formulations. Furthermore, in the biofuel and renewable energy sectors, pneumatic conveying is utilized to transport dregs to biogas production facilities or composting sites. The versatility of these systems allows them to adapt to different production scales, from small-scale operations to large industrial plants, making them a preferred choice for efficient material handling in multiple applications.

Benefits of Choosing Shandong HeadPowder Engineering Co., Ltd.
When selecting a pneumatic conveying system for cereal dregs, it is essential to partner with a reputable manufacturer that understands the unique challenges of handling these materials. Shandong HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, specializes in designing and manufacturing customized pneumatic conveying solutions tailored to the specific needs of clients. The company’s expertise in material handling technology ensures that the systems are optimized for the characteristics of cereal dregs, such as moisture content, particle size, and abrasiveness. By choosing HeadPowder, clients benefit from advanced engineering, rigorous quality control, and comprehensive after-sales support, ensuring reliable and efficient operation of the conveying systems. The company’s commitment to innovation and customer satisfaction has established it as a leading provider in the industry, delivering solutions that enhance productivity and reduce operational costs.