

Design of a Negative Pressure Pneumatic Conveying System for Manganese Carbonate
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. This article focuses on the development of a negative pressure pneumatic conveying system specifically tailored for the transportation of manganese carbonate, a critical component in various industrial applications.
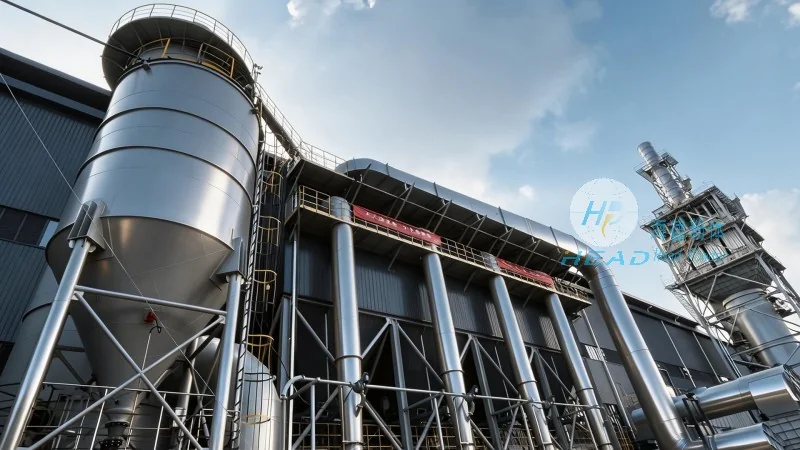
Overview of the Negative Pressure Pneumatic Conveying System
The negative pressure pneumatic conveying system is engineered to efficiently transport manganese carbonate from storage silos or production lines to processing units. By utilizing a vacuum environment, the system ensures minimal product degradation and optimal control over the conveying process. This design addresses the unique challenges associated with handling fine powders like manganese carbonate, which are prone to dust generation and require precise flow management.
Key Components and Their Functions
The system comprises several critical components, each playing a vital role in ensuring reliable operation. The primary elements include a vacuum pump, a conveying line, a hopper for material storage, and a filter system to capture any airborne particles. The vacuum pump creates the necessary negative pressure, drawing the manganese carbonate powder through the conveying line. The hopper is designed with a smooth interior to prevent material buildup and facilitate consistent feeding. The filter system is crucial for maintaining air quality and preventing dust contamination in the surrounding environment.
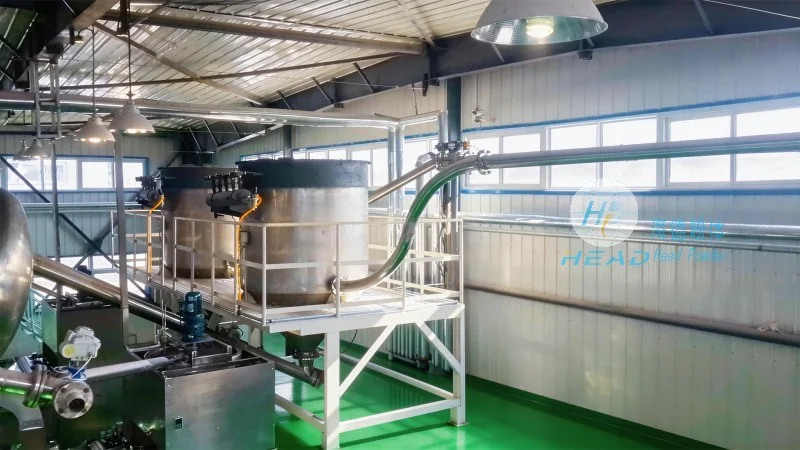
Material Handling Efficiency and Process Control
Efficiency is a key consideration in the design of this system. The negative pressure approach minimizes the risk of product loss and spillage, which is particularly important for manganese carbonate due to its industrial applications. The system allows for precise control over the flow rate, ensuring that the material is conveyed at the optimal speed to prevent clogging or degradation. This control is achieved through adjustable valves and pressure sensors that monitor the system's performance in real-time. The result is a consistent and reliable material transfer process that meets the demands of modern industrial operations.
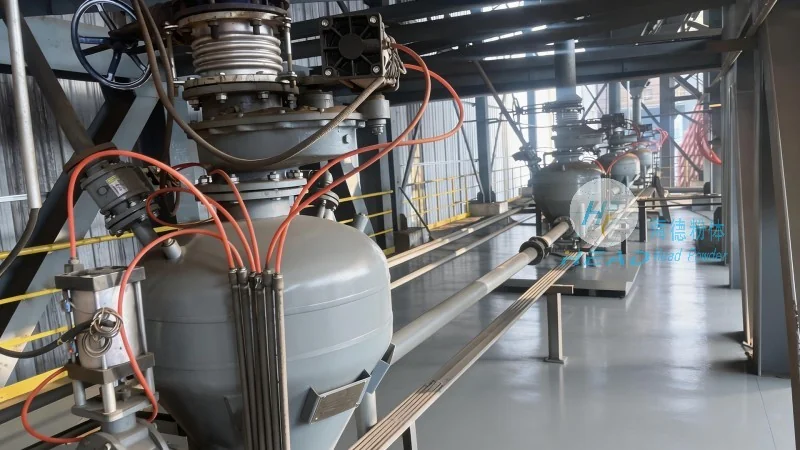
Industrial Applications and Benefits
Manganese carbonate is widely used in the production of batteries, steel, and other chemical products. The negative pressure pneumatic conveying system is particularly suitable for these applications due to its ability to handle fine powders without compromising product quality. The system's benefits extend beyond efficiency, as it also reduces labor costs associated with manual handling and minimizes environmental impact by containing dust within the system. Additionally, the design allows for easy integration with existing production lines, making it a cost-effective solution for companies looking to upgrade their material handling capabilities.
Conclusion
HeadPowder's negative pressure pneumatic conveying system for manganese carbonate represents a sophisticated solution to the challenges of material handling in industrial settings. By combining advanced engineering principles with practical design considerations, the system ensures efficient, reliable, and safe transportation of the material. As a company with a strong presence in Shandong, China, HeadPowder continues to innovate in the field of material handling, providing tailored solutions that meet the specific needs of its clients. The success of this system underscores the company's commitment to quality and excellence in engineering.