

Principle and Working Scene Characteristics of Ammonium Bicarbonate Material Pneumatic Conveying Mac
Ammonium bicarbonate, a widely used chemical in industries such as agriculture and food processing, requires efficient and reliable material handling solutions to ensure smooth production workflows. The pneumatic conveying machine for ammonium bicarbonate is a specialized equipment designed to transport this material through an air-driven system, offering advantages over traditional methods like belt conveyors or bucket elevators.
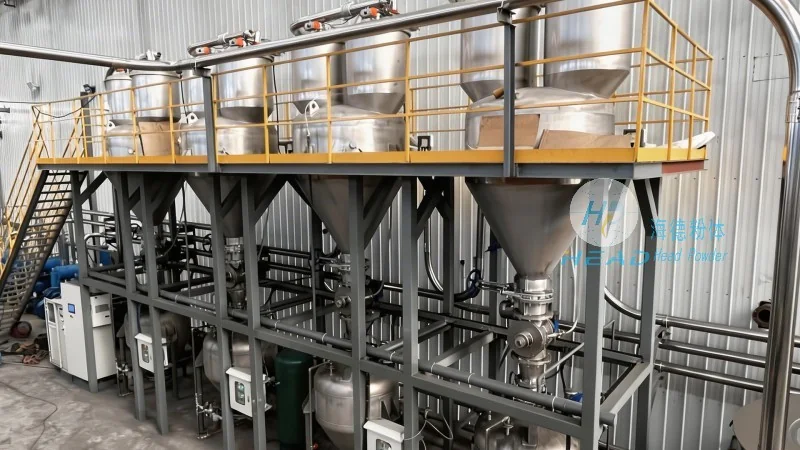
Principle of Pneumatic Conveying for Ammonium Bicarbonate
The core principle of the ammonium bicarbonate pneumatic conveying machine lies in the use of compressed air or suction to move the material particles through a pipeline. This system typically operates under either positive pressure (where air is forced into the pipeline) or negative pressure (where air is drawn out). For ammonium bicarbonate, which is a fine powder with a relatively low bulk density, positive pressure systems are often preferred as they provide better control over the material flow and reduce the risk of clogging. The machine consists of a hopper, a conveyor line, and a discharge mechanism. The hopper holds the ammonium bicarbonate, and when the system is activated, air is introduced into the conveyor line, creating a flow that carries the material from the source to the destination. The design of the hopper and the air distribution system is critical to ensure uniform material feeding and prevent agglomeration, which can lead to blockages in the pipeline.
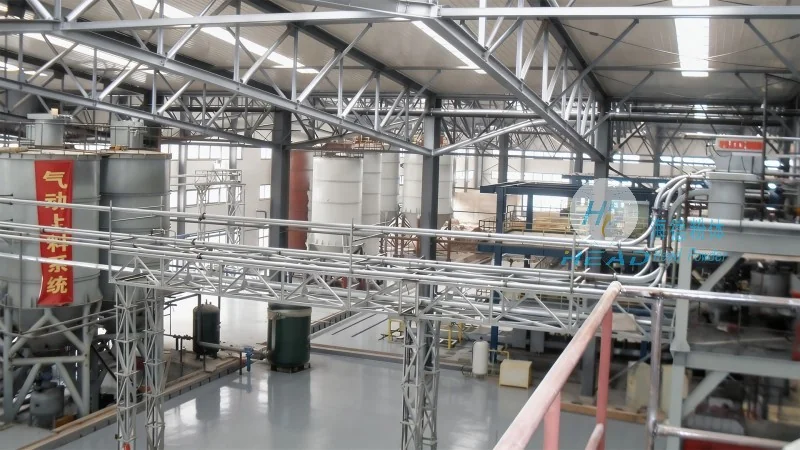
Working Scene Characteristics and Applications
The working scene characteristics of the ammonium bicarbonate pneumatic conveying machine are tailored to the specific needs of industrial environments where this chemical is processed. In agricultural applications, for example, the machine is used to transport ammonium bicarbonate from storage silos to fertilizer blending plants or packaging lines. The key characteristics include high efficiency in handling fine powders, minimal material loss during transport, and the ability to operate in clean environments, which is essential for maintaining product quality and compliance with industry standards. In the food processing industry, the machine is employed to move ammonium bicarbonate from production lines to storage or packaging areas, ensuring that the material remains free from contamination and is delivered to the next stage of processing without degradation. The system's ability to handle large volumes of material quickly and with minimal human intervention makes it ideal for high-throughput production lines. Additionally, the machine's design allows for easy integration with existing production equipment, reducing the need for extensive modifications to the facility. The working scene also includes considerations for safety and maintenance, as the system operates under pressure and requires regular checks to prevent leaks or malfunctions.
Advantages of Using Pneumatic Conveying for Ammonium Bicarbonate
Compared to traditional material handling methods, the pneumatic conveying machine for ammonium bicarbonate offers several advantages that make it a preferred choice for many industries. One of the most significant benefits is the reduction in material degradation, as the enclosed system prevents exposure to air, moisture, or other contaminants that can affect the quality of the ammonium bicarbonate. This is particularly important for a chemical that is sensitive to environmental factors. Another advantage is the ability to transport material over long distances without the need for multiple transfer points, which can reduce operational costs and improve overall efficiency. The system also provides better control over the material flow rate, allowing for precise dosing and mixing, which is crucial in processes like fertilizer manufacturing. Furthermore, the pneumatic conveying machine is more hygienic and easier to clean compared to other equipment, which is essential in food and pharmaceutical applications where cleanliness is paramount. The low maintenance requirements of the system, combined with its durability, make it a cost-effective solution for long-term use.
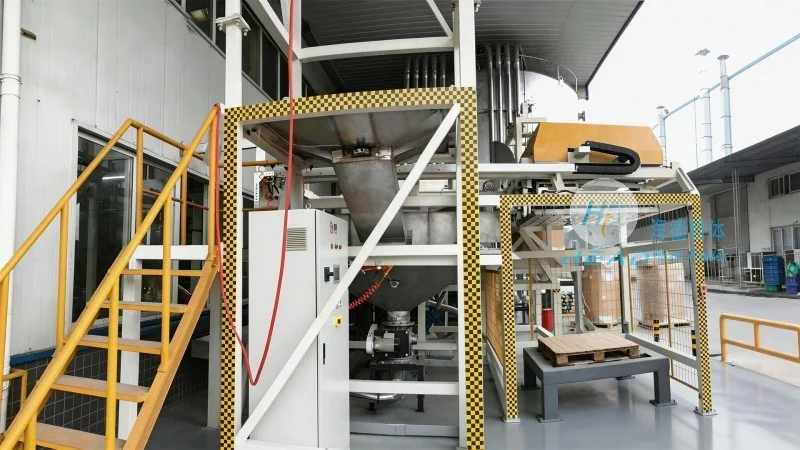
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of specialized material handling equipment, including pneumatic conveying systems for various chemical and industrial applications. With a focus on innovation and quality, the company has established itself as a trusted partner in the industry, providing customized solutions that meet the unique needs of its clients. Headpowder's facilities are located in Shandong, China, where the company leverages advanced manufacturing technologies and a skilled workforce to produce high-performance equipment. The company's commitment to research and development ensures that its products remain at the forefront of technological advancements, offering reliable and efficient solutions for material handling challenges. By combining expertise in engineering, manufacturing, and customer service, headpowder delivers solutions that enhance productivity, reduce costs, and improve safety in industrial operations. The company's reputation for excellence and reliability has made it a preferred choice for businesses seeking to optimize their material handling processes.