

Principle and Working Scene Characteristics of Powder Silo Powder Conveying System Equipment
HeadPowder, a leading provider in the field, specializes in advanced powder silo conveying systems designed to optimize material handling efficiency. These systems are engineered to address the unique challenges of transporting bulk powders, ensuring consistent performance and reliability in industrial applications.
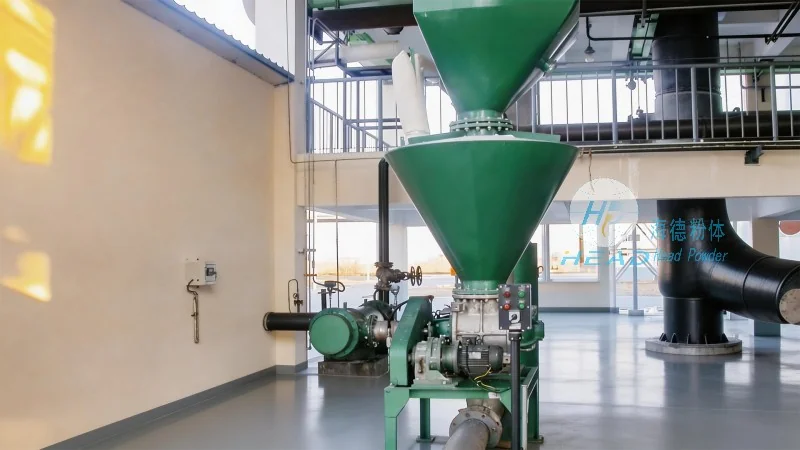
Core Principles of the Conveying System
The fundamental principle of the powder silo conveying system lies in its ability to handle fine or cohesive powders with precision. By integrating advanced pneumatic or mechanical components, the system maintains material integrity while minimizing degradation or segregation. Key to its operation is the controlled pressure and flow management, which ensures smooth transfer from the silo to downstream processes. The design incorporates features such as airtight sealing and adjustable speed controls, allowing for customization based on the specific characteristics of the powder being handled.
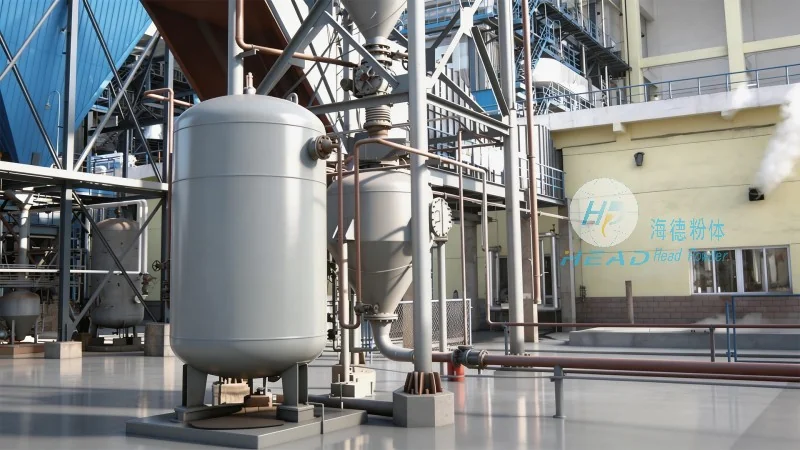
Working Scene Characteristics and Applications
The working scene characteristics of HeadPowder's powder silo conveying systems are tailored to diverse industrial environments. These systems are commonly employed in sectors like pharmaceuticals, food processing, and chemical manufacturing, where maintaining product purity and preventing contamination is critical. In pharmaceutical applications, for instance, the system’s sterile design and contamination control measures ensure compliance with stringent regulatory standards. Similarly, in food processing, the hygienic construction and easy-to-clean components meet the high sanitary requirements of the industry. The versatility of the system also makes it suitable for handling various types of powders, including fine chemicals, agricultural products, and industrial raw materials, adapting to different particle sizes and flow properties.
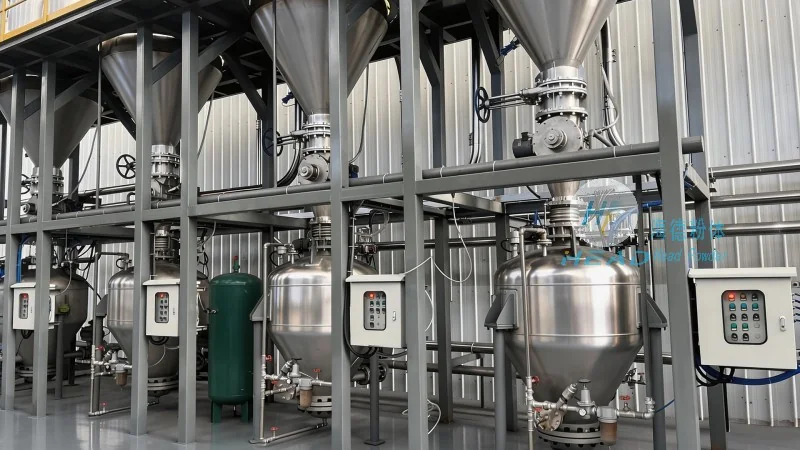
Technical Advantages and Performance
HeadPowder’s powder silo conveying systems offer several technical advantages that enhance operational efficiency. The system’s compact design reduces space requirements, making it ideal for facilities with limited floor space. Additionally, the energy-efficient operation minimizes operational costs while maintaining high throughput rates. The advanced control systems provide real-time monitoring of flow rates and pressure, enabling operators to adjust settings dynamically for optimal performance. Furthermore, the system’s durability and low maintenance requirements contribute to long-term cost savings, as it requires minimal downtime for repairs or servicing.
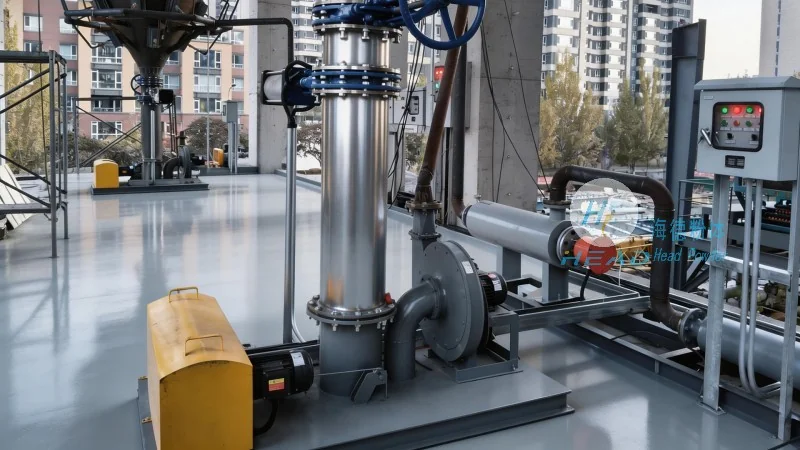
Company Background and Commitment
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, has established itself as a trusted manufacturer of high-quality material handling solutions. With a strong focus on research and development, the company continuously innovates to meet the evolving needs of its clients. The company’s commitment to quality is reflected in its adherence to international standards and rigorous testing protocols. By leveraging local expertise and global best practices, HeadPowder ensures that its products meet the highest industry benchmarks, providing reliable and efficient solutions for powder handling challenges.