

Working Principle and Features of Sugar Material Handling Systems
Efficient and reliable sugar material handling systems are crucial for modern sugar processing facilities. These systems ensure smooth material flow from storage to processing units, enhancing overall operational efficiency and product quality. Understanding the working principle and key features of such systems is essential for optimizing production processes in the sugar industry.
Working Principle of Sugar Material Handling Systems
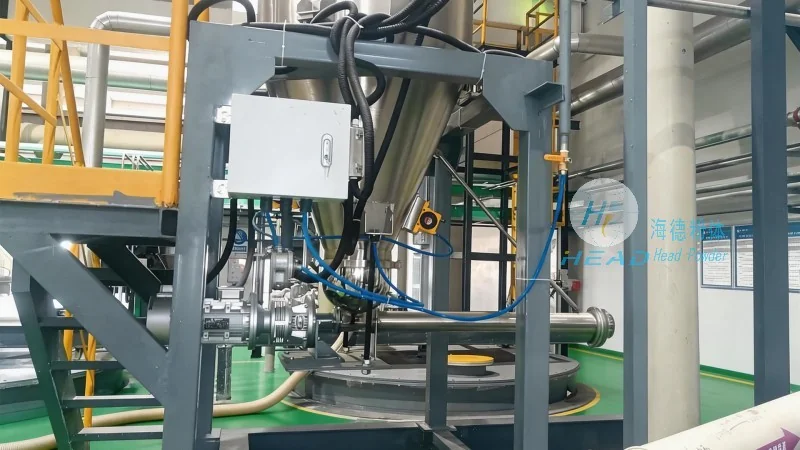
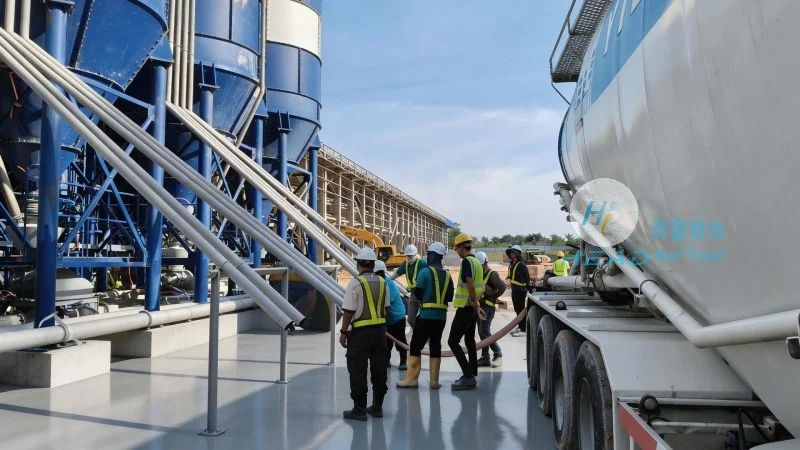
Sugar material handling systems typically operate through a combination of mechanical and automated components designed to transport raw sugar, refined sugar, or other sugar-related materials. The core working principle involves the use of conveyor belts, elevators, and pneumatic conveyors to move bulk materials in a controlled manner. These systems often start with material storage in silos or hoppers, where the sugar is held before being transferred to processing equipment. The initial step includes feeding mechanisms that regulate the flow of sugar into the conveyor system. From there, the material is transported horizontally or vertically, depending on the layout of the processing plant. Pneumatic conveyors may use air pressure to move sugar particles through pipes, while mechanical conveyors rely on rollers or belts to carry the load. The system concludes with discharge mechanisms that deliver the sugar to the next stage of processing, such as refining or packaging. This integrated approach ensures a continuous and efficient flow of sugar throughout the production line.
Key Features of Sugar Material Handling Systems
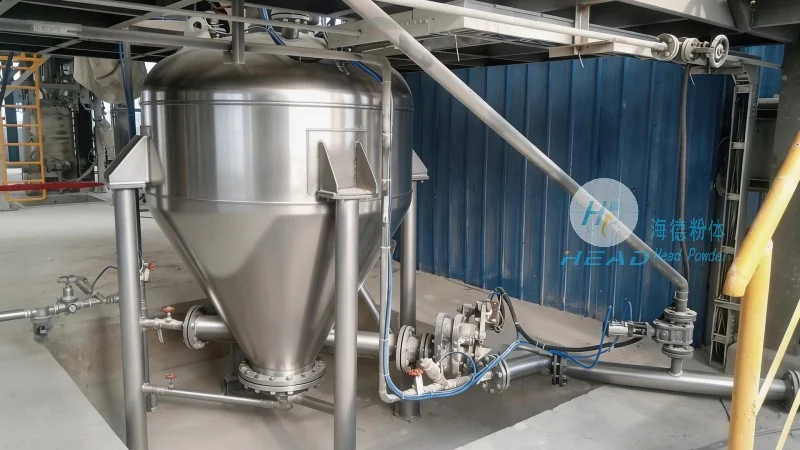
Modern sugar material handling systems are characterized by several key features that enhance their performance and adaptability. One of the primary features is the ability to handle various sugar types, including raw cane sugar, beet sugar, and refined white sugar, without causing degradation or contamination. The systems are designed with hygienic materials, such as stainless steel, to meet industry standards for food processing. Another important feature is the integration of automation and control systems, which allow for real-time monitoring and adjustment of the material flow. This automation reduces human error and increases operational consistency. Additionally, the systems are equipped with safety features, including emergency stop buttons and overload protection, to ensure safe operation in industrial environments. The modular design of these systems enables easy expansion or modification to accommodate changes in production volume or processing requirements. Energy efficiency is also a key consideration, with many systems incorporating variable speed drives to optimize power consumption. These features collectively contribute to the reliability, efficiency, and adaptability of sugar material handling systems in modern sugar processing operations.
About Shandong HeadPowder Engineering Co., Ltd.
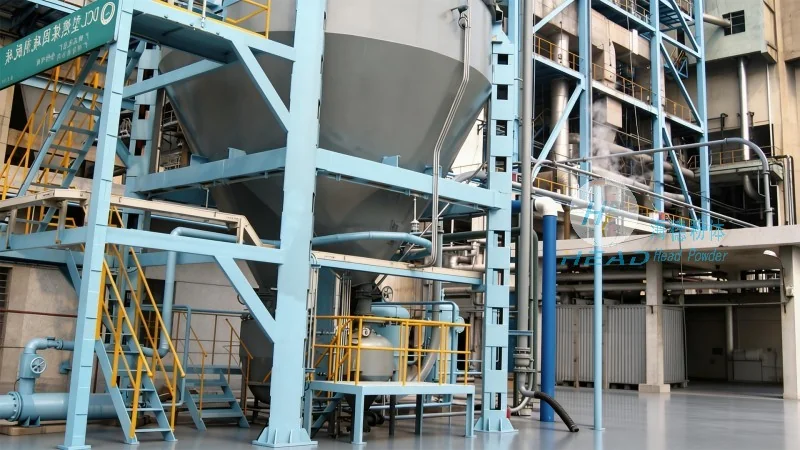
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer of specialized material handling solutions for the sugar industry. With a strong presence in China, the company has established itself as a trusted provider of high-quality equipment tailored to the unique needs of sugar processing facilities. The company's expertise lies in designing and manufacturing systems that enhance operational efficiency, ensure product quality, and meet industry standards. By leveraging advanced engineering and manufacturing capabilities, headpowder delivers customized solutions that address the specific challenges faced by sugar producers. The company's commitment to innovation and customer satisfaction has earned it a reputation for reliability and excellence in the industry. With a focus on quality and performance, headpowder continues to serve as a key partner for sugar processing companies seeking to optimize their material handling processes.