

Working Principle and Features of Rare Earth Powder Pneumatic Conveying Equipment
Understanding the working principle and features of rare earth powder pneumatic conveying equipment is crucial for industries dealing with these specialized materials. This equipment is designed to efficiently transport rare earth powders through a pneumatic system, offering a reliable solution for material handling in various applications.
Working Principle of Rare Earth Powder Pneumatic Conveying Equipment
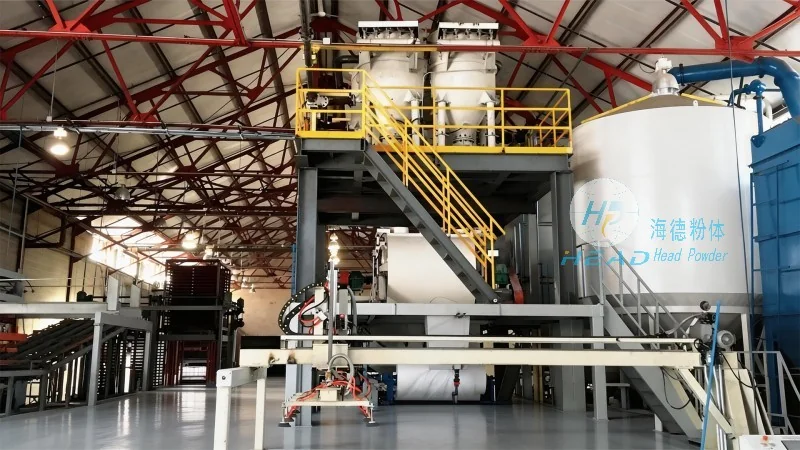
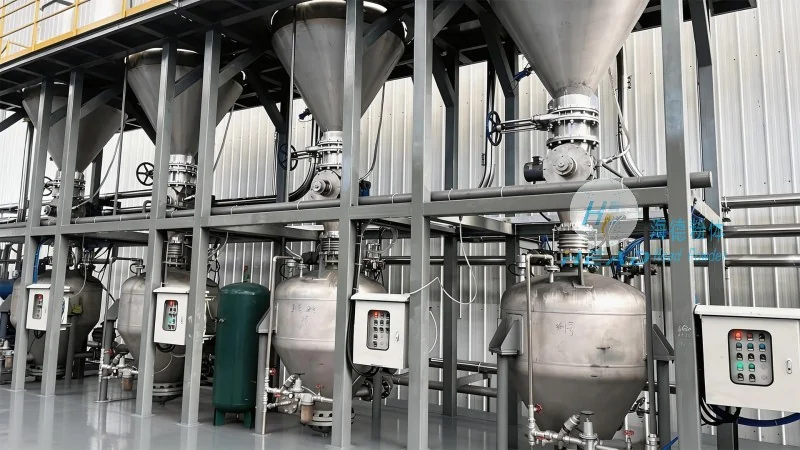
The working principle of rare earth powder pneumatic conveying equipment revolves around the fundamental concept of using air as a medium to transport solid particles. In this system, the rare earth powder is introduced into a hopper or feeder, where it is then drawn into a conveying pipeline by a vacuum or pressure source. The vacuum system creates a negative pressure that pulls the powder and air mixture through the pipeline, while the pressure system uses positive pressure to push the mixture forward. The choice between vacuum and pressure modes depends on factors such as the distance to be covered, the particle size of the powder, and the desired flow rate. For longer distances or larger particle sizes, a pressure system may be more effective, as it can maintain higher air velocities to prevent particle settling. Conversely, vacuum systems are often preferred for shorter distances or when the material needs to be transported from a lower to a higher elevation. The conveying line is typically made of materials like stainless steel or plastic, which are resistant to corrosion and wear from the rare earth powder. The system also includes components such as filters and cyclones to separate the powder from the air at the receiving end, ensuring that the material is collected in a clean and dry state. This separation process is crucial for maintaining the purity of the rare earth powder, which is often used in high-tech applications where contamination is unacceptable.
Key Features of Rare Earth Powder Pneumatic Conveying Equipment
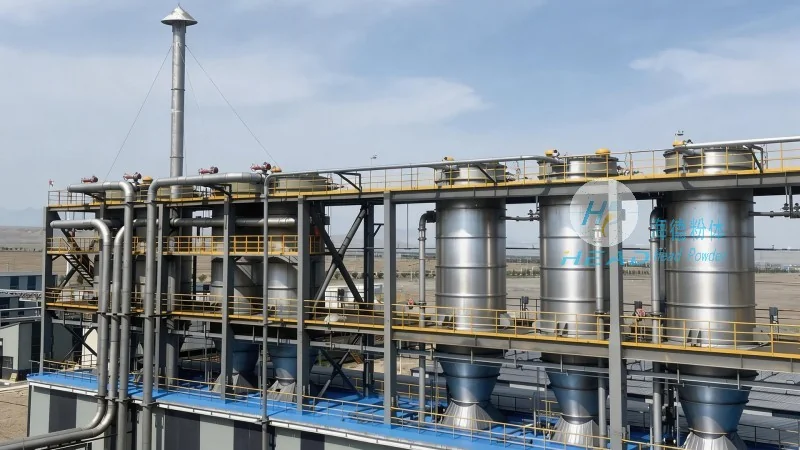
Several key features distinguish rare earth powder pneumatic conveying equipment from other material handling solutions, making it particularly suitable for handling these specialized powders. One of the most important features is its ability to handle fine and abrasive particles without causing excessive wear or clogging. The equipment is designed with smooth internal surfaces and appropriate pipe diameters to minimize friction and particle agglomeration. This is critical for rare earth powders, which often have a high specific gravity and can be prone to sticking together. The system also incorporates advanced control mechanisms that allow for precise regulation of air flow and pressure, ensuring consistent material transport. These controls can be automated, providing real-time monitoring and adjustment to maintain optimal performance. Another notable feature is the system's flexibility, as it can be configured to handle different types of rare earth powders, including those with varying moisture content or chemical properties. The equipment can also be integrated with other processing equipment, such as mixing or drying units, to form a complete production line. Additionally, the design emphasizes safety and environmental compliance, with features like dust suppression systems and emergency shutdown capabilities. These features not only protect the operators and the environment but also help in meeting regulatory requirements, which is essential for industries dealing with rare earth materials.
Company Information: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a prominent entity in the material handling industry, specializes in the design, manufacturing, and supply of pneumatic conveying equipment tailored for the unique needs of the rare earth sector. The company, operating from Shandong, China, leverages decades of experience and cutting-edge technology to deliver high-performance solutions that enhance operational efficiency and product quality. HeadPowder's product portfolio includes a range of rare earth powder pneumatic conveying systems, each engineered to handle specific challenges such as high particle density, fine particle size, and potential reactivity. The company's manufacturing facility is equipped with advanced machinery and quality control systems, ensuring that every piece of equipment meets stringent industry standards. HeadPowder's commitment to customer satisfaction is reflected in its comprehensive after-sales support, including installation, maintenance, and technical assistance. By partnering with HeadPowder, businesses can benefit from reliable equipment that minimizes downtime and maximizes productivity, ultimately contributing to their success in the competitive rare earth market. The company's presence in Shandong, a key industrial region in China, positions it to serve a wide range of clients across the country and beyond, with a focus on delivering sustainable and efficient material handling solutions.