

What is a Pneumatic Pulse Powder Conveying System? And What Are Its Design Principles?
A pneumatic pulse powder conveying system is a specialized industrial equipment designed to transport bulk powder materials through a pipeline using compressed air. This technology is widely used in various industries such as food processing, pharmaceuticals, chemicals, and mining, where efficient and reliable powder handling is crucial. The system operates by creating a pressure differential that propels the powder particles through the pipeline, ensuring a consistent and controlled flow.
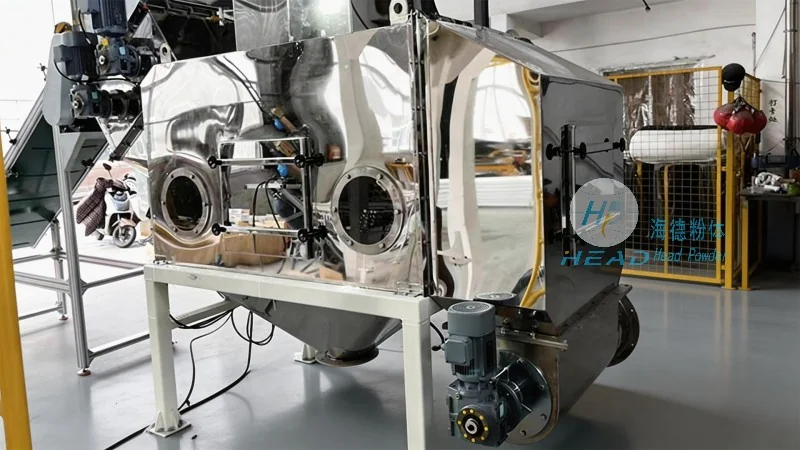
HeadPowder: A Leading Manufacturer of Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a reputable company based in Shandong, China. With years of experience in the field, HeadPowder specializes in the design, manufacturing, and supply of high-quality pneumatic conveying systems. The company's commitment to innovation and customer satisfaction has made it a trusted partner for businesses seeking reliable powder handling solutions. HeadPowder's products are engineered to meet the diverse needs of different industries, offering flexibility and efficiency in powder transportation.
The Design Principles of Pneumatic Pulse Conveying Systems
The core design principle of a pneumatic pulse powder conveying system is the use of compressed air to create a pulse or pressure wave that moves the powder through the pipeline. This method, known as pulse conveying, involves periodic bursts of air that displace the powder particles, preventing clogging and ensuring smooth operation. The system typically consists of several key components, including a hopper for material storage, a pulse generator to control the air pressure, a pipeline network for material transport, and a receiver for the discharged powder. Each component plays a critical role in the overall performance of the system.
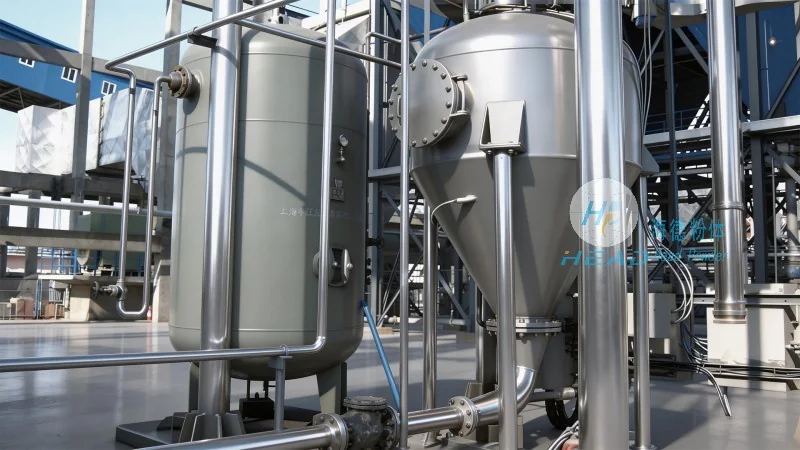
Key Components and Their Functions
1. **Hopper**: The hopper is the initial storage unit where the bulk powder is placed. It is designed to maintain a consistent material level and prevent material bridging or segregation. The hopper is equipped with a discharge valve that allows the powder to flow into the pipeline when needed.
2. **Pulse Generator**: The pulse generator is a critical component that controls the frequency and duration of the air pulses. It regulates the pressure in the pipeline, ensuring that the powder is propelled at an optimal speed without causing excessive wear or pressure buildup. The generator can be adjusted to accommodate different powder types and pipeline lengths.
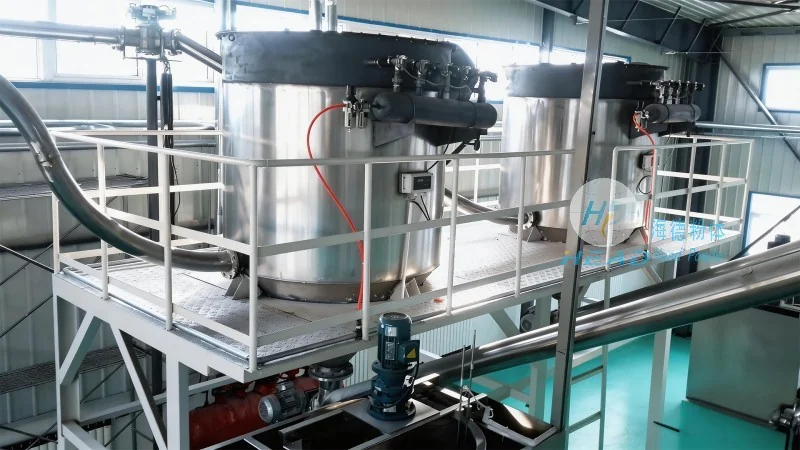
3. **Pipeline Network**: The pipeline network is the main transport channel for the powder. It is usually made of materials such as stainless steel or plastic, which are resistant to corrosion and wear from the powder particles. The pipeline is designed with appropriate bends and fittings to minimize pressure loss and maintain the flow of the material.
4. **Receiver**: The receiver is the final component where the conveyed powder is collected. It is equipped with a discharge valve or a conveyor system to transfer the powder to the next processing stage. The receiver is designed to prevent dust emissions and ensure a clean and safe working environment.
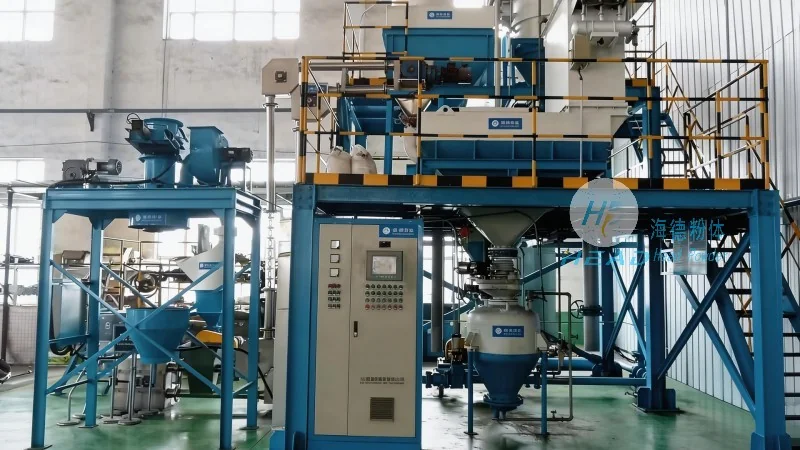
Advantages of Pneumatic Pulse Conveying Systems
Compared to traditional mechanical conveying methods, pneumatic pulse powder conveying systems offer several advantages. First, they are highly flexible and can be easily integrated into existing production lines. The system can be modified to accommodate changes in production volume or material type without significant modifications. Second, the system is capable of handling a wide range of powder materials, including fine, abrasive, and sticky powders. Third, the operation is relatively simple and requires minimal maintenance. The system can be automated to operate continuously, reducing labor costs and increasing productivity. Finally, the system is more hygienic and cleaner compared to mechanical systems, which is particularly important in industries such as food and pharmaceuticals.
Applications in Different Industries
Pneumatic pulse powder conveying systems are used in various industries due to their versatility and efficiency. In the food industry, the system is used to transport ingredients such as flour, sugar, and spices. In the pharmaceutical industry, it is used to transport active pharmaceutical ingredients (APIs) and excipients. In the chemical industry, it is used to transport chemicals and raw materials. In the mining industry, it is used to transport ore and minerals. The system's ability to handle different powder types and its hygienic design make it suitable for these applications.