

Design of Fly Ash Particle Pneumatic Conveying System
At Shandong HeadPowder Engineering Co., Ltd., we specialize in the design and implementation of advanced pneumatic conveying systems tailored for the efficient handling of fly ash particles. Our expertise lies in creating customized solutions that meet the specific operational requirements of industrial clients, ensuring optimal performance and reliability in material transport processes.
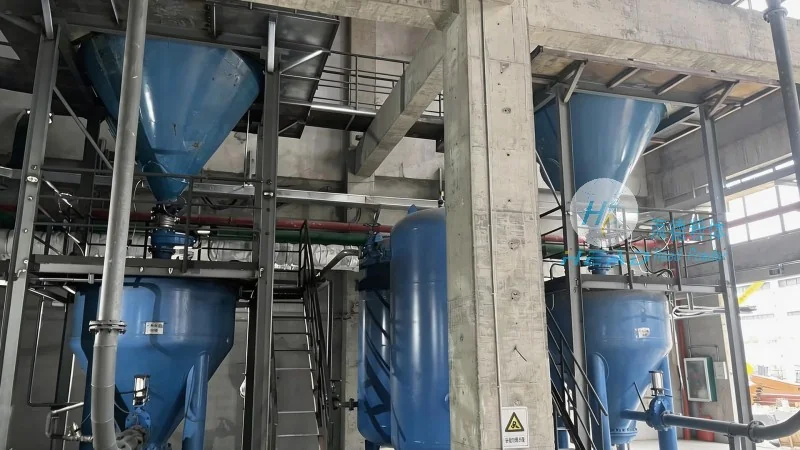
System Design Principles and Key Components
Our fly ash particle pneumatic conveying system design incorporates a comprehensive approach that addresses the unique challenges associated with transporting fine particulate materials like fly ash. The system is engineered to maintain consistent flow rates, minimize material degradation, and reduce operational downtime. Key components include high-efficiency air compressors, specialized conveying pipes, and advanced control systems that regulate pressure and airflow dynamics. These elements work in tandem to ensure seamless material transfer from source to destination, whether for storage, processing, or disposal applications.
Material Handling Efficiency and System Flexibility
The design of our pneumatic conveying system emphasizes efficiency and adaptability. By leveraging positive pressure or negative pressure conveying methods, we can accommodate various fly ash particle sizes and moisture content, adapting to diverse industrial scenarios. The system’s modular architecture allows for easy integration with existing infrastructure, enabling clients to upgrade or expand their material handling capabilities without significant disruptions. This flexibility is particularly valuable in industries where operational changes or scale-up are common, such as power generation, cement production, and construction material processing.
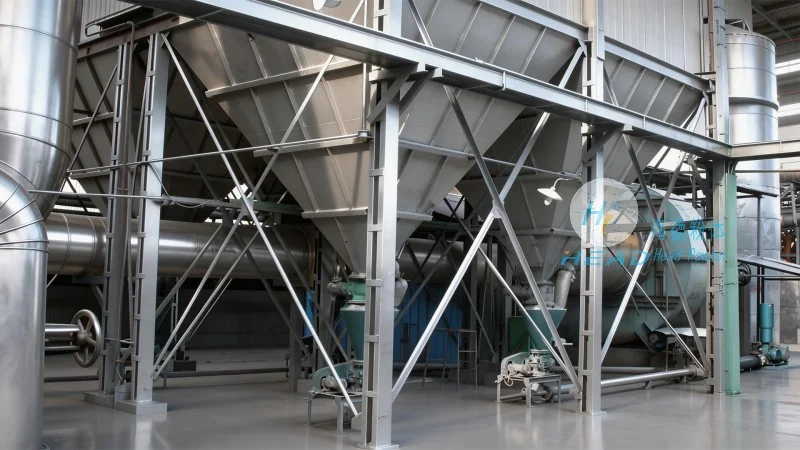
Reliability and Maintenance Considerations
Reliability is a cornerstone of our system design. We prioritize robust construction materials and components that withstand the abrasive nature of fly ash particles, reducing wear and tear over time. The inclusion of regular maintenance protocols and diagnostic tools ensures that the system operates at peak performance, minimizing the risk of breakdowns and extending its service life. Our engineering team provides comprehensive support, including pre-installation assessments, on-site commissioning, and post-implementation maintenance services, to guarantee that clients receive a system that is not only efficient but also long-lasting and cost-effective.
Customization and Client-Specific Solutions
Every fly ash particle pneumatic conveying system is tailored to meet the unique needs of our clients. We work closely with each customer to understand their operational parameters, material characteristics, and budget constraints, then develop a customized solution that maximizes efficiency while staying within financial limits. This client-centric approach ensures that the final system is optimized for their specific workflow, whether it involves short-distance transport within a facility or long-distance transfer between sites. Our commitment to customization extends to system scalability, allowing clients to adjust the system’s capacity as their business grows or operational demands change.
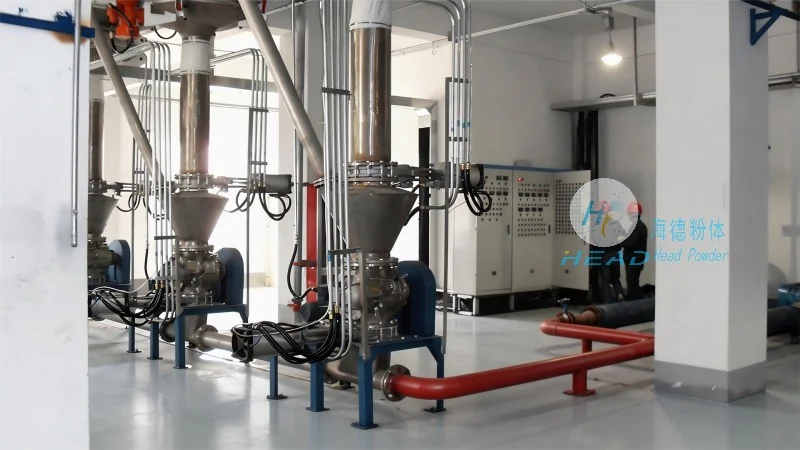
Environmental and Safety Compliance
Our pneumatic conveying systems are designed with environmental and safety considerations at the forefront. The system minimizes dust emissions through sealed conveying lines and efficient filtration, adhering to local environmental regulations. Additionally, safety features such as pressure relief valves, emergency shut-off mechanisms, and regular safety inspections are integrated to protect both personnel and equipment. By prioritizing environmental responsibility and safety, we help our clients operate in compliance with industry standards while reducing their environmental footprint.
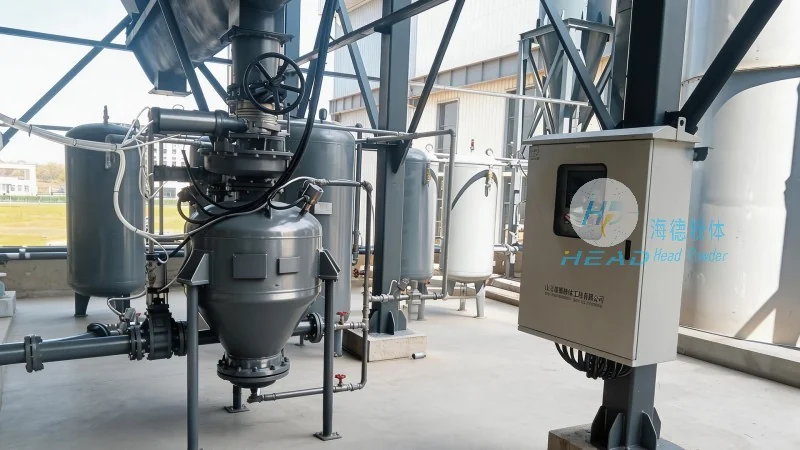
Technical Specifications and Performance Metrics
Our fly ash particle pneumatic conveying system is equipped with technical specifications that reflect industry best practices. Key performance metrics include a maximum conveying distance of up to 500 meters, a flow rate capacity ranging from 5 to 50 tons per hour, and a pressure range of 0.5 to 2.0 bar. The system’s energy efficiency is optimized through variable frequency drives and energy recovery systems, reducing operational costs and environmental impact. These specifications are continuously refined based on real-world performance data and client feedback, ensuring that our systems remain at the forefront of material handling technology.
Conclusion and Service Commitment
Shandong HeadPowder Engineering Co., Ltd. is dedicated to providing innovative and reliable solutions for fly ash particle pneumatic conveying. Our team of experienced engineers and technicians combines technical expertise with a client-focused approach to deliver systems that meet and exceed industry standards. By integrating advanced design principles, robust components, and comprehensive support, we ensure that our clients achieve efficient, cost-effective, and sustainable material handling solutions. Whether you are a new client or an existing partner, we are committed to supporting your operational needs and helping you achieve your business goals through our advanced pneumatic conveying systems.