

[Coke and Carbon Black Powder Pneumatic Conveying: A Material Transport Solution to Overcome Distance Limitations]
HeadPowder, a leading engineering firm based in Shandong, China, specializes in providing advanced pneumatic conveying solutions for handling carbon black and coal powder. The company's expertise lies in developing systems that effectively transport these fine powders over extended distances, overcoming traditional limitations in material handling. This article explores the technology, benefits, and applications of such systems, highlighting how they enhance operational efficiency and reliability in industrial processes.
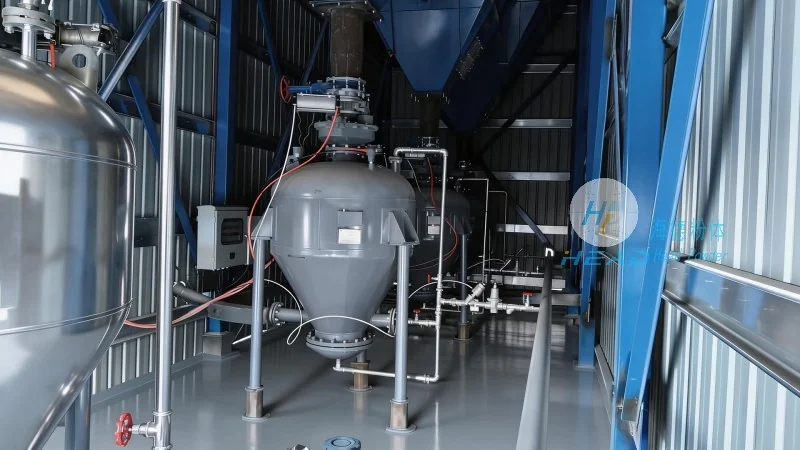
Understanding Pneumatic Conveying for Carbon Black and Coal Powder
Pneumatic conveying is a method of transporting bulk materials, such as carbon black and coal powder, using a gas stream (usually air) to move the material through a pipeline. Unlike traditional mechanical systems like screw conveyors or belt conveyors, pneumatic systems offer flexibility in layout and the ability to handle materials that are difficult to transport with mechanical means. For carbon black and coal powder, which are often fine, abrasive, and prone to dust, pneumatic conveying provides a clean, efficient, and low-maintenance solution. The technology involves creating a pressure differential or using vacuum to draw the material into the pipeline, where it is then transported to the destination point. This method is particularly effective for overcoming distance limitations, as it can transport materials over hundreds or even thousands of meters without significant loss of performance.
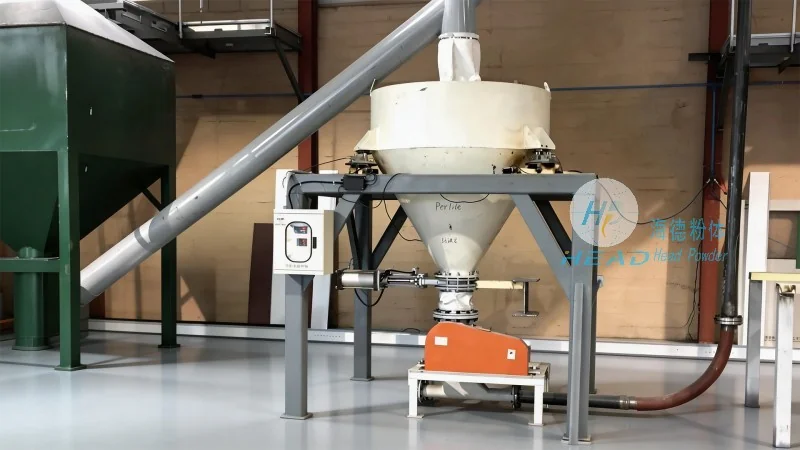
Key Advantages of Pneumatic Conveying Systems
One of the primary advantages of pneumatic conveying for carbon black and coal powder is its ability to handle materials over long distances. Traditional systems may struggle with material degradation or blockages over extended routes, but pneumatic systems maintain consistent flow and particle integrity. The systems also offer improved safety and hygiene, as they operate in enclosed pipelines, reducing dust emissions and minimizing the risk of fire or explosion. Additionally, pneumatic conveying can be integrated with other processing equipment, such as mixers, dryers, or storage silos, creating a seamless material handling workflow. The low maintenance requirements and energy efficiency of these systems further contribute to their cost-effectiveness, making them an attractive option for industrial applications.

HeadPowder's Engineering Expertise and Solutions
Shandong HeadPowder Engineering Co., Ltd. leverages decades of experience in designing and implementing pneumatic conveying systems tailored to the specific needs of carbon black and coal powder industries. The company's engineers work closely with clients to assess material characteristics, process requirements, and site constraints to develop customized solutions. Whether the application involves short-distance transport within a facility or long-distance transfer between plants, HeadPowder provides systems that meet stringent performance standards. The company's solutions include both positive pressure and vacuum conveying technologies, allowing for flexibility in system design and operation. By utilizing high-quality materials and advanced control systems, HeadPowder ensures that its pneumatic conveying equipment operates reliably and efficiently, delivering consistent results for clients. The company's commitment to innovation and customer satisfaction has established it as a trusted partner in the material handling sector.
Applications and Industries Served
The applications of pneumatic conveying for carbon black and coal powder span across various industries, including chemical manufacturing, mining, and energy production. In the chemical industry, these systems are used to transport carbon black for rubber and plastic production, ensuring uniform mixing and quality control. In mining operations, pneumatic conveying facilitates the transport of coal powder from processing plants to storage or power generation facilities, improving logistics and reducing transportation costs. The energy sector also benefits from these systems, as they enable efficient handling of coal for power plants, enhancing operational efficiency and reducing downtime. HeadPowder's solutions are adaptable to these diverse applications, providing tailored systems that meet the unique demands of each industry.
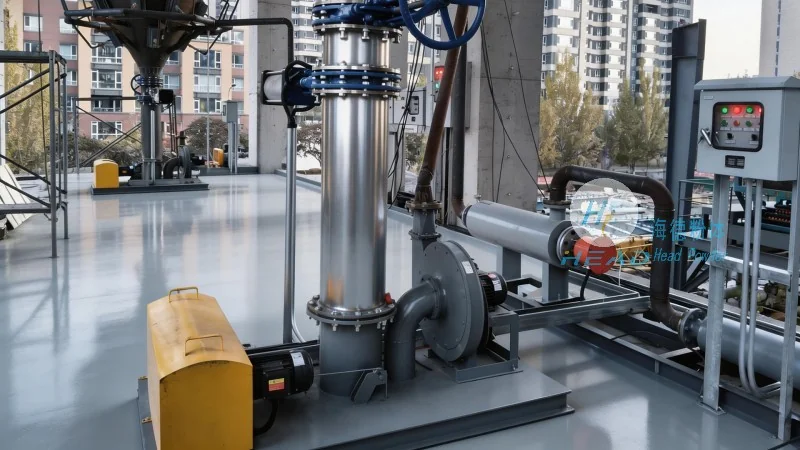
Conclusion and Future Outlook
Pneumatic conveying represents a significant advancement in material handling technology, particularly for carbon black and coal powder, which require specialized solutions to overcome distance limitations. HeadPowder's expertise in designing and implementing these systems ensures that clients can achieve optimal performance, efficiency, and safety in their operations. As industrial processes continue to evolve, the demand for reliable and efficient material transport solutions will remain high. HeadPowder remains at the forefront of this technology, continuously innovating to meet the changing needs of the industry and providing sustainable solutions for the future.